BALL VALVES
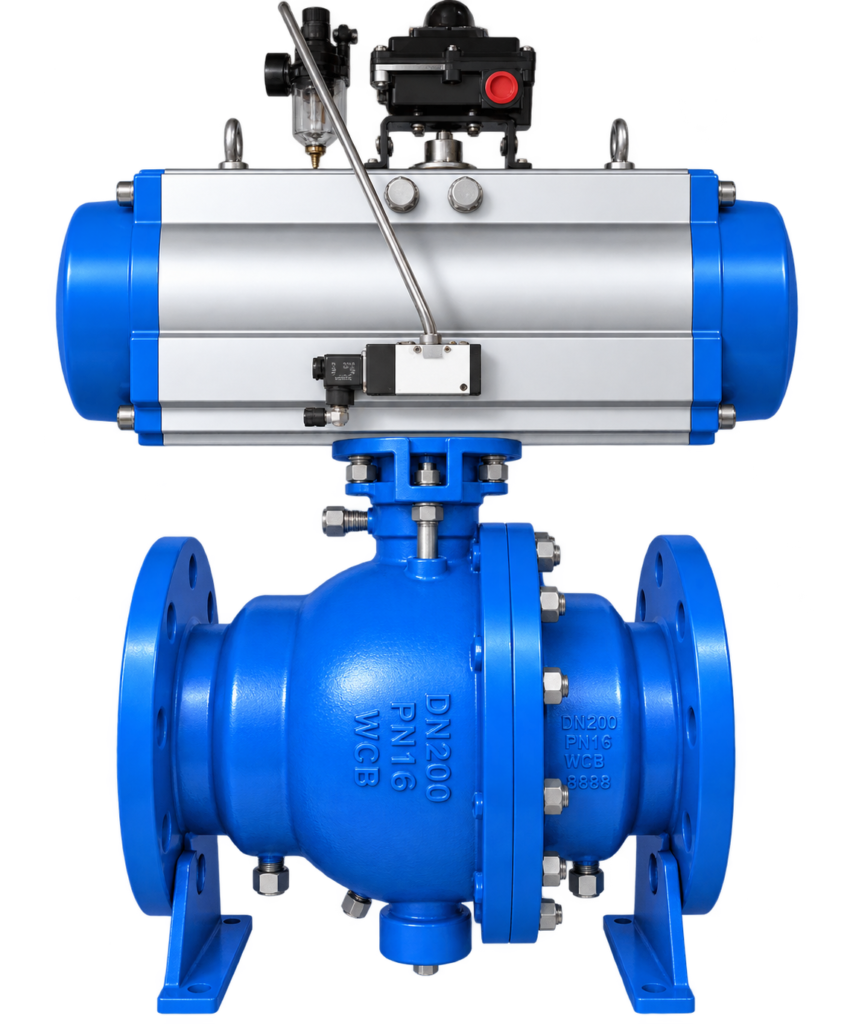
Pneumatic Trunnion Ball Valve
Alis Valves is a trusted Pneumatic Trunnion Ball Valve Manufacturer in India,…
Engineered for Safety, Reliability & Performance in Upstream, Midstream and Downstream Operations
Alis Valves manufactures premium industrial valves for the oil and gas industry, Oil & Gas Valves engineered to perform in high-pressure, high-temperature, and hazardous operating environments. Our comprehensive range of ball valves, butterfly valves, gate valves, globe valves, check valves, control valves, pneumatic actuated valves, and electric actuated valves ensures safe and reliable flow control for drilling, pipeline transportation, refineries, LNG terminals, petrochemical facilities, and offshore platforms. Designed to meet international standards, our valves provide exceptional durability, leak-free performance, and long service life in critical oil and gas applications.
Valve Solutions for Oil & Gas
A wide range of high-performance valves designed to meet the critical demands of Oil & Gas applications.
Alis Valves is a trusted Pneumatic Trunnion Ball Valve Manufacturer in India,…
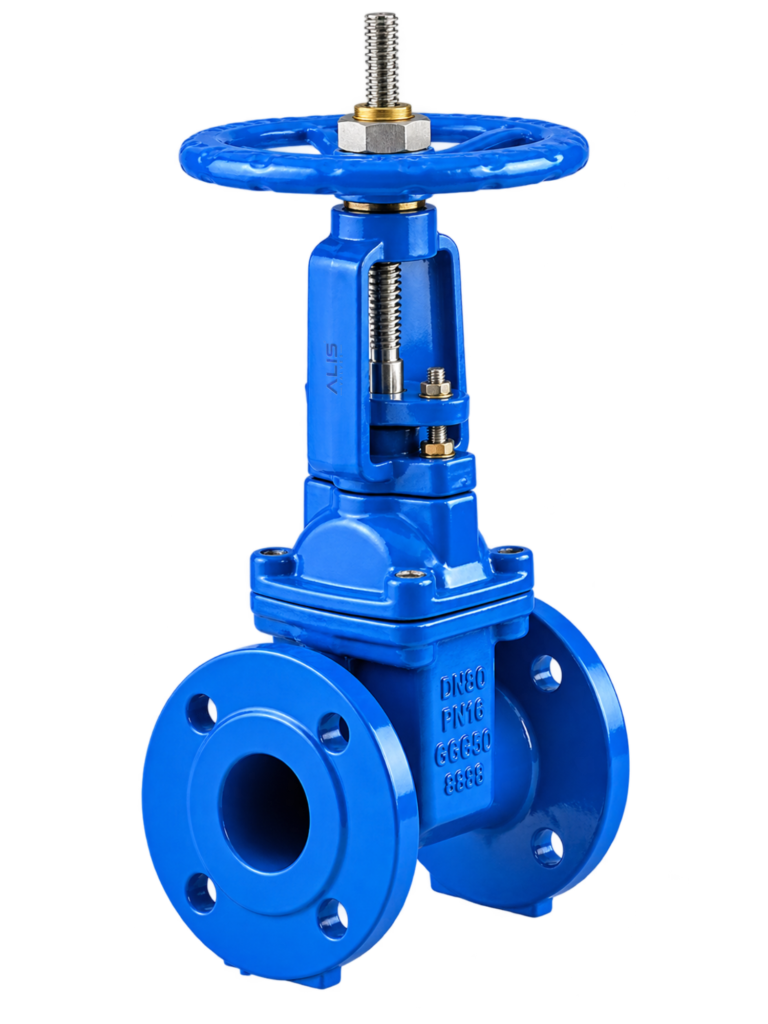
Alis Valves offers high-quality Rising Stem Gate Valves designed for reliable isolation…
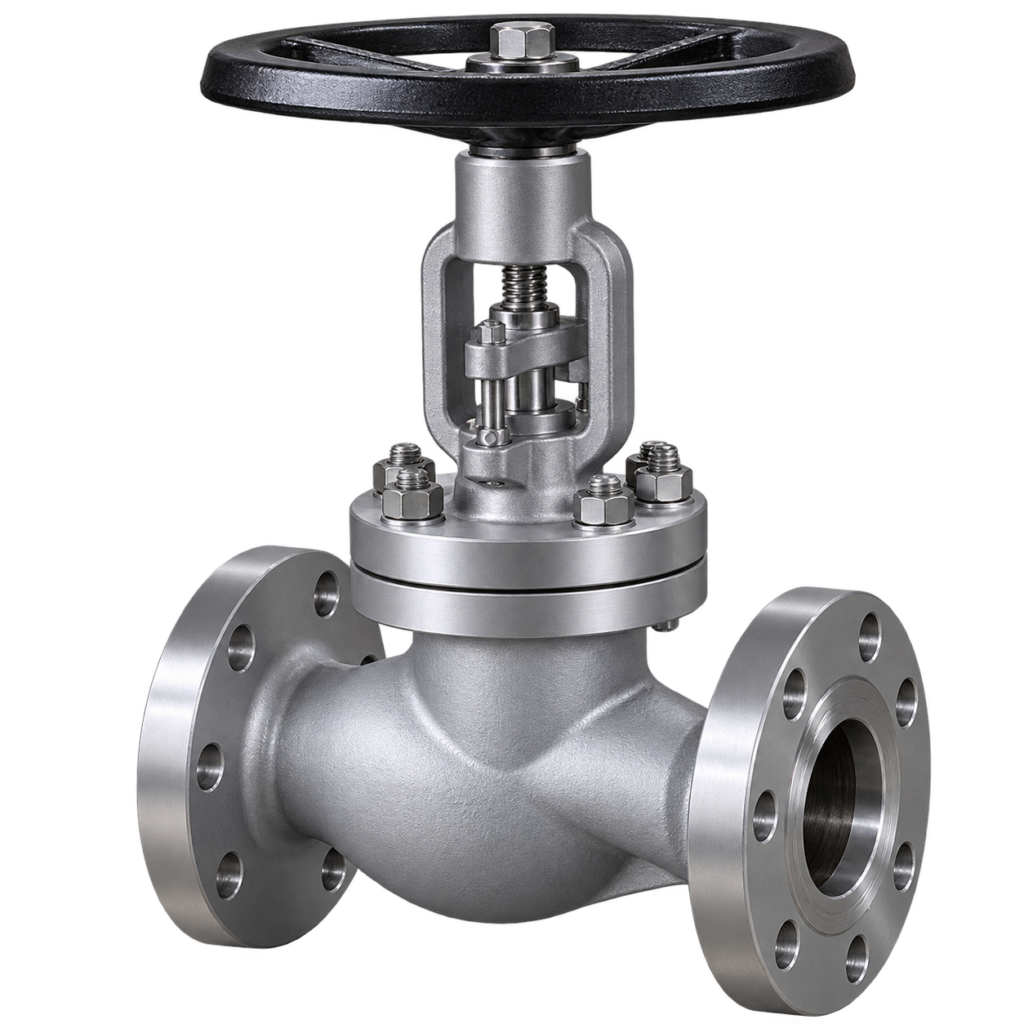
Alis Valves is a trusted High Pressure Globe Control Valve Manufacturer &…
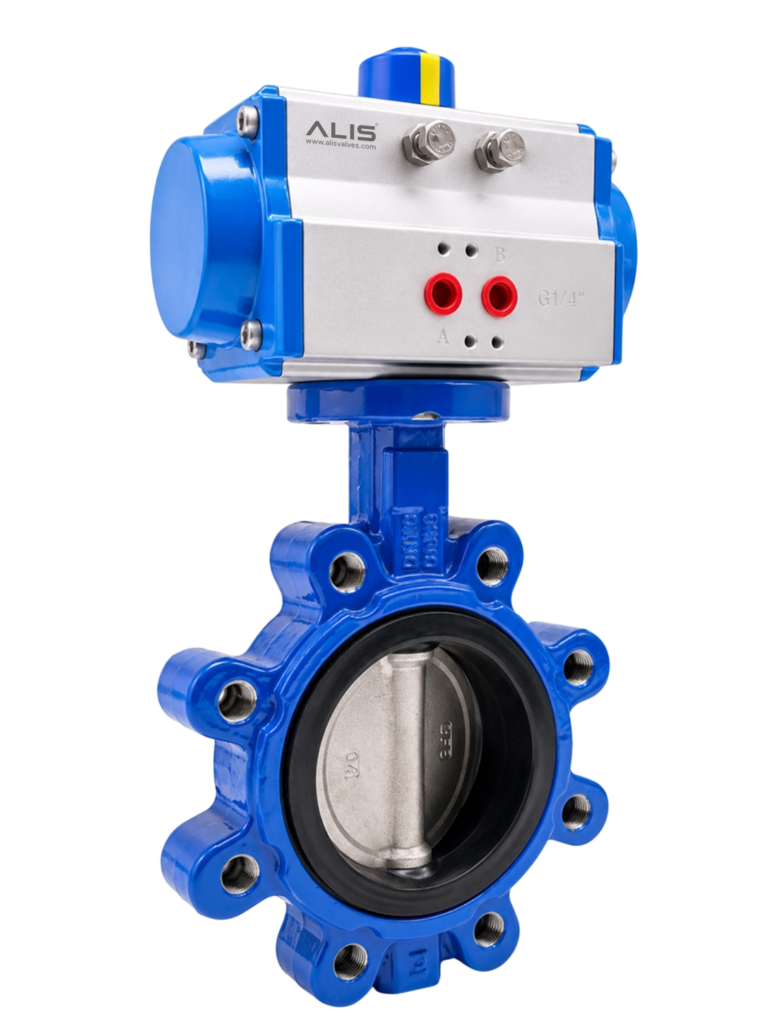
ALIS Valves is a leading Pneumatic Lug Type Butterfly Valve Manufacturer &…
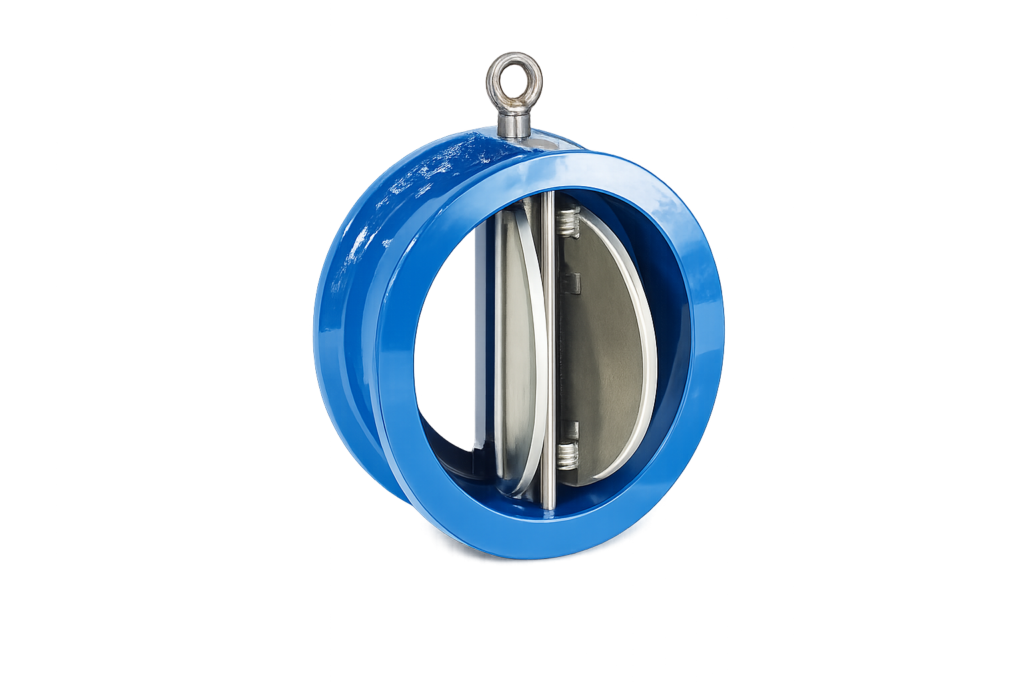
Alis Valves is a leading Dual Plate Check Valve Manufacturer & Supplier…
Product Categories for Oil & Gas
Explore key valve categories and automated packages engineered for Oil & Gas applications.
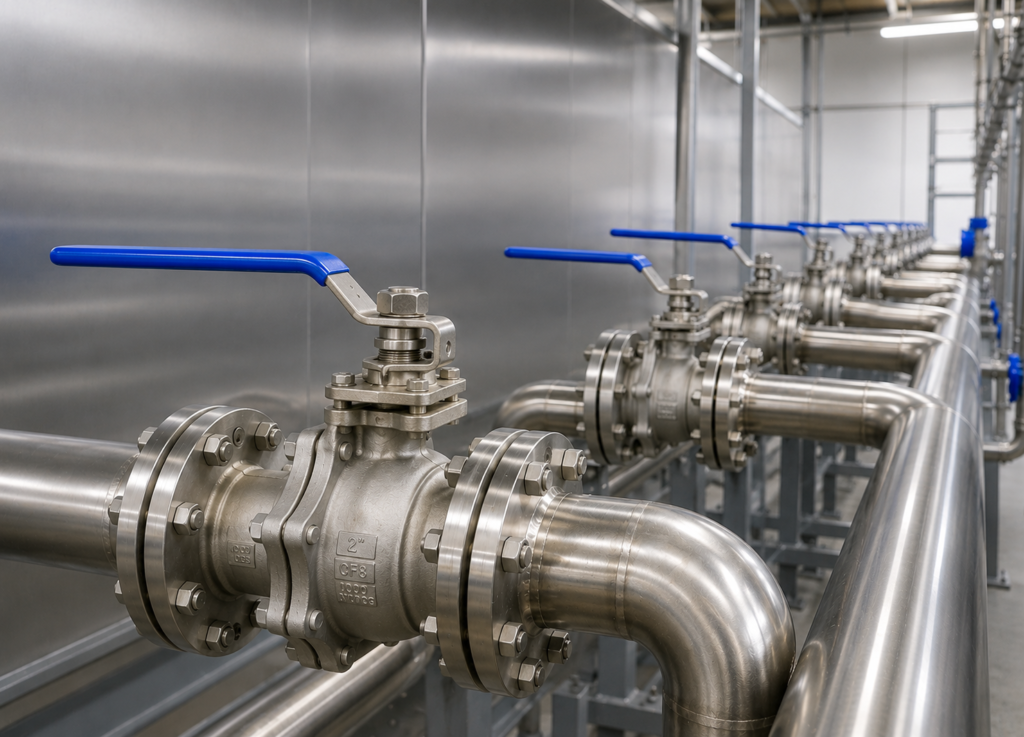
Designed around your needs, our Ball Valves deliver smooth operation, reliable shut-off, and the confidence you need for every flow…
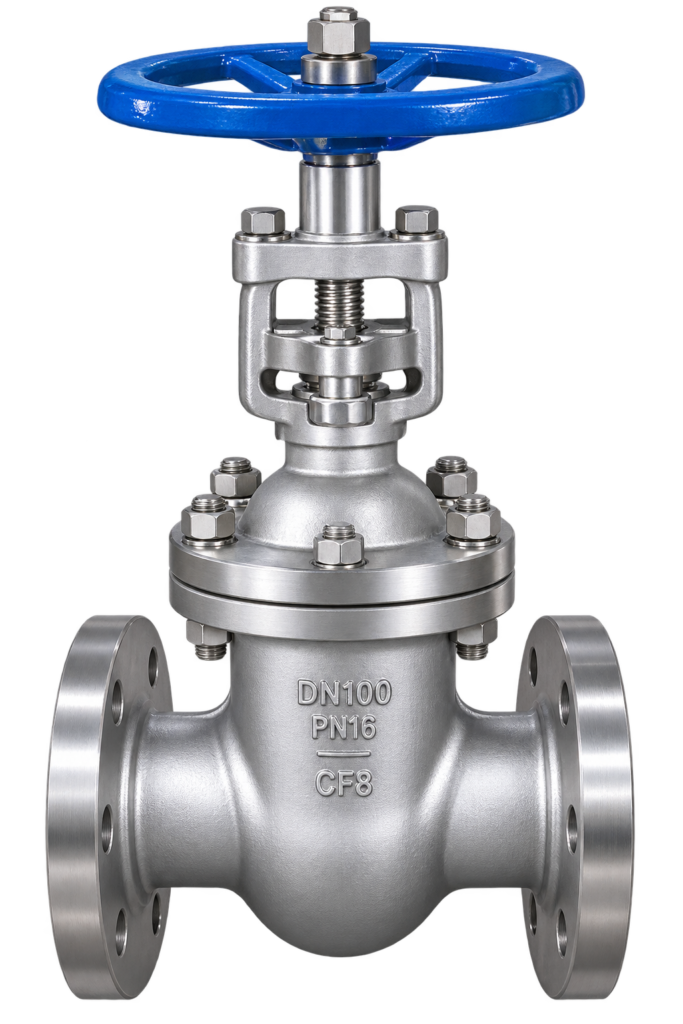
Engineered Gate Valve engineered for superior reliability and severe service performance.
ALIS Valves is a trusted manufacturer and supplier of high-performance control valves designed for accurate flow, pressure, temperature, and level…
Designed for effortless flow control, our Butterfly Valves combine easy operation, dependable shut-off, and durable performance to keep your processes…
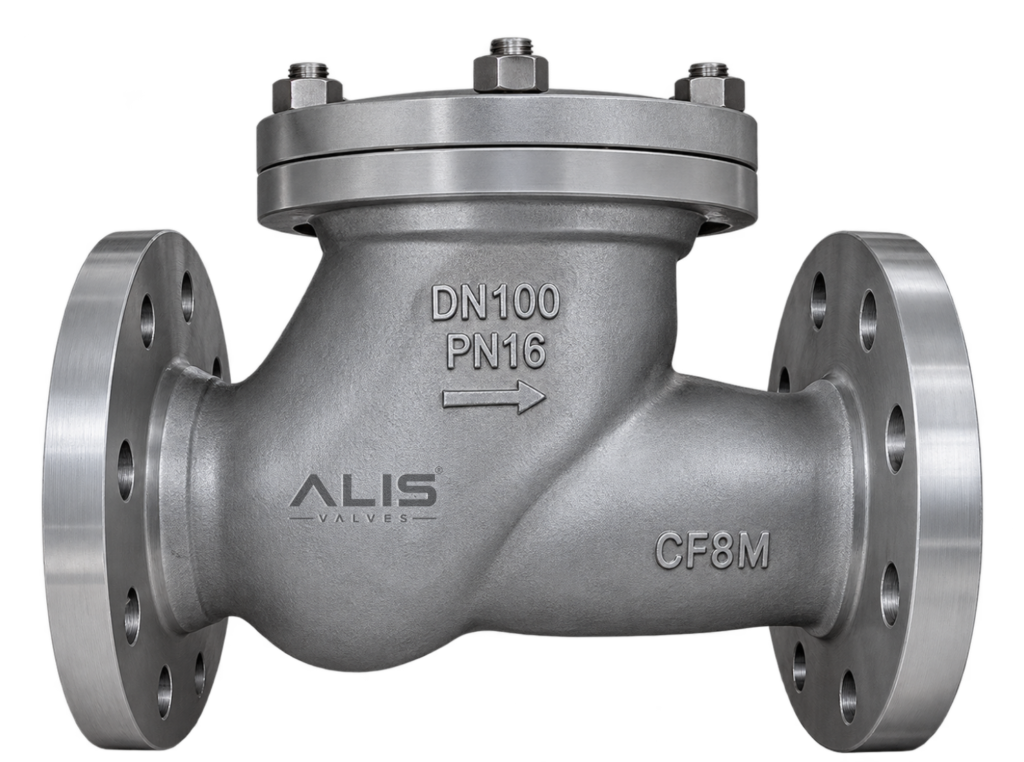
Check Valves designed for automatic backflow prevention in pipelines handling water, steam, oil, gas, and process fluids. Built for dependable…
Process Solutions & Applications
Engineered valve packages, automated assemblies, and specialized flow control systems designed for critical operating units.
Factory-assembled valve packages with pneumatic or electric actuators, accessories, and control components for reliable and efficient process automation.
Built for Demanding Conditions
Up to Class 2500 (ASME B16.34)
-196°C to +650°C
1/2" to 20"
DN 15 to DN 500
Flanged, RTJ, Butt Weld, Socket Weld, Threaded, Wafer & Lug
WCB, WCC, LCB, CF8, CF8M, SS304, SS316, Duplex, Super Duplex, Inconel, Monel, Hastelloy
API 6D, API 608, API 609, API 600, API 598, ASME B16.34, ISO 17292, NACE MR0175, ANSI, BS, DIN
Got Questions?
Common questions about valve selection, specifications, and certifications for this industry.