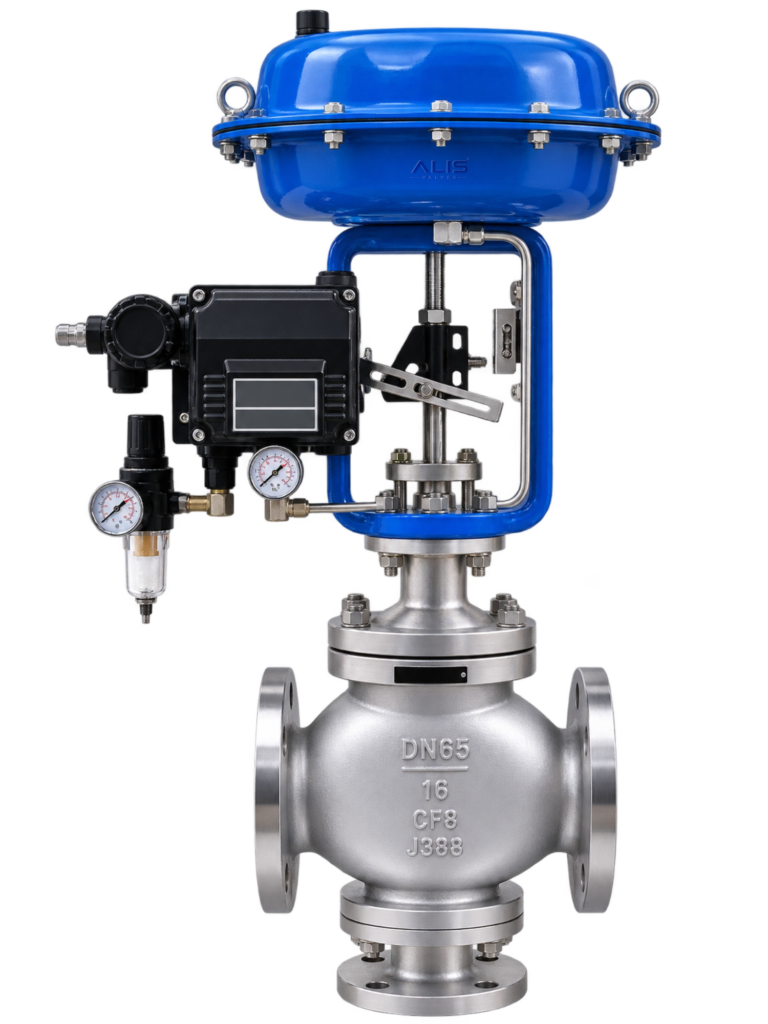
3 WAY CONTROL VALVE
3 Way Diaphragm Type Control Valve
Alis Valves is an 3 Way Diaphragm Type Control Valve Manufacturer in…
Engineered for Safety, Reliability & Performance in Demanding Process Conditions
Alis Valves manufactures high-performance industrial valves for the sugar industry, Sugar Industry Valves Manufacturer in India engineered to deliver safe and efficient flow control across sugar mills, ethanol plants, distilleries, and cogeneration facilities. Our comprehensive range of ball valves, butterfly valves, gate valves, globe valves, check valves, knife gate valves, control valves, pneumatic actuated valves, and electric actuated valves is designed to handle sugar juice, molasses, steam, condensate, hot water, process chemicals, and slurry. Built to international standards, our valves provide exceptional durability, leak-free operation, and reliable performance in demanding sugar processing environments.

Valve Solutions for Sugar
A wide range of high-performance valves designed to meet the critical demands of Sugar applications.
Alis Valves is an 3 Way Diaphragm Type Control Valve Manufacturer in…
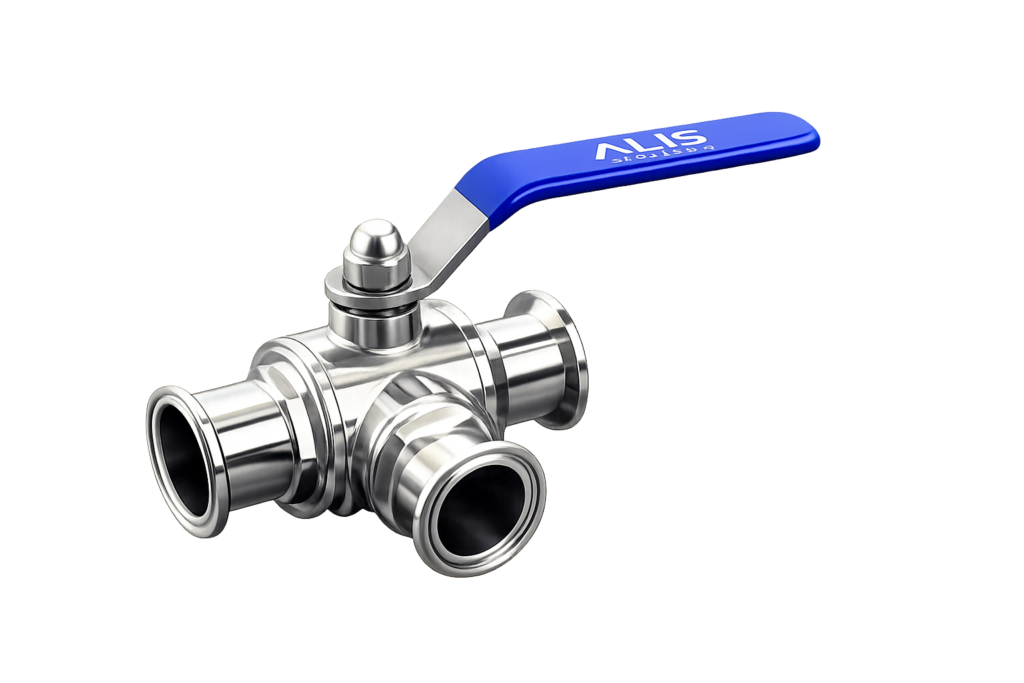
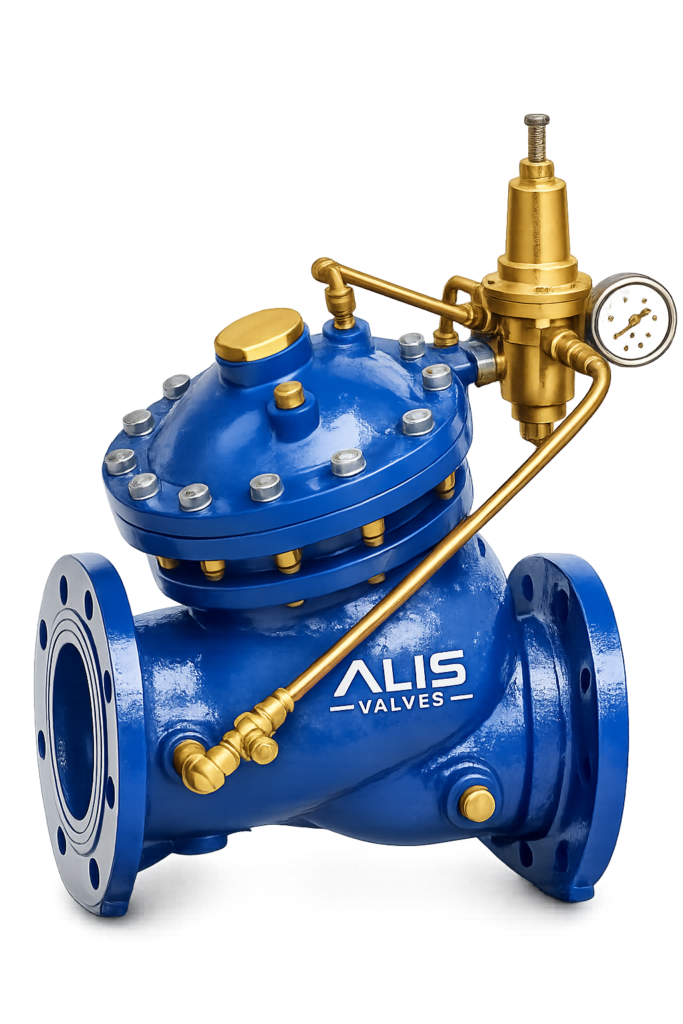
The Adjustable Pressure Reducing Valve (PRV) is a self-operated control valve designed…
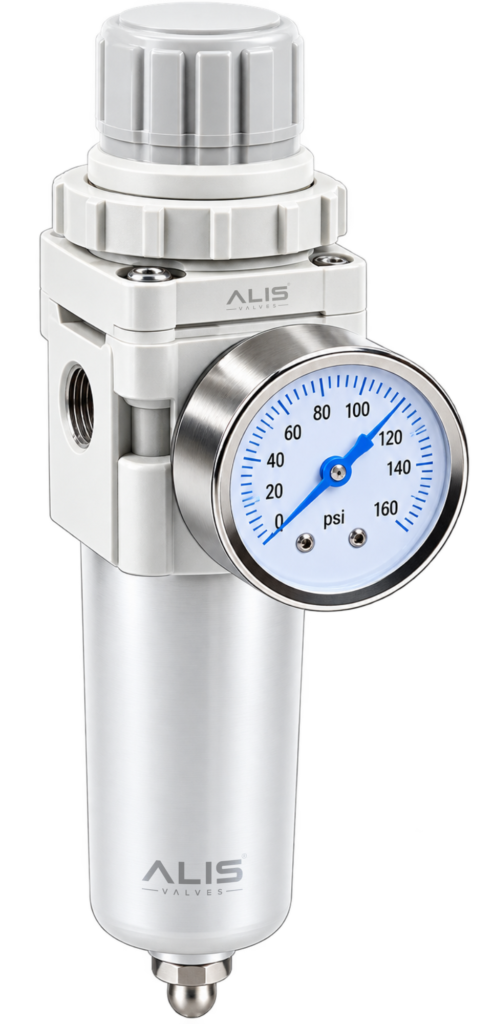
Alis Valves is a trusted Air Filter Regulator (AFR) Manufacturer Supplier in…
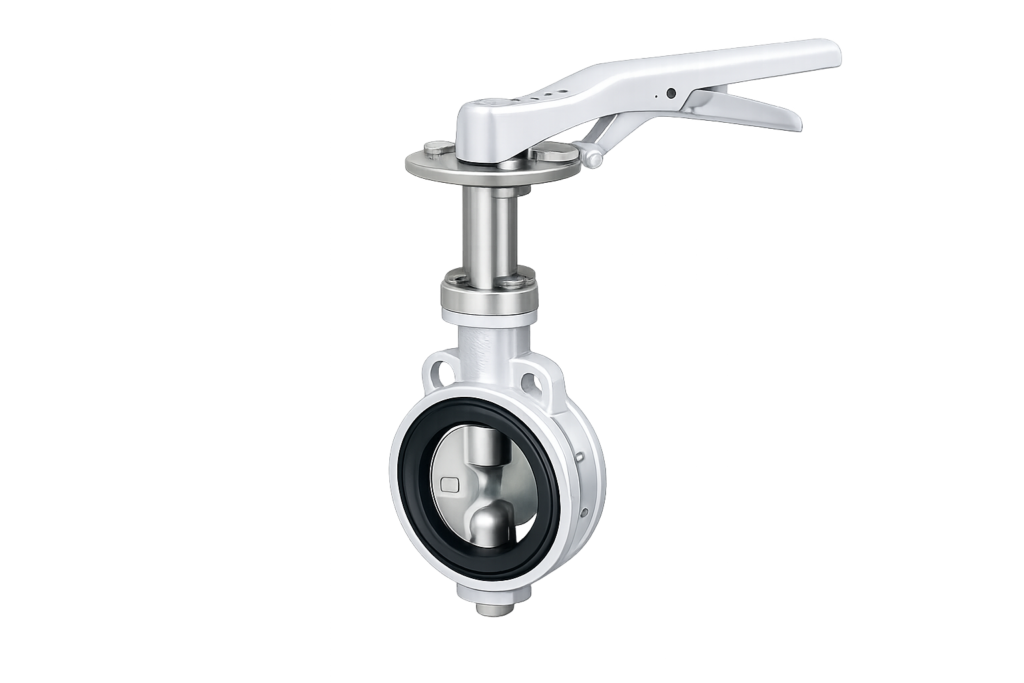
Alis Valves is a trusted Aluminum Butterfly Valve Manufacturer & Supplier in…
Product Categories for Sugar
Explore key valve categories and automated packages engineered for Sugar applications.
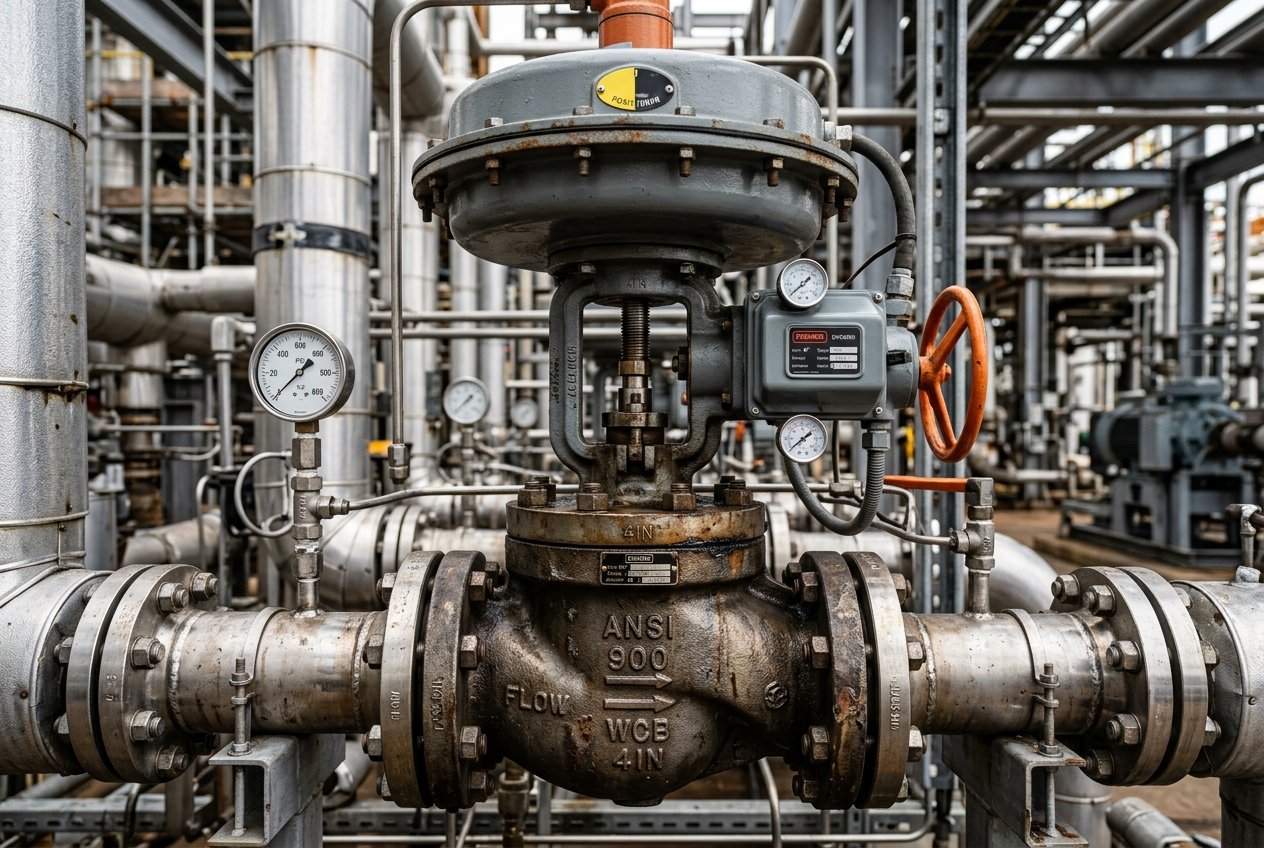
Engineered Control Valves engineered for superior reliability and severe service performance.
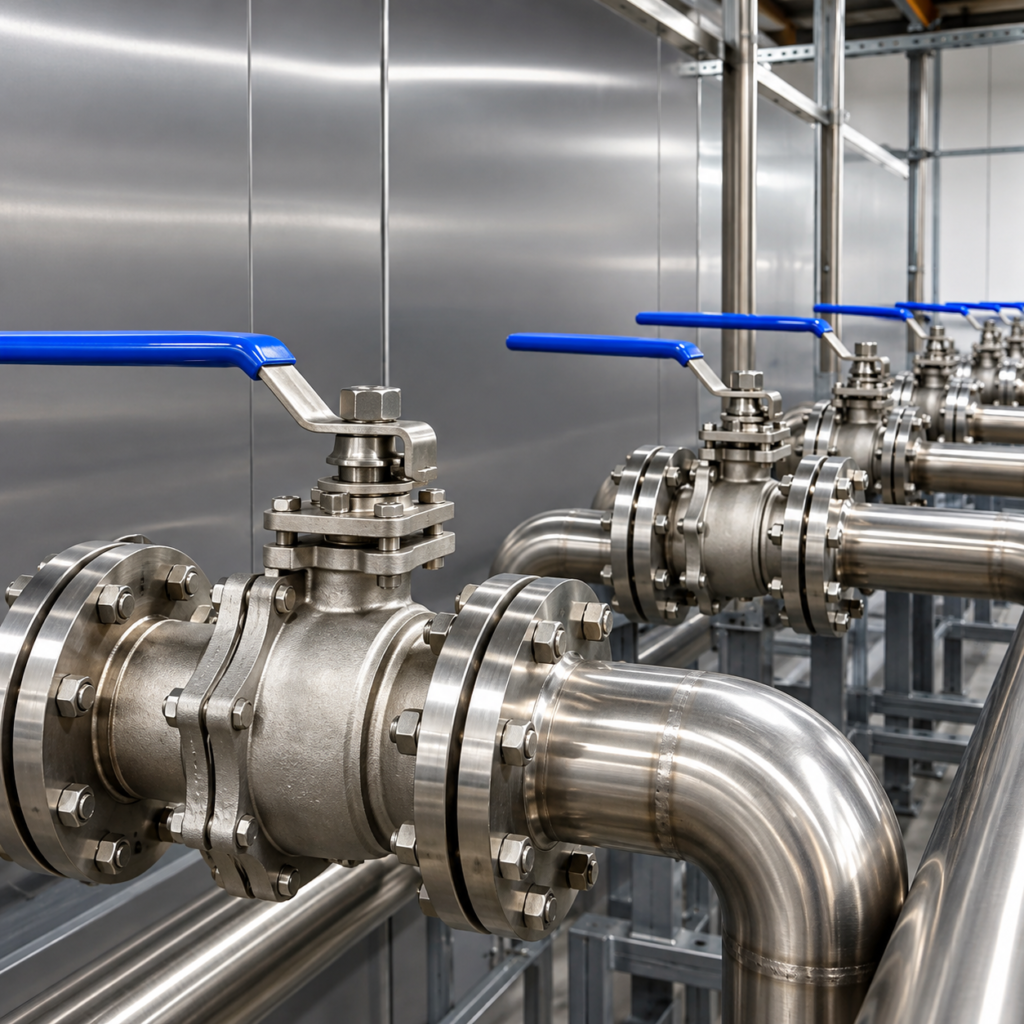
Designed around your needs, our Ball Valves deliver smooth operation, reliable shut-off, and the confidence you need for every flow…
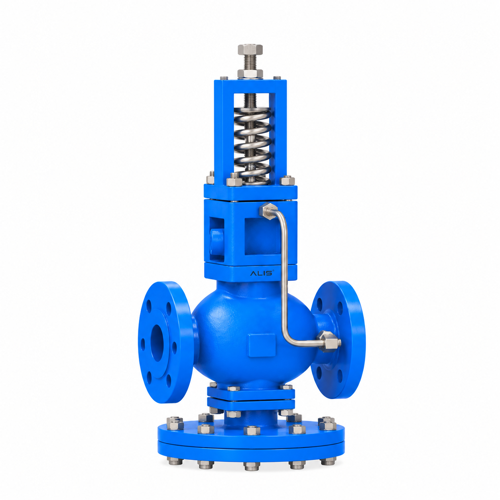
Pressure Reducing Valves engineered to maintain constant outlet pressure while protecting pipelines and equipment from excessive pressure. Ideal for power…
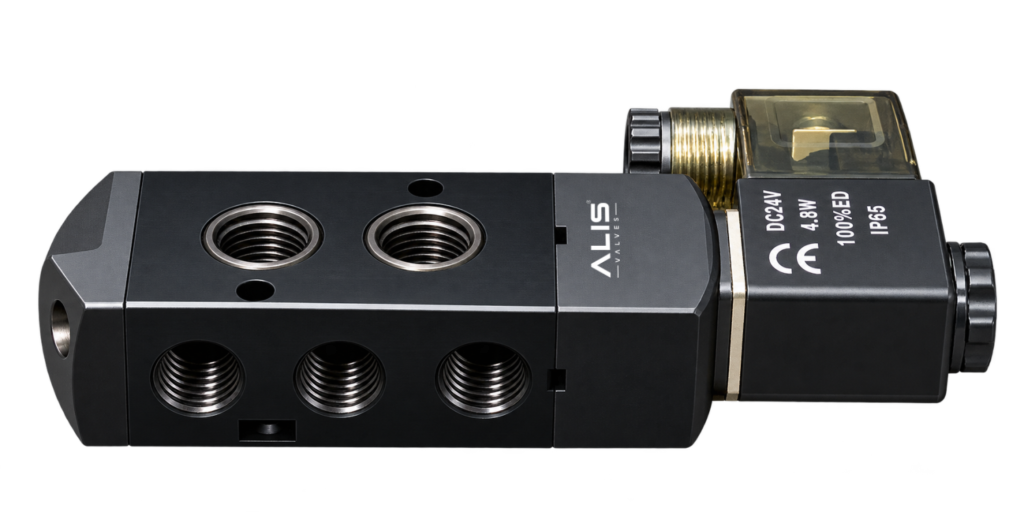
Explore Premium Valve Accessories Including Positioners, Solenoid Valves, Air Filter Regulators (AFR), Limit Switch Boxes, Gear Operators and More.
Designed for effortless flow control, our Butterfly Valves combine easy operation, dependable shut-off, and durable performance to keep your processes…
SUGAR INDUSTRY SOLUTIONS
Industrial valve solutions for sugarcane crushing, juice processing, evaporation, steam distribution, and boiler utility systems. Our valve technologies support reliable flow control and isolation throughout sugar mill operations, with product selection based on process media, temperature, pressure, and operating conditions.
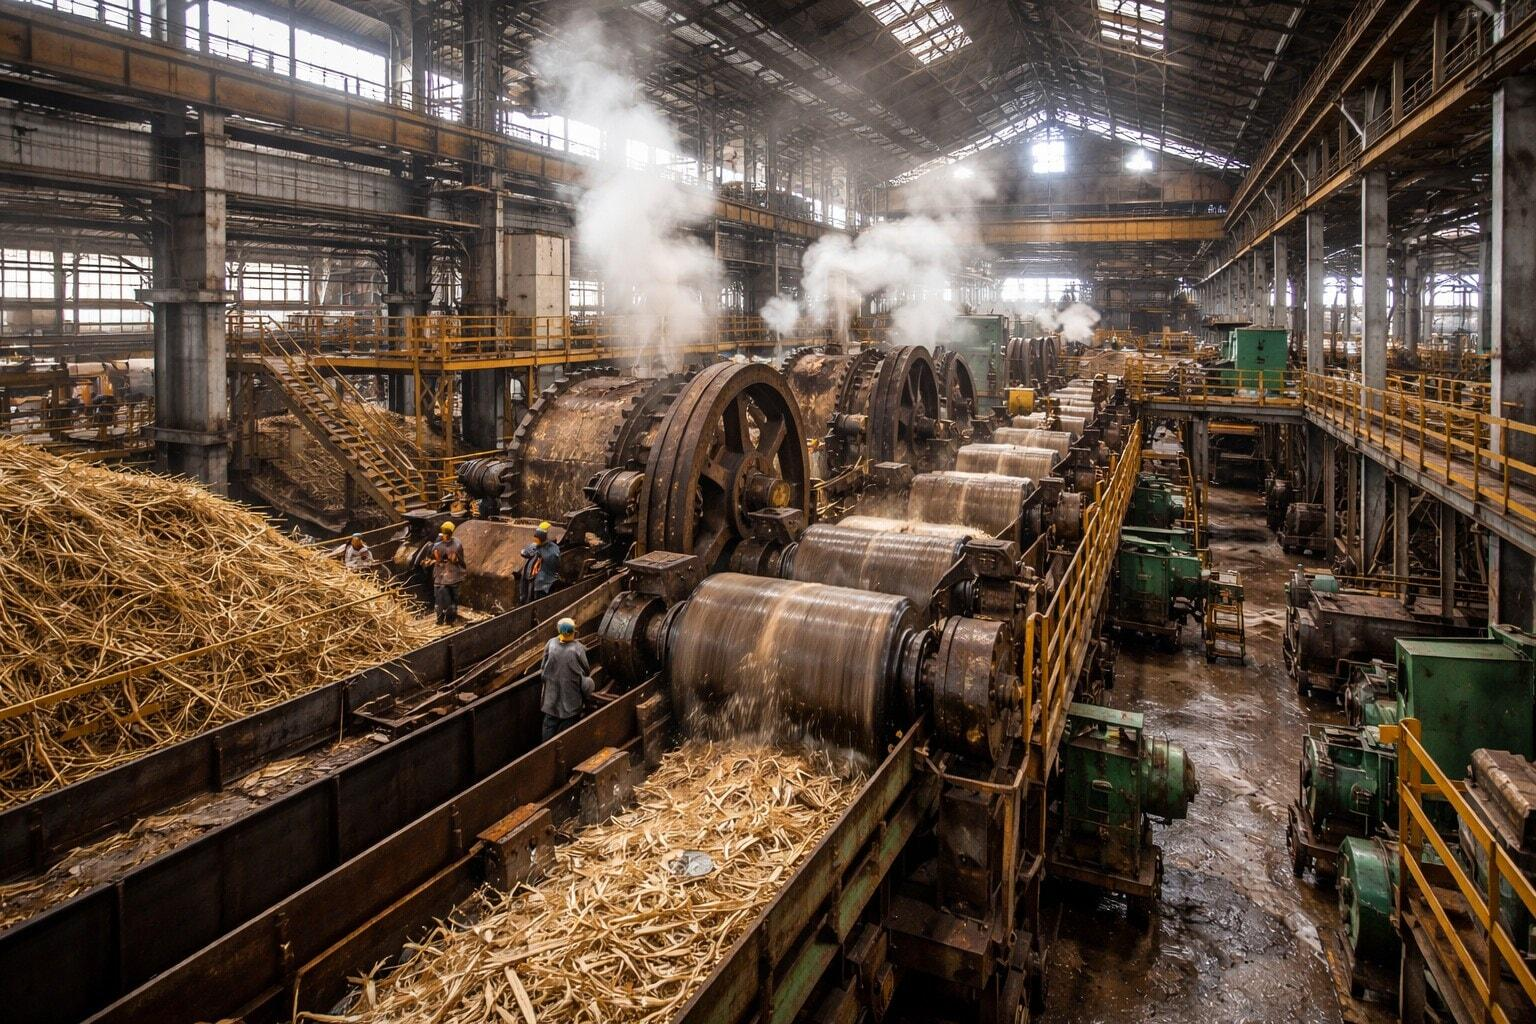
Industrial valve solutions for sugarcane juice transfer, crushing plant utilities, and process flow isolation across sugar manufacturing operations.
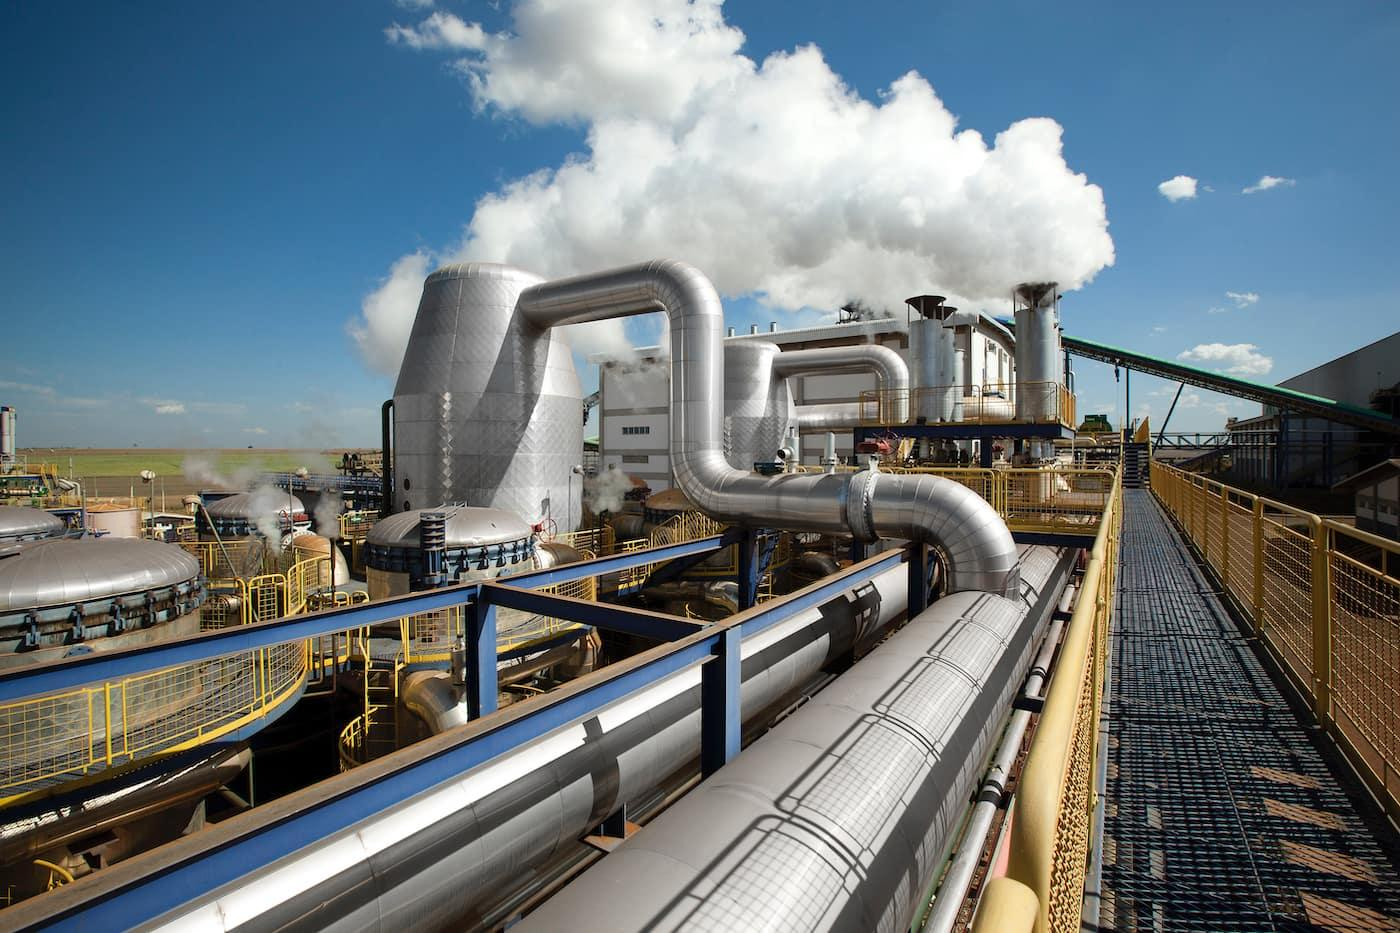
Valve solutions for steam distribution, juice heating, evaporator circuits, and condensate handling, selected for the required pressure and temperature.
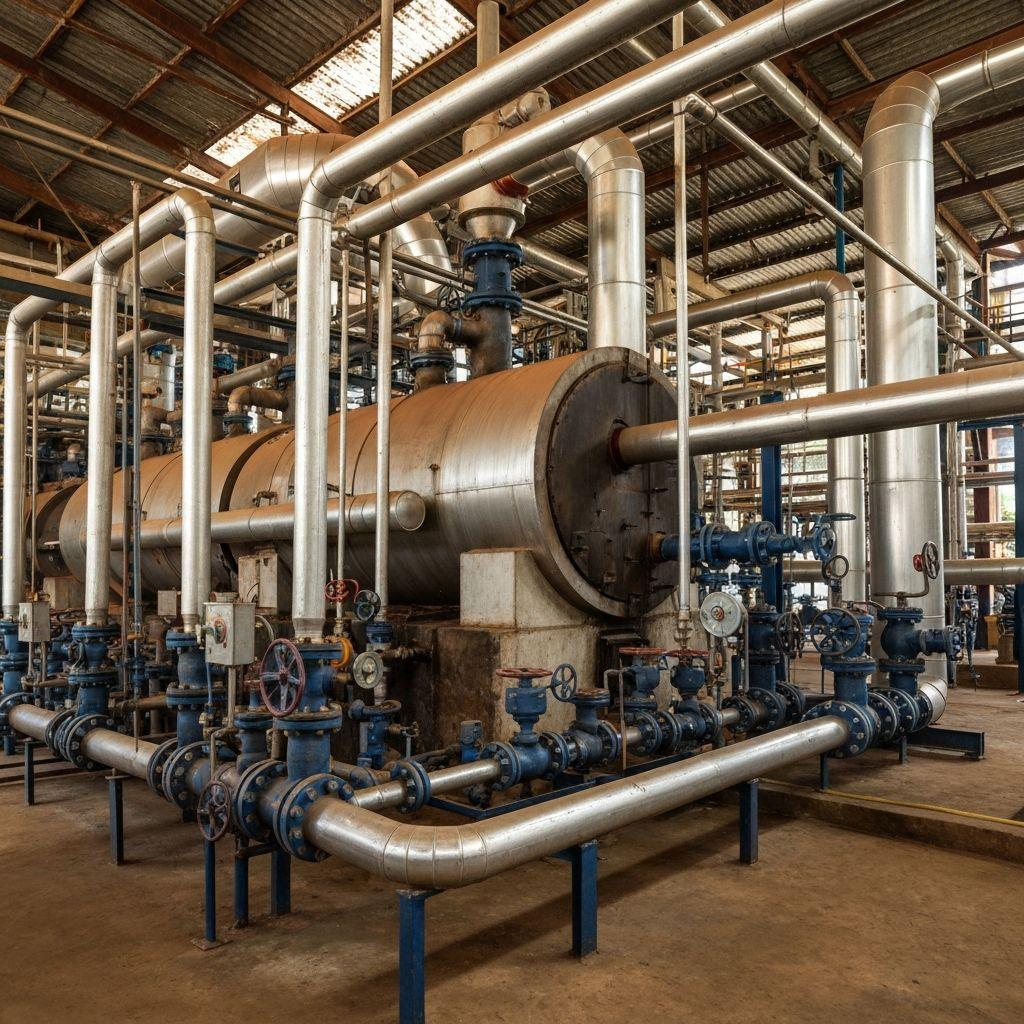
Industrial valve solutions for boiler feedwater, cooling water, and compatible process utility lines supporting bagasse-fired power generation in sugar mills.
Built for Demanding Conditions
Up to Class 2500 (ASME B16.34)
-20°C to +450°C
1/2" to 20"
DN15 to DN 500
Flanged, Wafer, Lug, Threaded, Butt Weld, Socket Weld
Cast Iron, Ductile Iron, WCB, CF8, CF8M, SS304, SS316, Duplex Stainless Steel
API 6D, API 608, API 609, API 598, ASME B16.34, ANSI, DIN, BS, ISO
Got Questions?
Common questions about valve selection, specifications, and certifications for this industry.