Engineered for Safety, Reliability & Performance in Demanding Process Applications
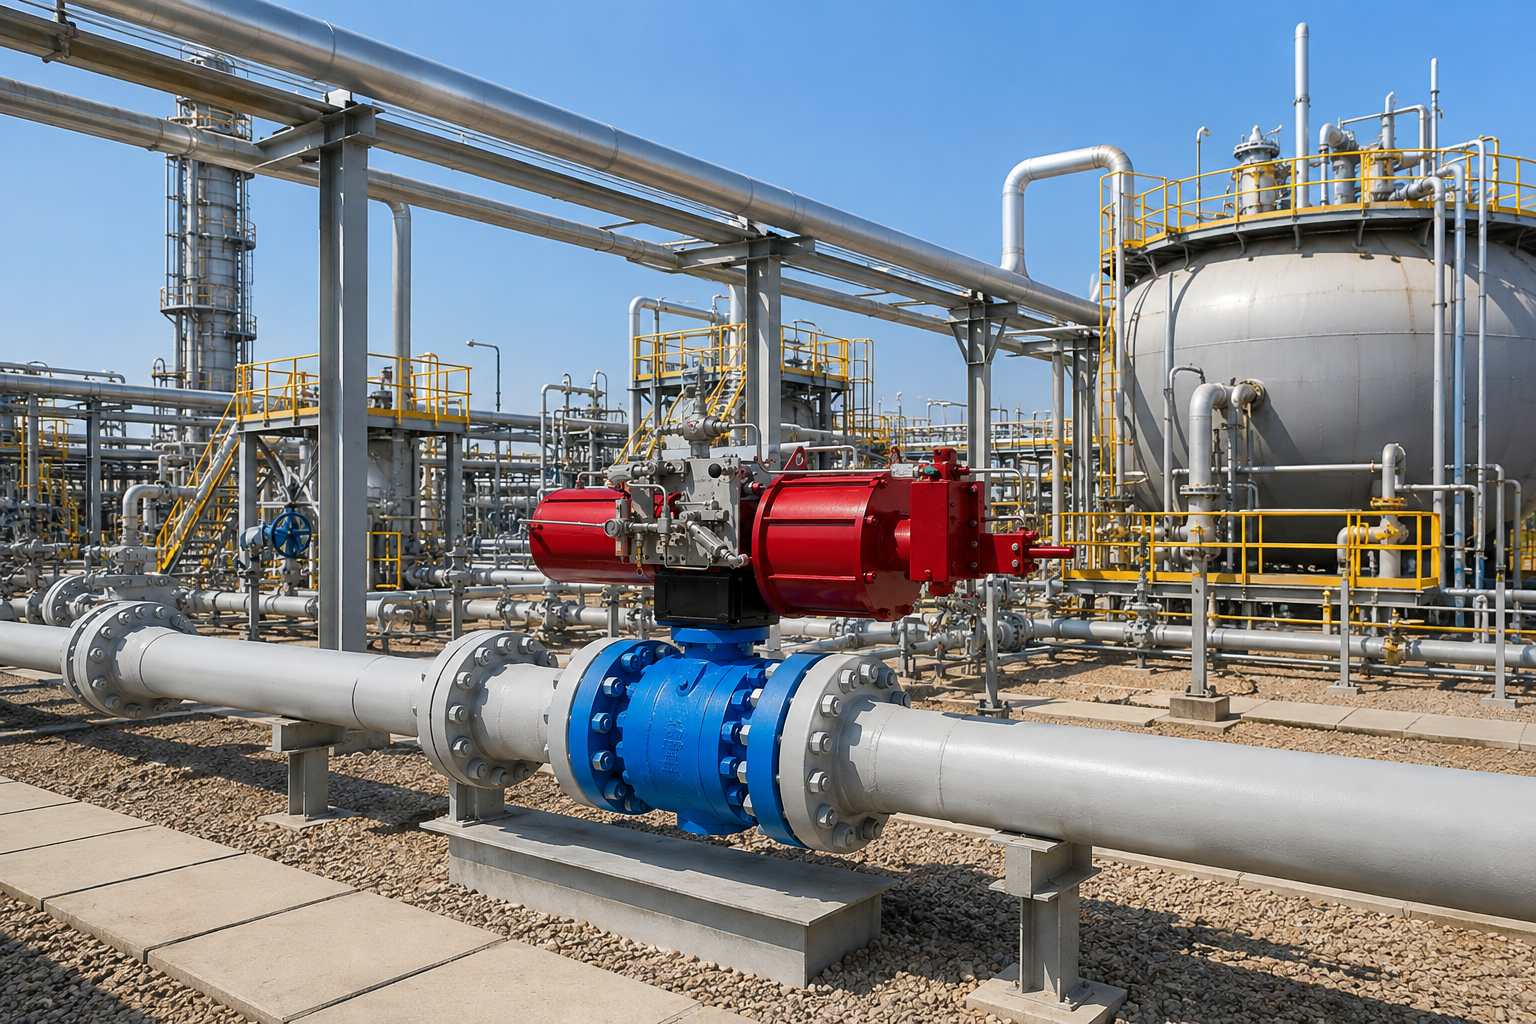
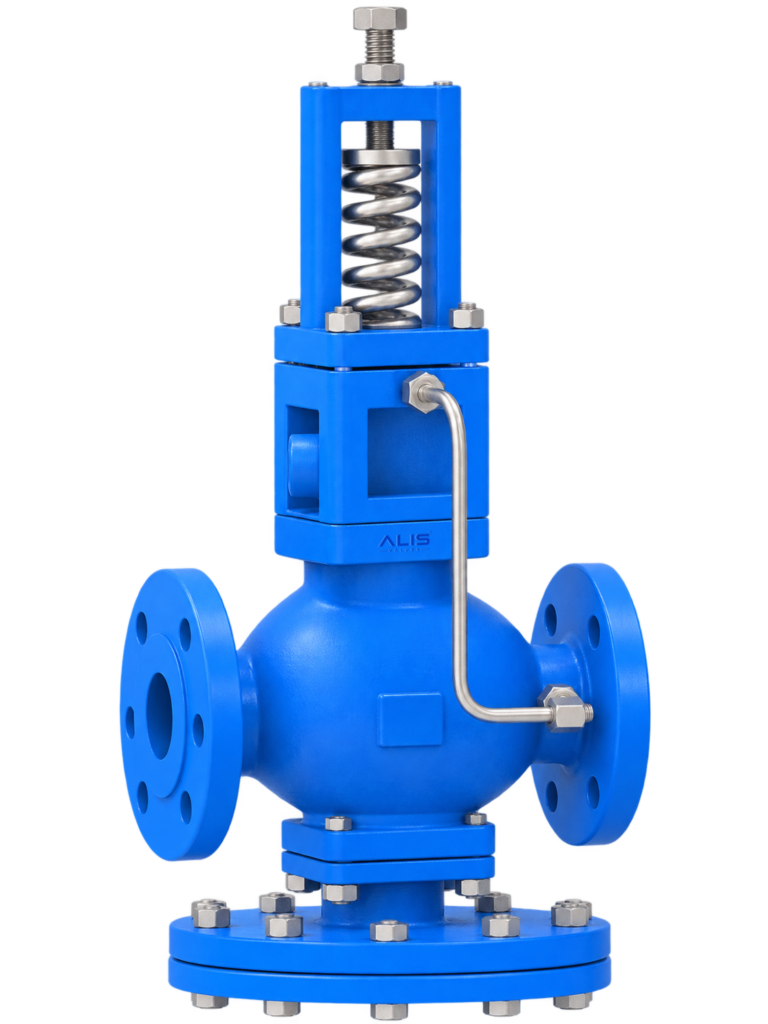
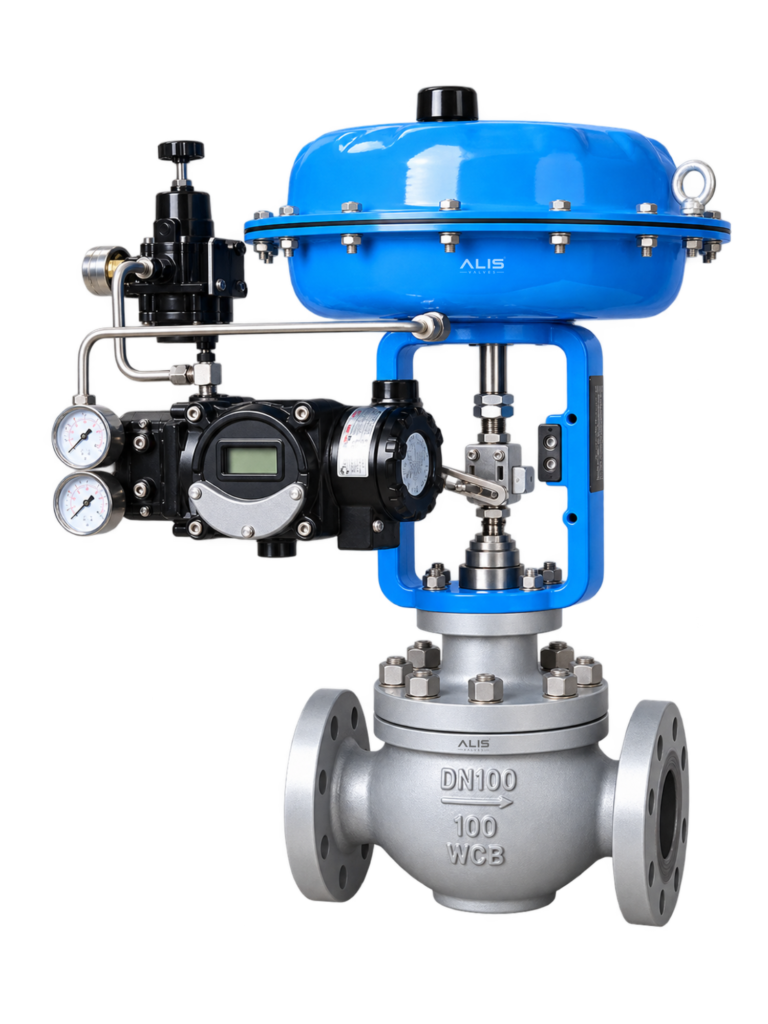
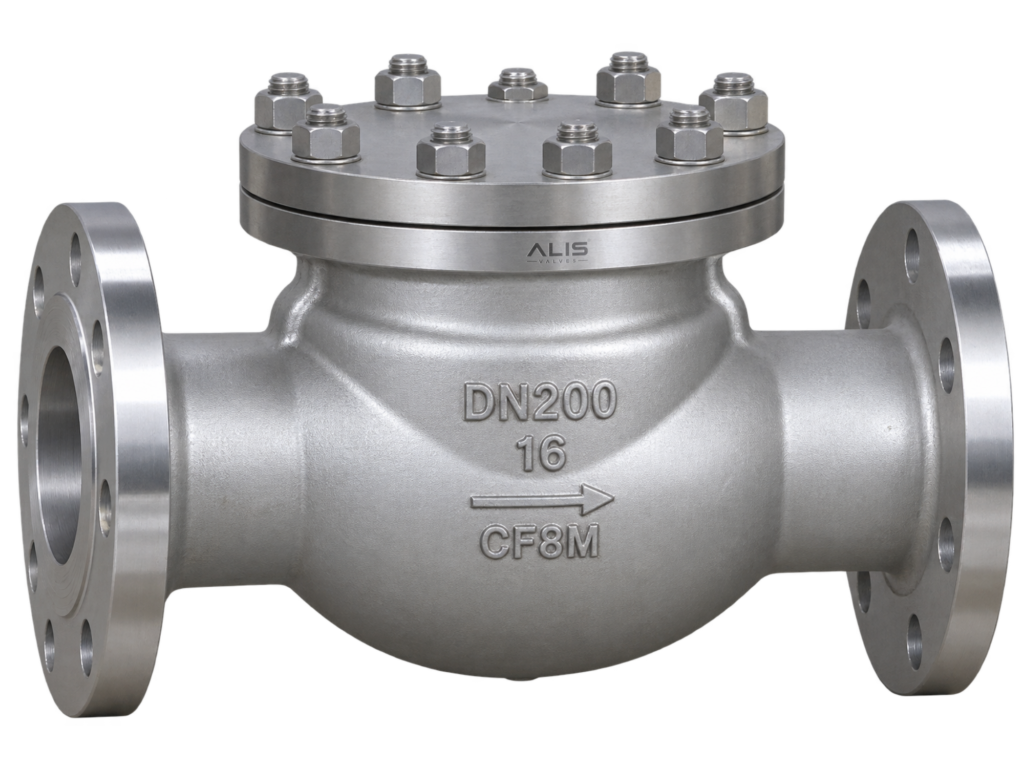
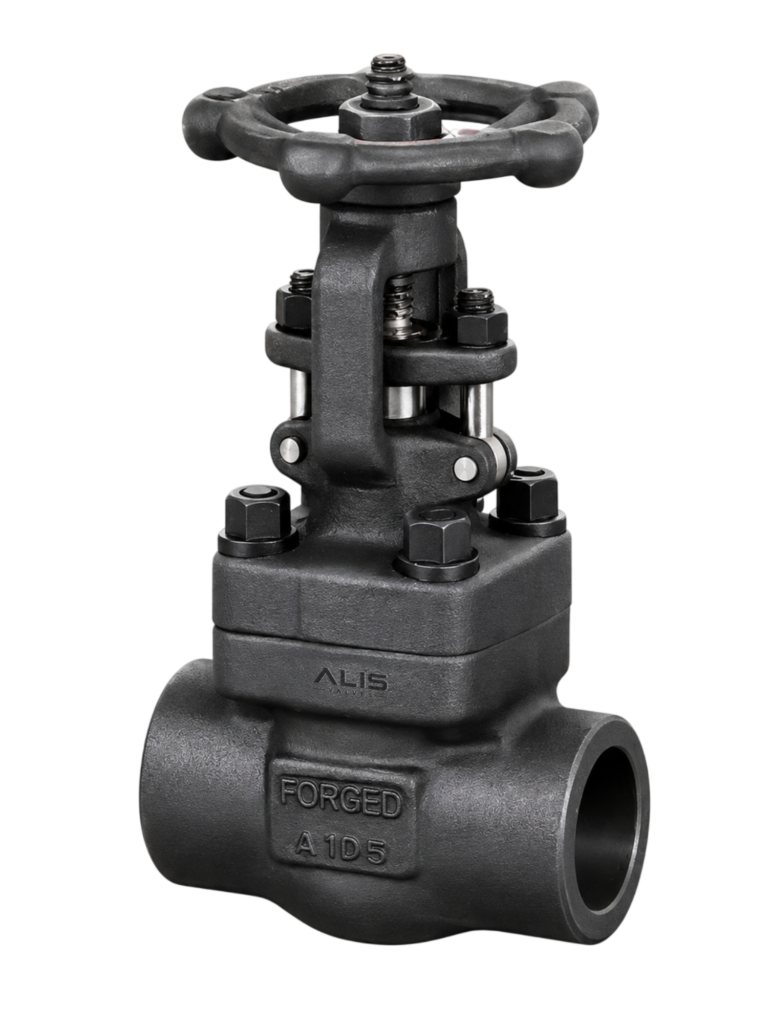
Alis Valves manufactures premium industrial valves for steam applications, Steam Valves Manufacturer in India engineered to deliver reliable flow control in boiler systems, steam distribution networks, condensate recovery systems, heat exchangers, process heating, and industrial utilities. Our comprehensive range of ball valves, butterfly valves, gate valves, globe valves, check valves, control valves, pressure reducing valves, pneumatic actuated valves, and electric actuated valves is designed to handle saturated steam, superheated steam, condensate, and high-temperature process fluids. Built to international standards, our valves ensure leak-free operation, superior durability, and long service life in demanding steam applications.
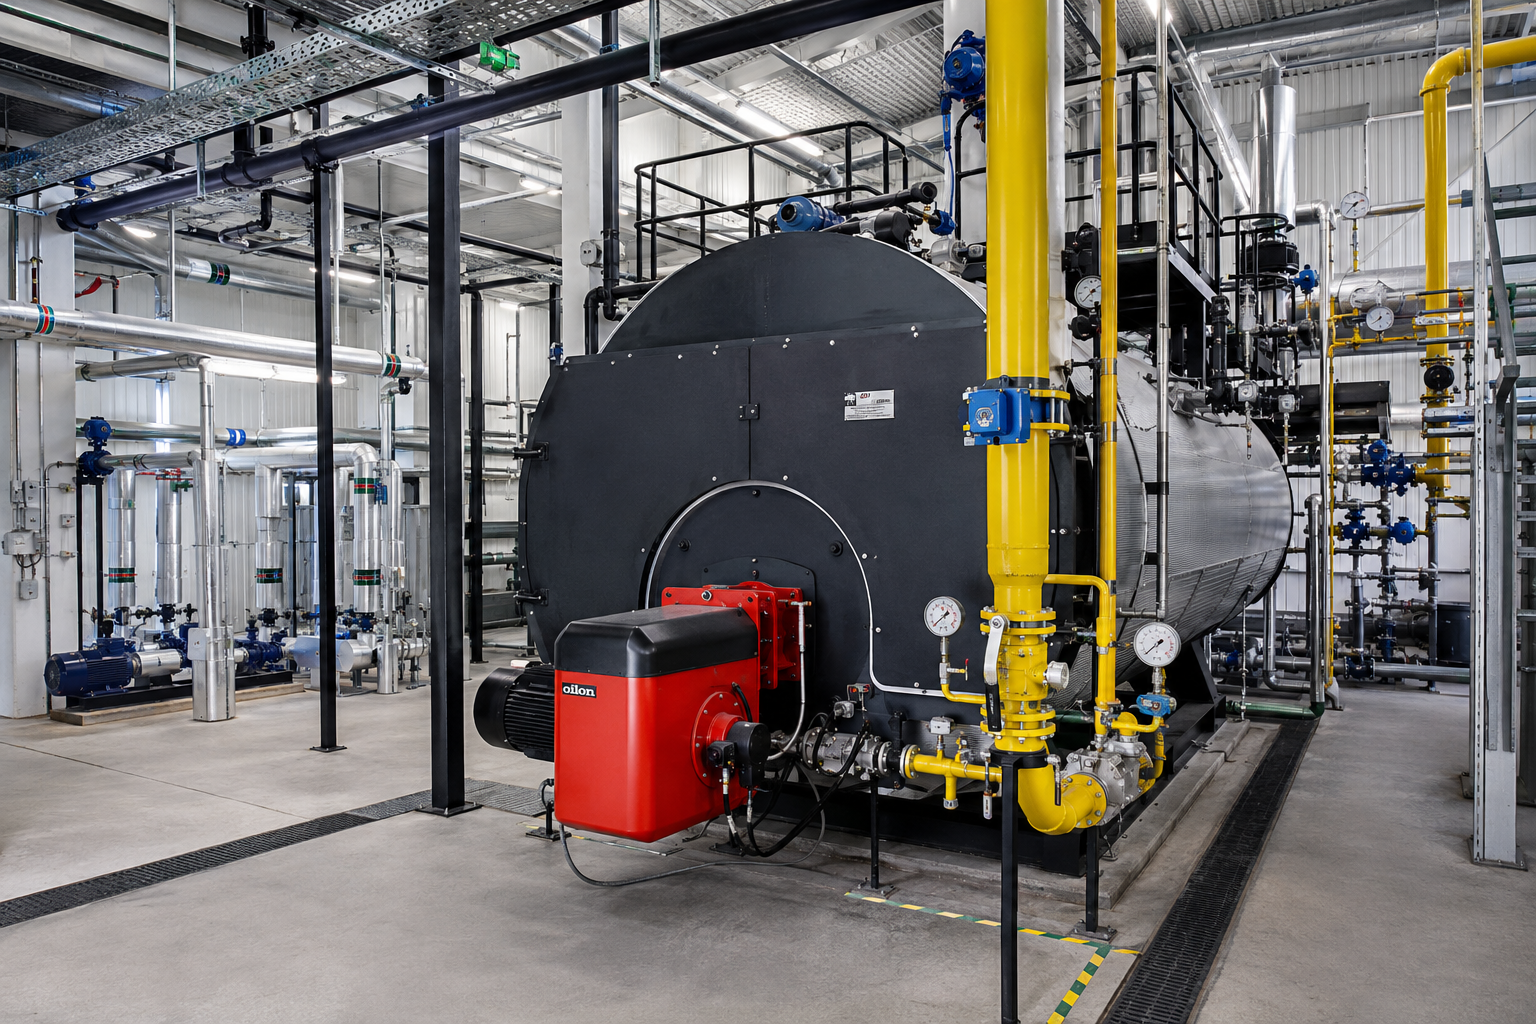
Built for Demanding Conditions
Up to Class 2500 (ASME B16.34)
-20°C to +650°C
1/2" to 20"
DN 15 to DN 500
Flanged, Butt Weld, Socket Weld, Threaded, RTJ
WCB, CF8, CF8M, SS304, SS316, Chrome Moly Alloy Steel
API 600, API 602, API 608, API 598, ASME B16.34, ANSI, DIN, BS, ISO