Chemical
Engineered valve solutions tailored for critical Chemical operating processes.
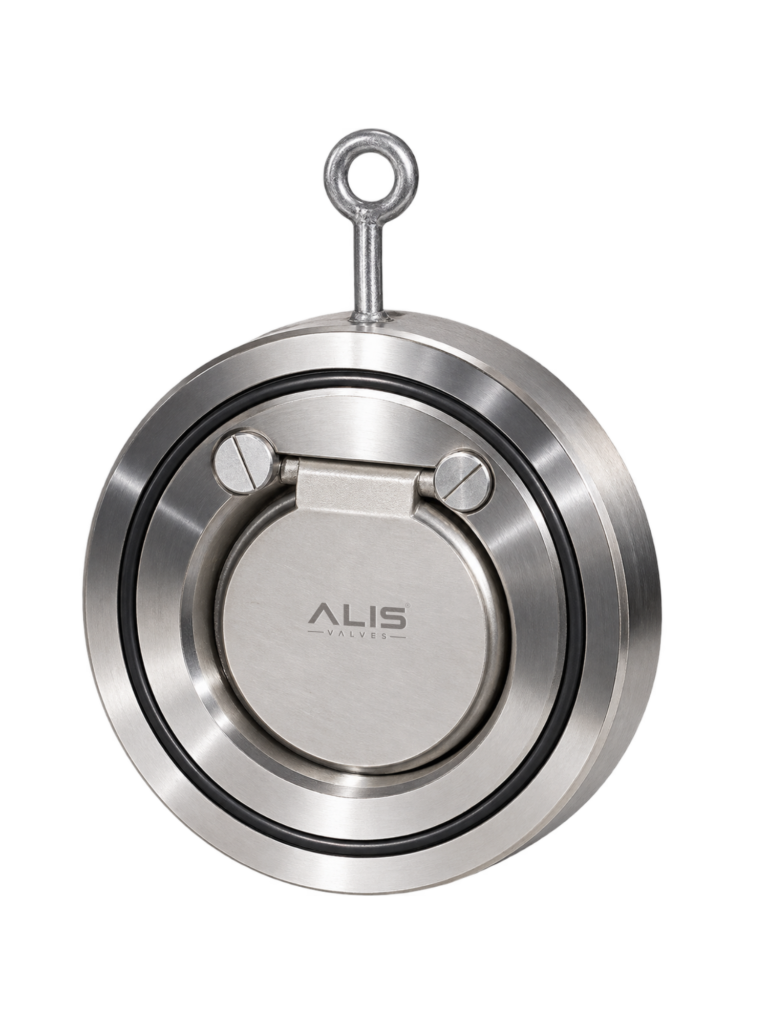
ALIS Valves is a Ball Check Valve Manufacturer and Supplier in India, offering reliable non-return valve solutions for industrial pipeline systems. Ball check valves are designed to prevent reverse flow by using a ball mechanism that moves with the flow and automatically returns to its sealing position when flow stops or reverses. Their simple construction helps support reliable operation and reduces the risk of backflow in pipelines Ball check valves are widely used in water treatment, wastewater management, pumping systems, chemical processing and general industrial piping applications. They are suitable for applications where preventing backflow, protecting pumps and maintaining flow direction are essential for efficient system operation.
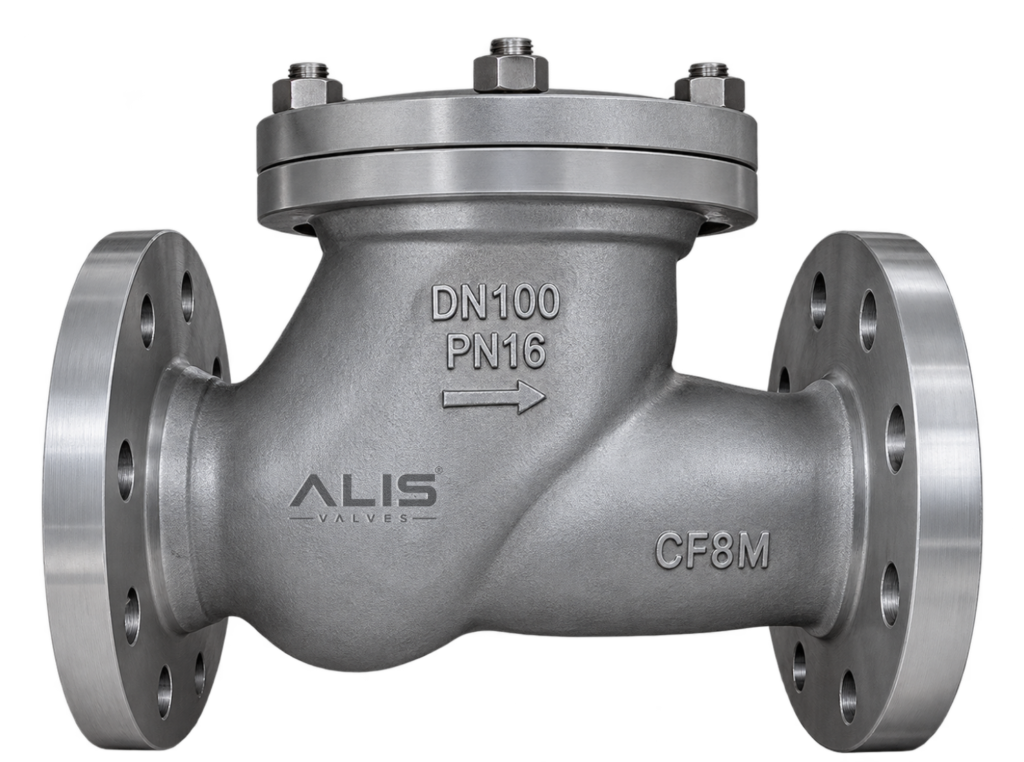
ALIS Valves offers Ball Check Valves for industrial applications requiring reliable one-way flow control. These valves use a ball mechanism to allow fluid to flow in the intended direction and help prevent reverse flow, protecting pipelines and connected equipment.
Ball Check Valves are suitable for compatible applications in water treatment plants, wastewater systems, chemical processing, industrial pipelines and other fluid handling systems. The appropriate valve selection depends on operating pressure, temperature, flow rate, fluid type, valve size and material requirements.
At ALIS Valves, we help you identify a suitable Ball Check Valve based on your application needs and project specifications. Contact us to discuss your requirements and find the right valve solution for your system.
Size Range
DN15 to DN300 (½" to 12")
Pressure Rating
PN10, PN16, PN25 / Class 150
Operating Temperature
Up to 80°C*
Closing Element
Ball
Seat Material
EPDM / NBR / PTFE
Ball Material
Stainless Steel / Ductile Iron / Rubber-Coated
Body Material
Cast Iron / Ductile Iron / Carbon Steel / Stainless Steel
Flow Direction
Unidirectional
Installation
Horizontal / Vertical
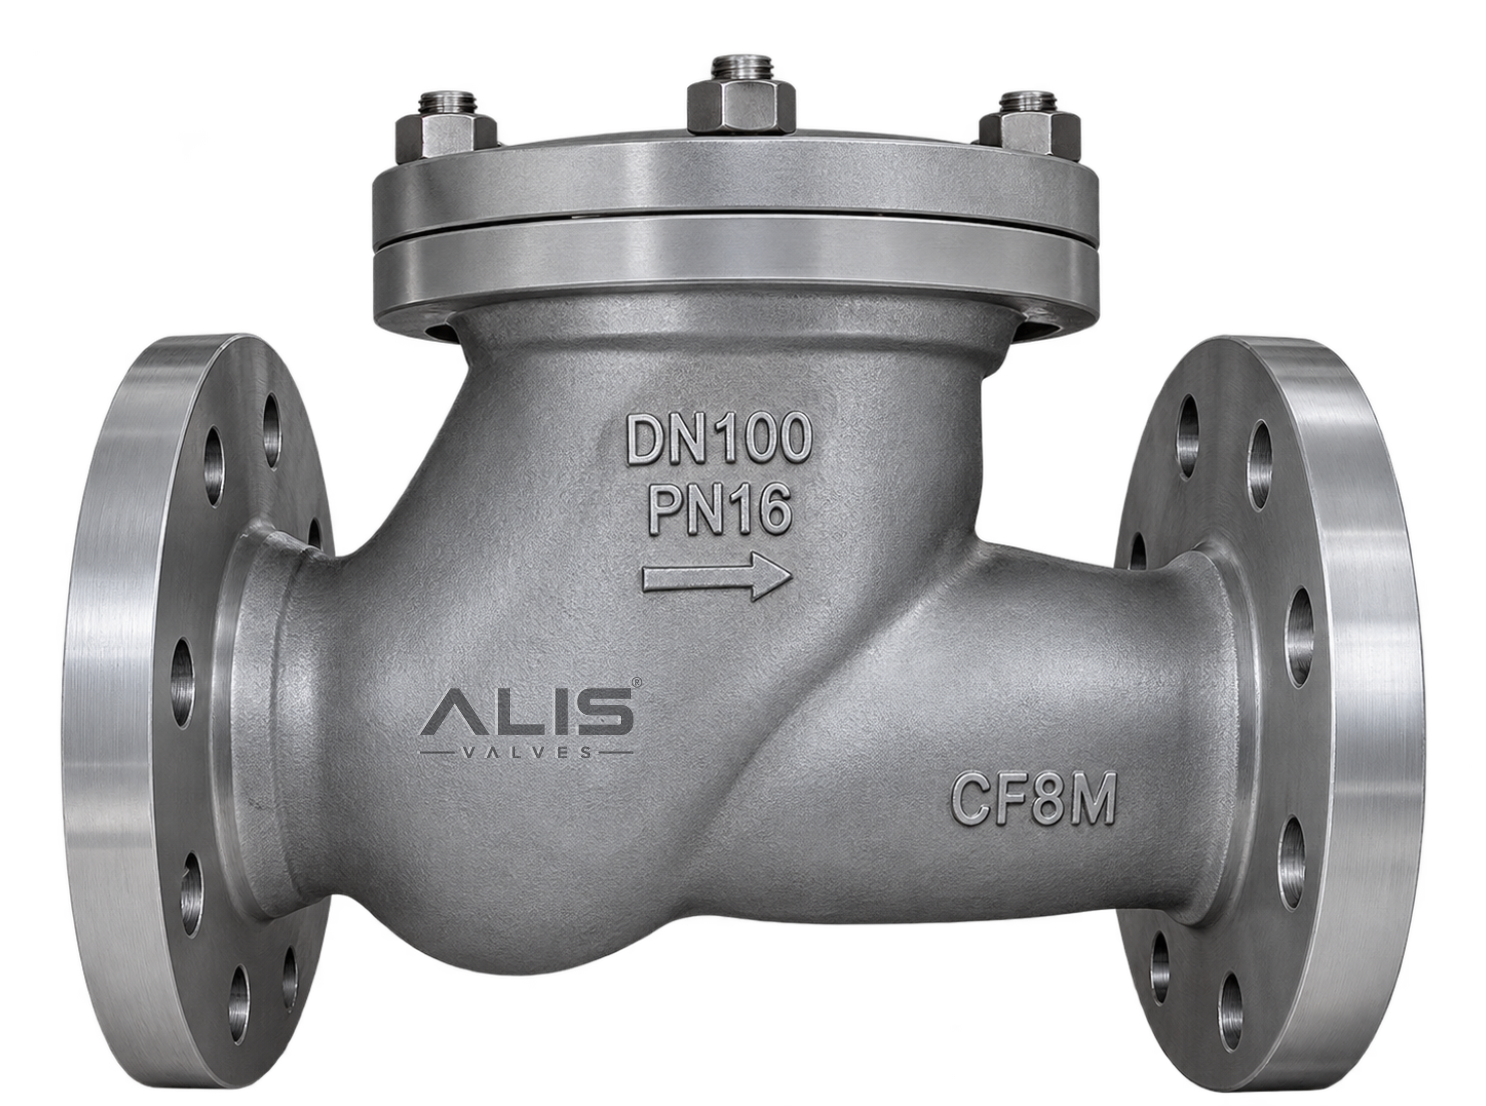
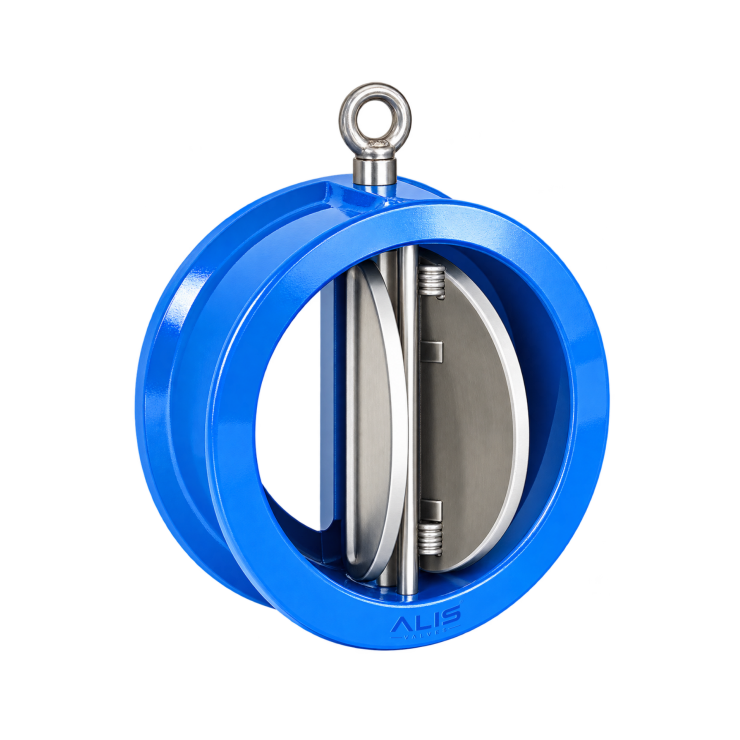
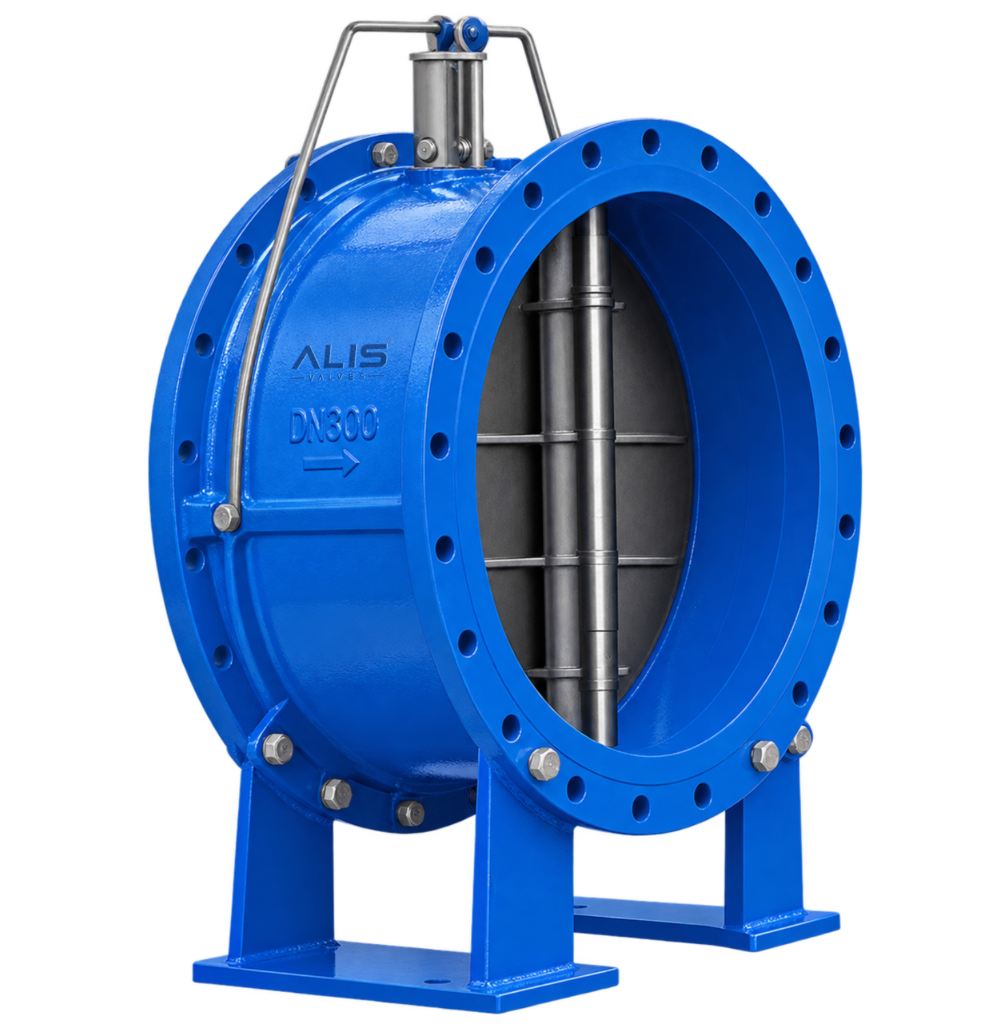
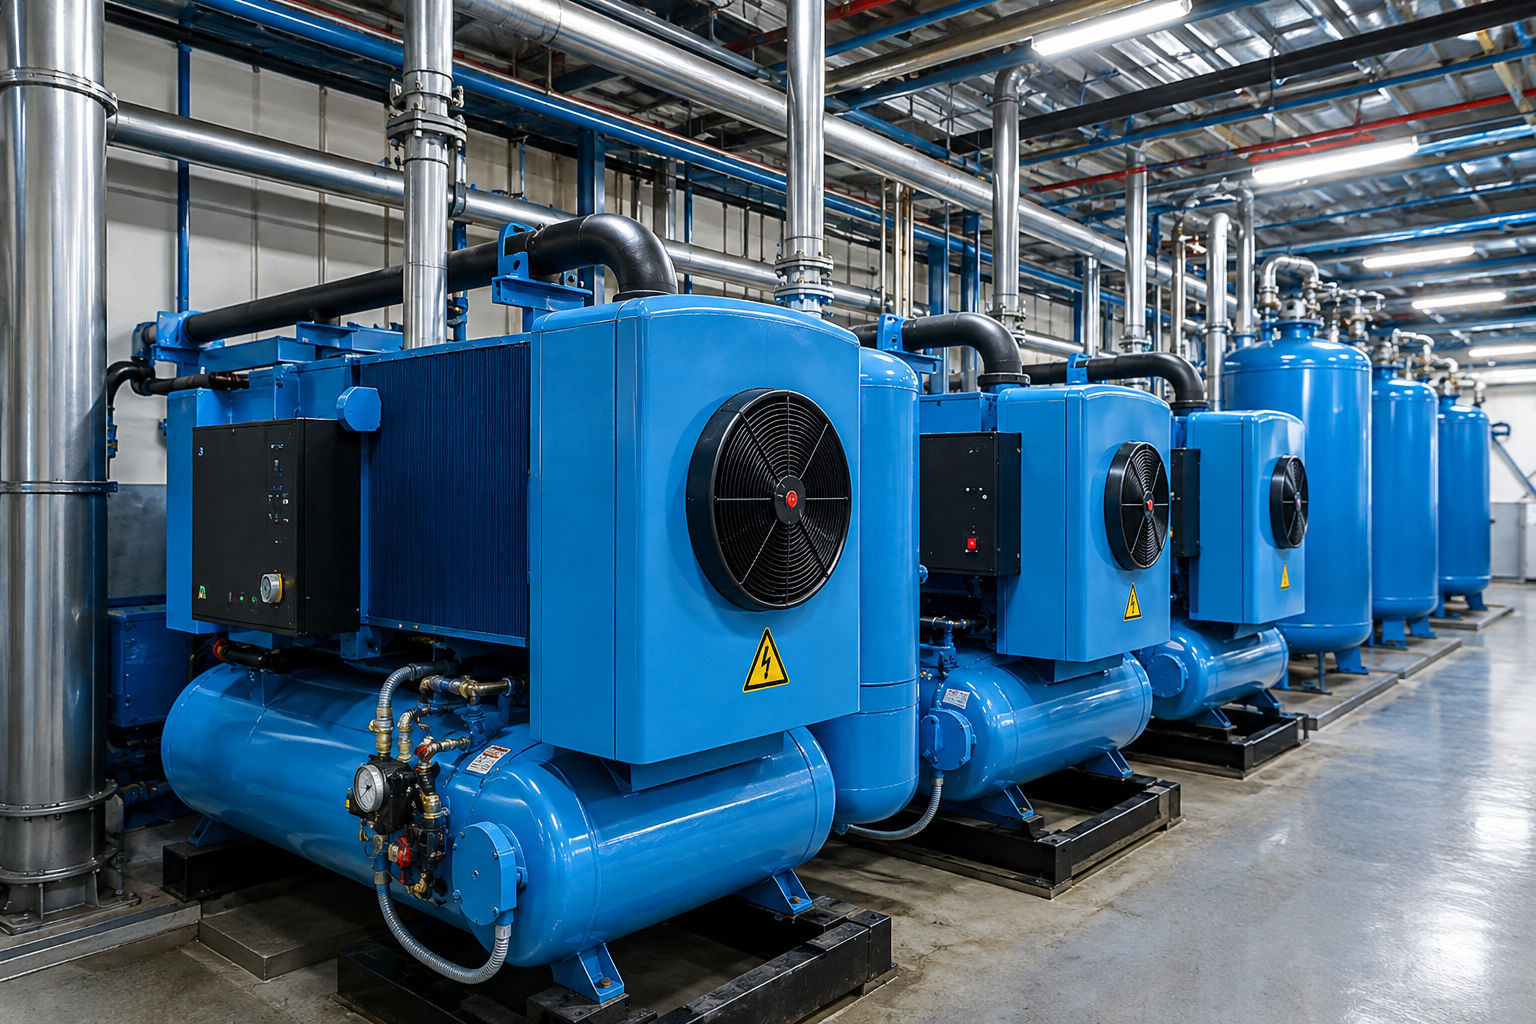
High-performance flow automation engineered for Compressed Air operations.
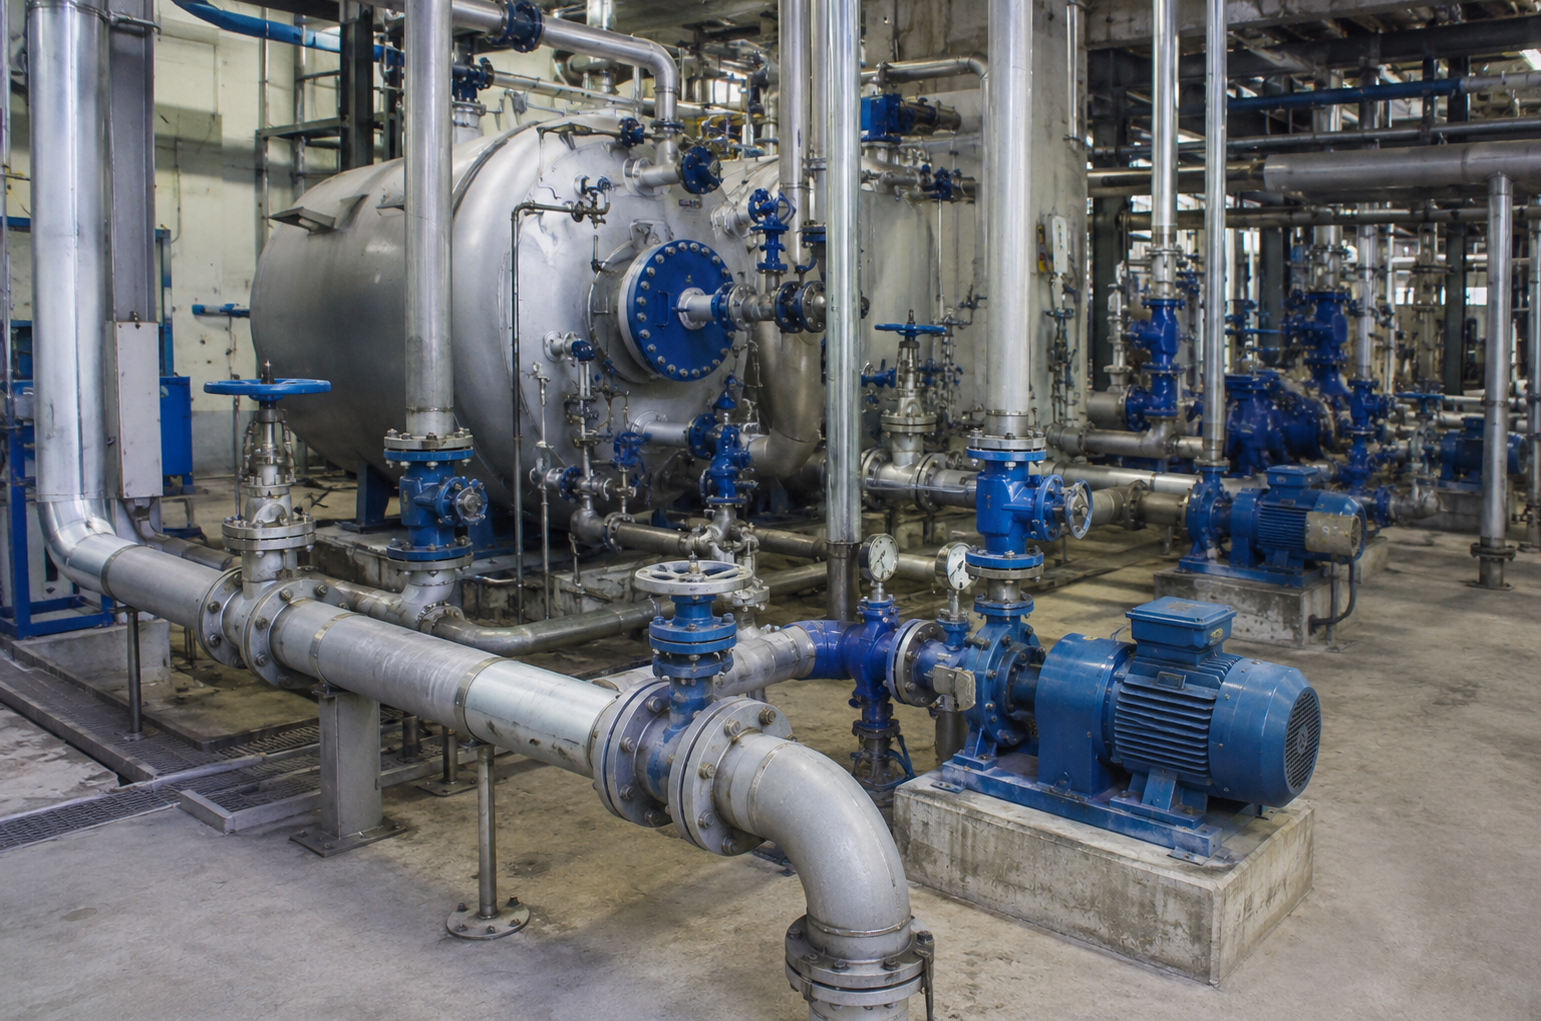
High-performance flow automation engineered for High Pressure operations.
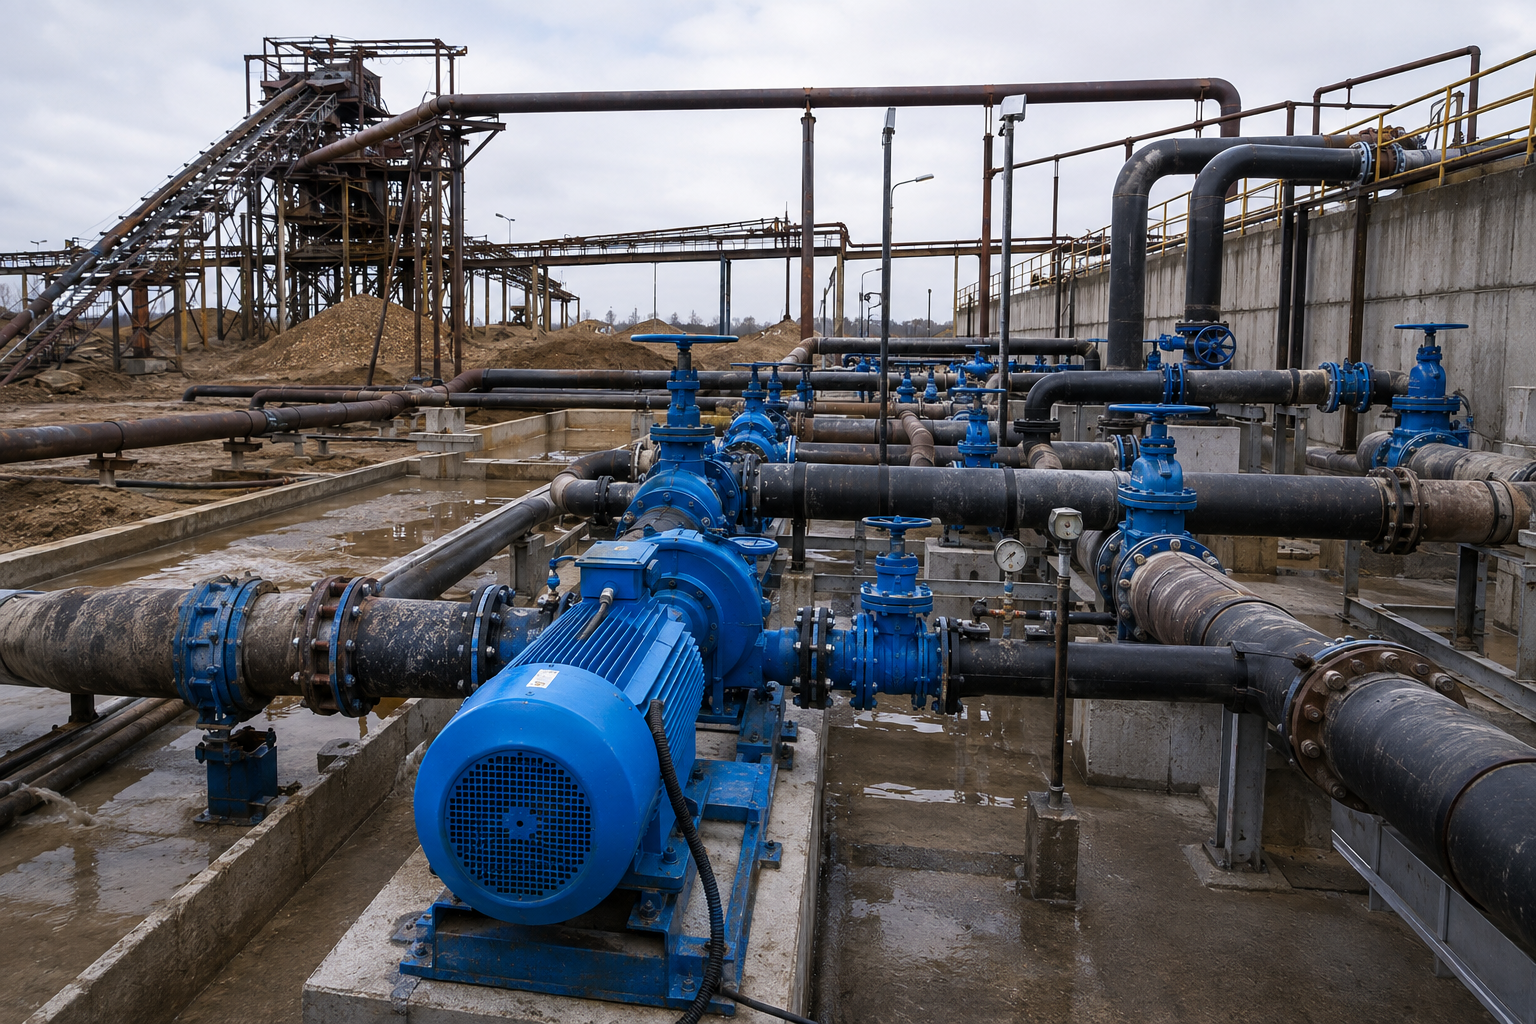
High-performance flow automation engineered for Slurry operations.
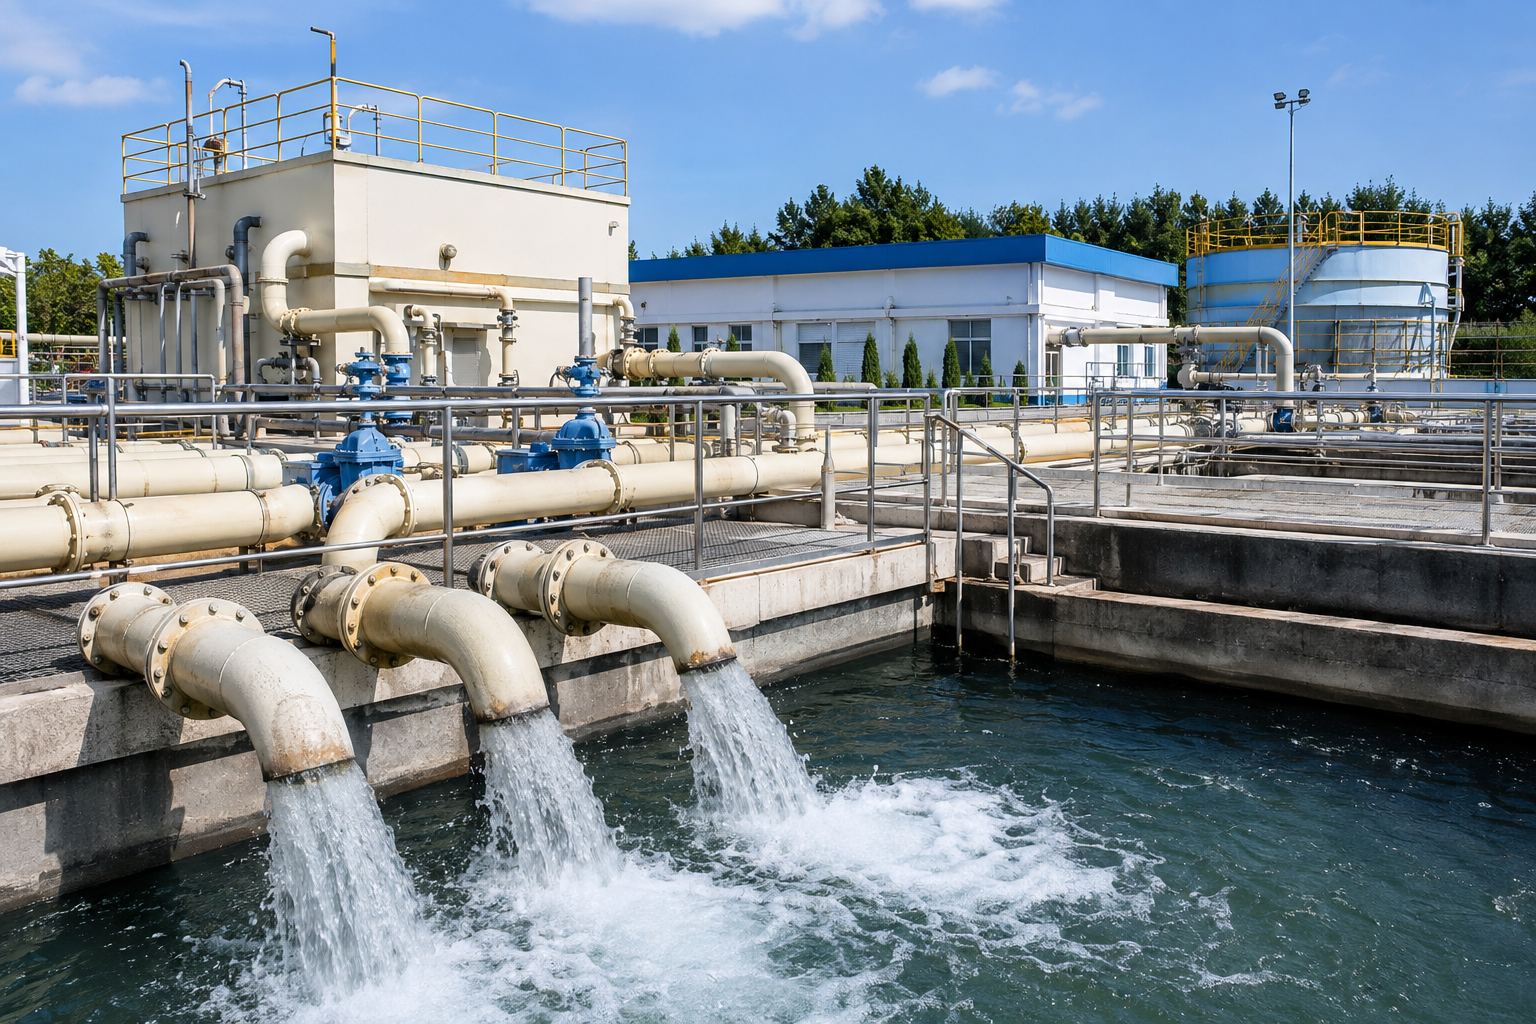
High-performance flow automation engineered for Water operations.
Ball Check Valve Product Brochure
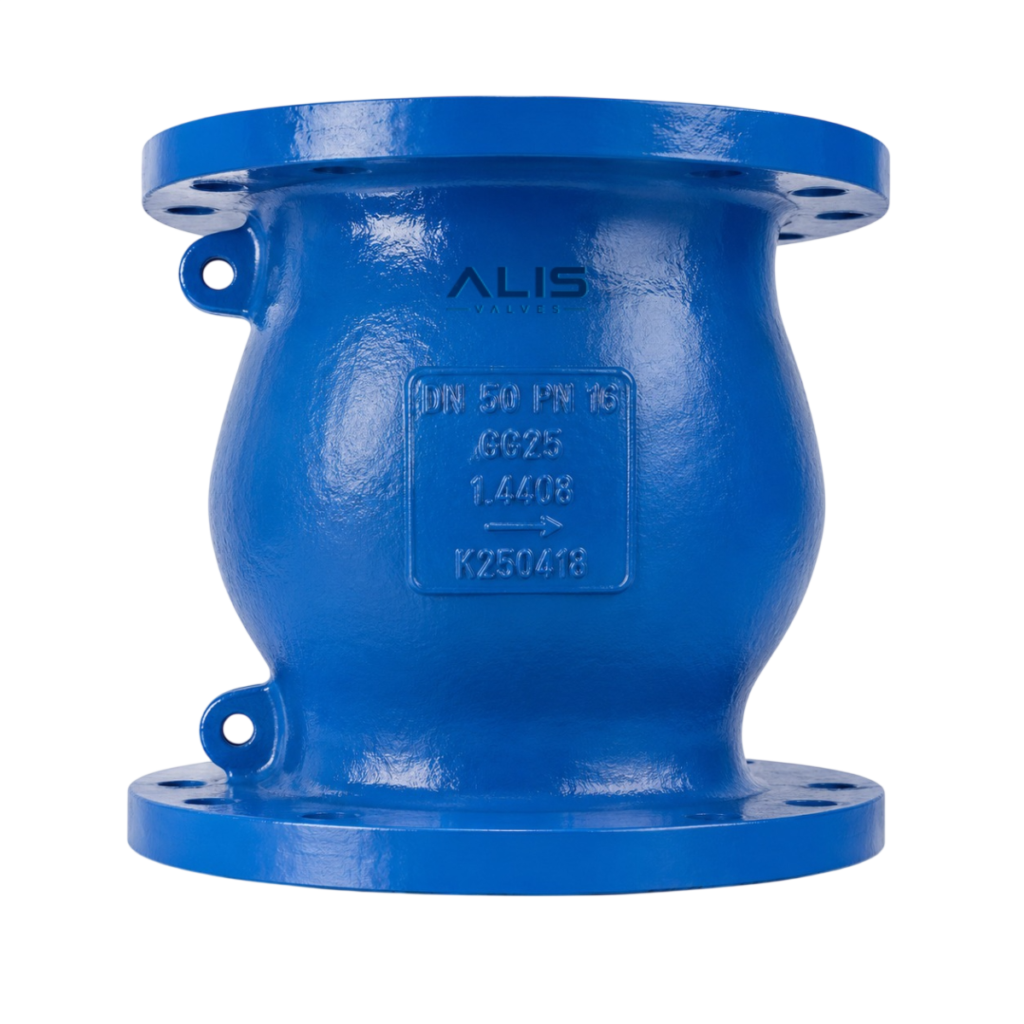
Axial Flow Check Valve Manufacturer Supplier in India is designed for reliable…
Alis Valves is a leading Dual Plate Check Valve Manufacturer & Supplier…
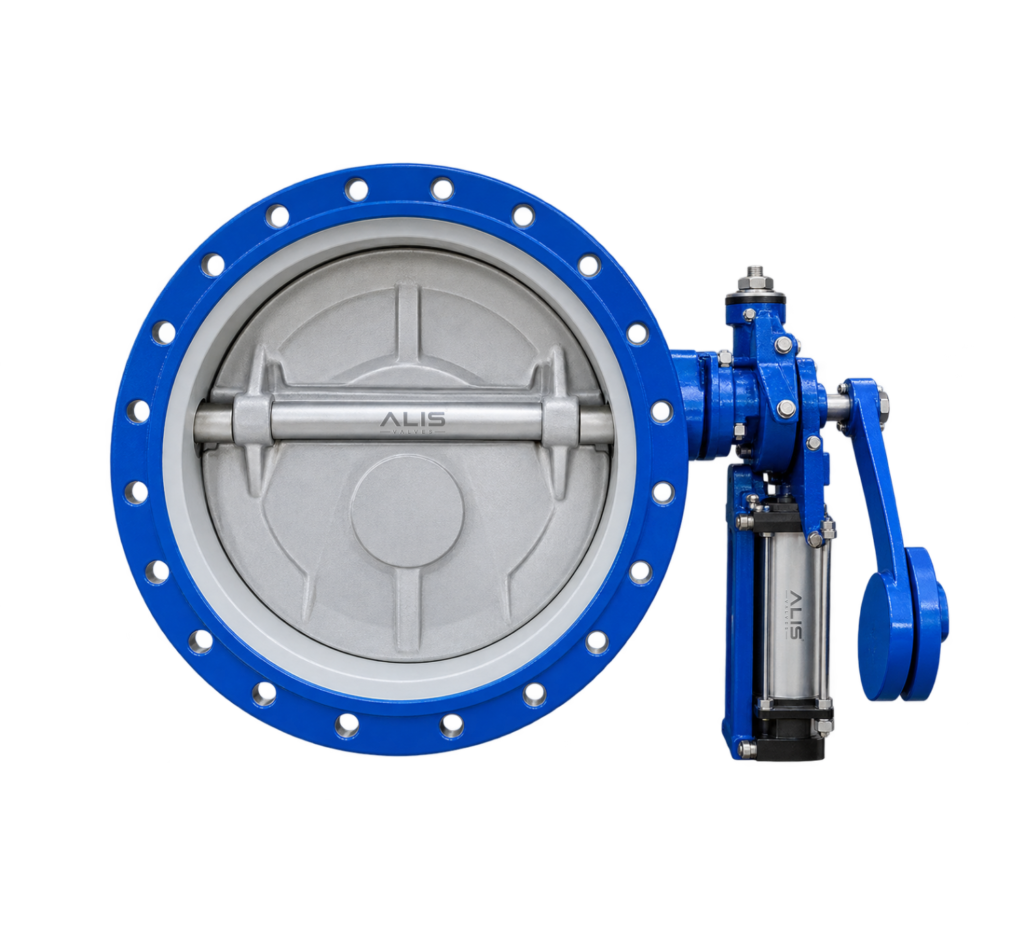
Alis Valves is an Pneumatic Closing Check Valve Manufacturer Supplier in India…
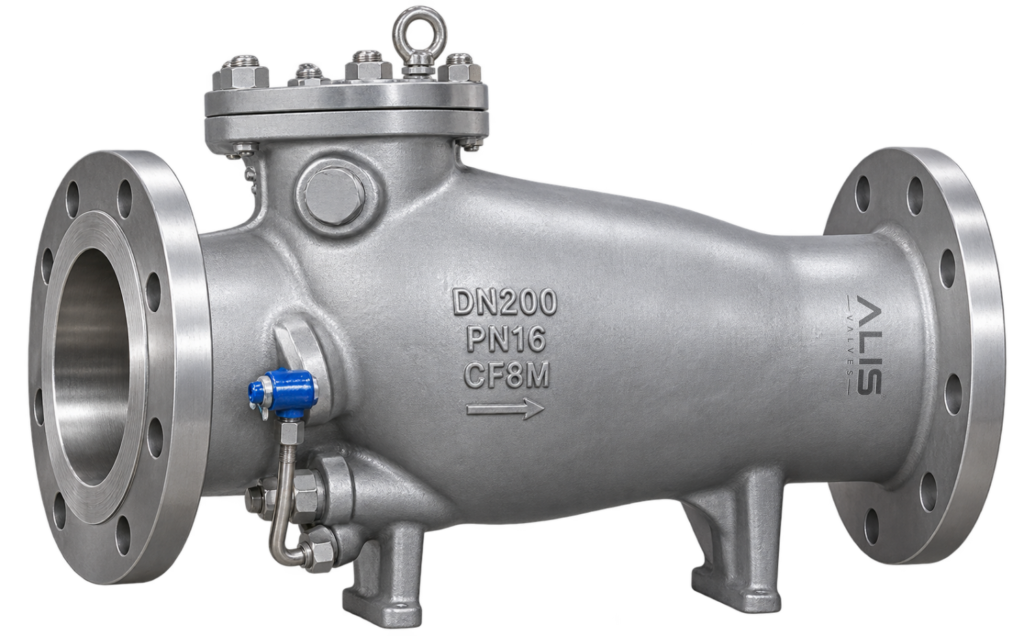
Alis Valves is an Resistance Slow Closing Check Valve Manufacturer in India…