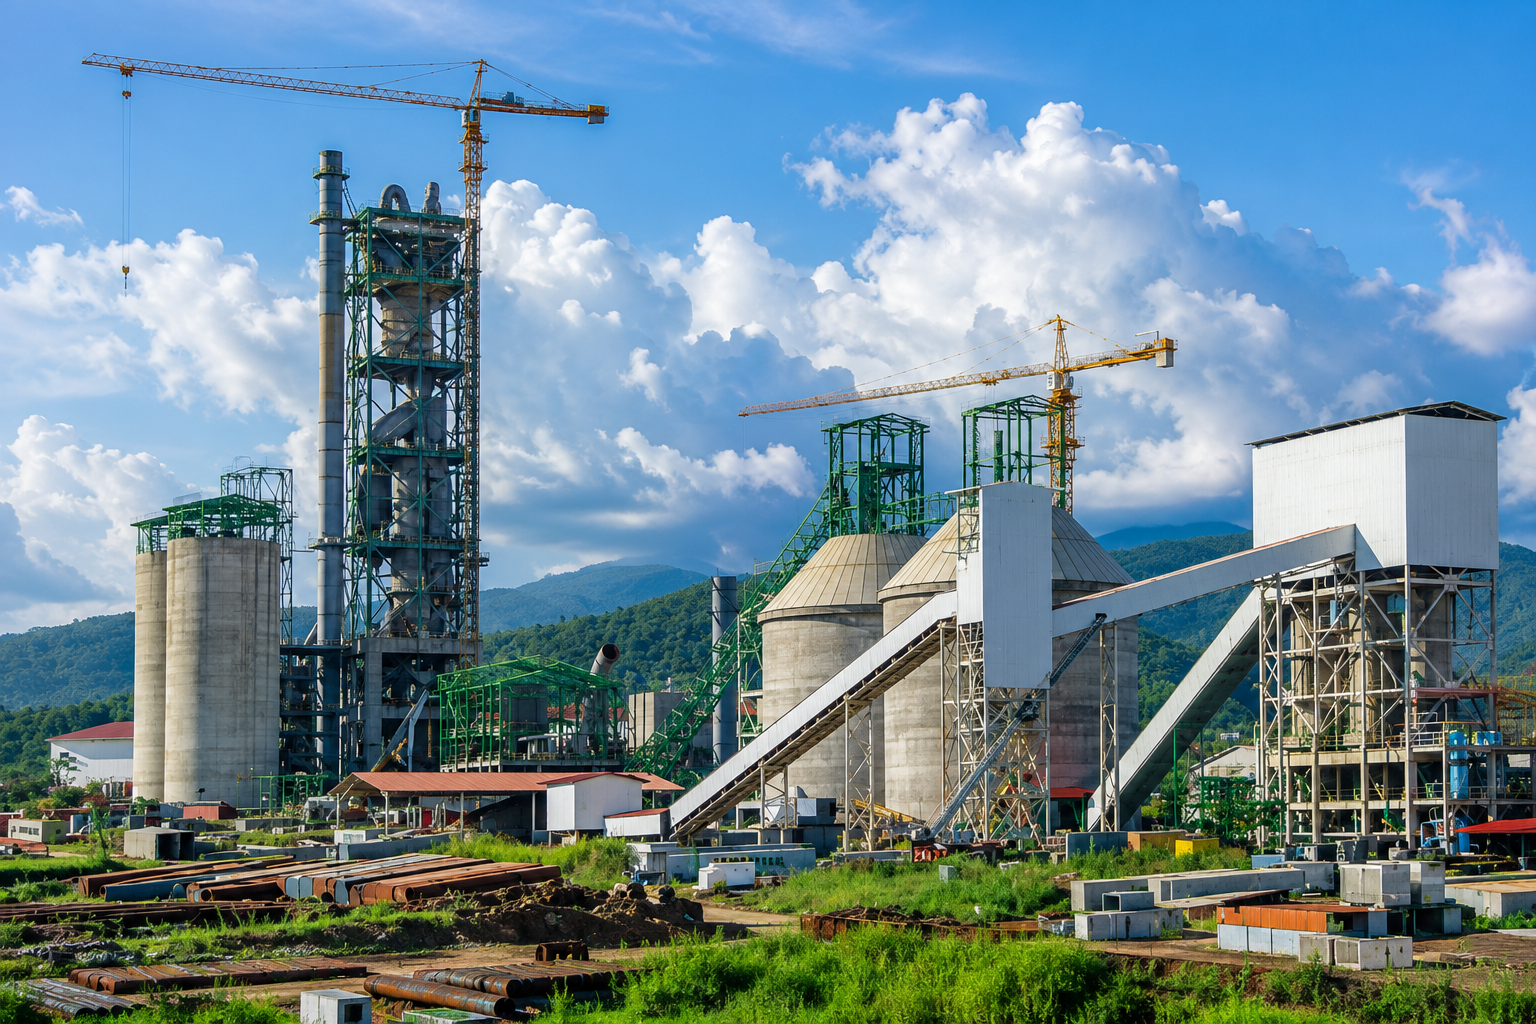
Cement
Engineered valve solutions tailored for critical Cement operating processes.
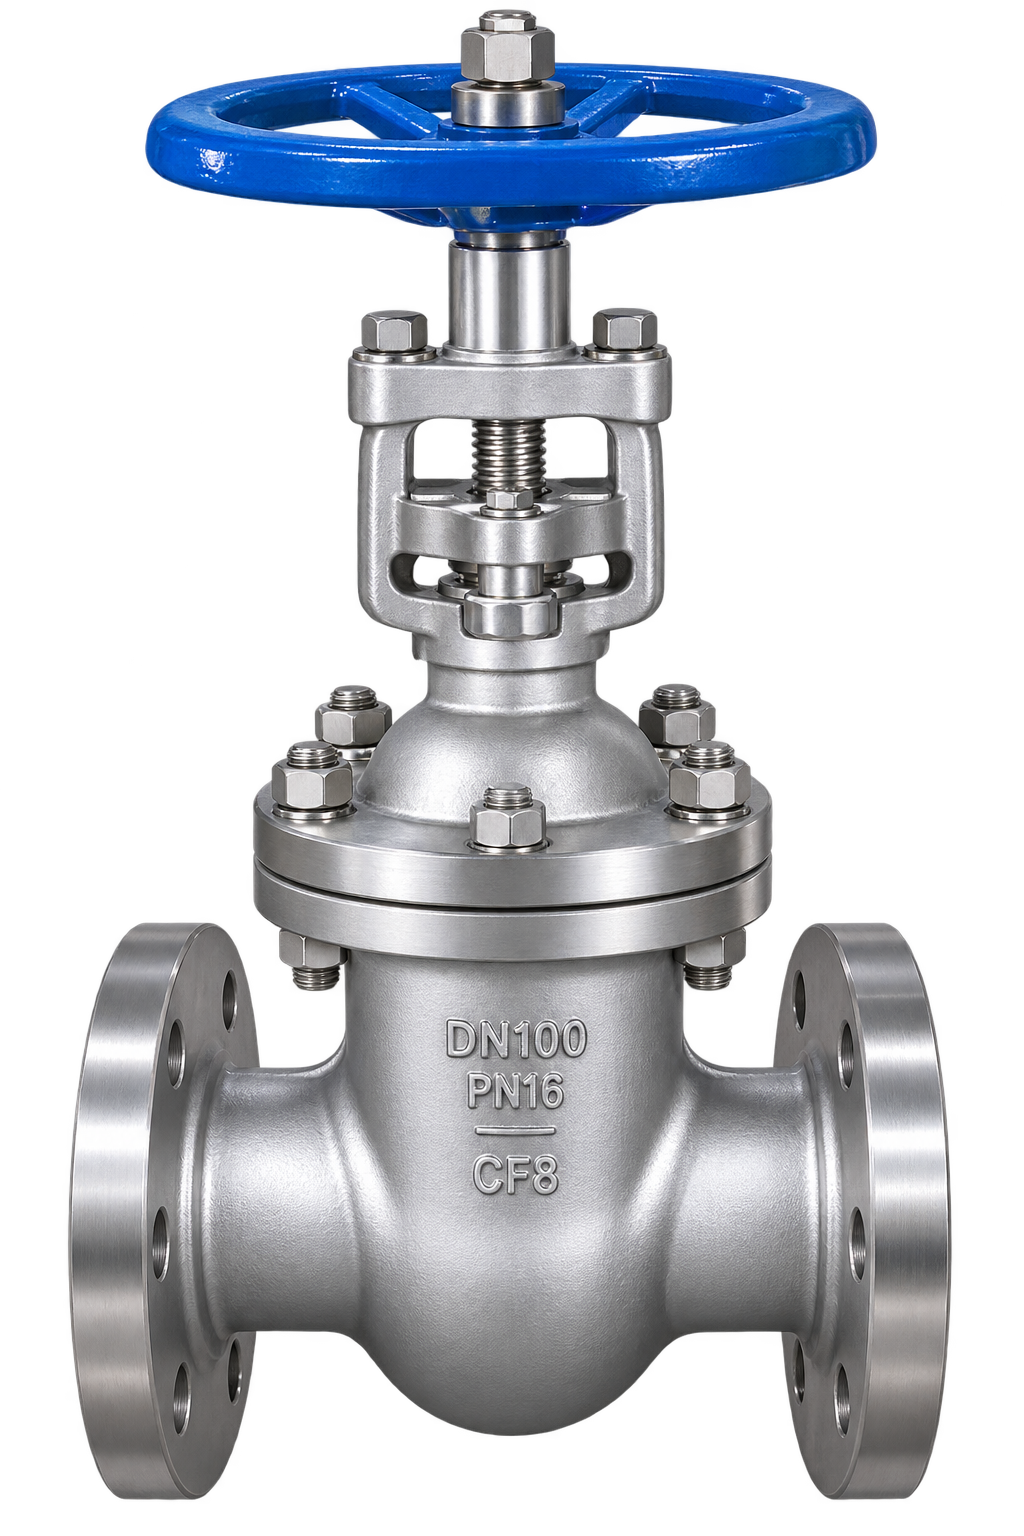
Alis Valves offers durable Non-Rising Stem Gate Valves designed for applications where space is limited and compact installation is required. In this design, the stem rotates to open or close the valve without moving vertically, making it ideal for underground and confined installations. Engineered for reliability and efficiency, non-rising stem gate valves provide tight shut-off, smooth operation, and long-lasting performance in water distribution, fire protection, and industrial systems.
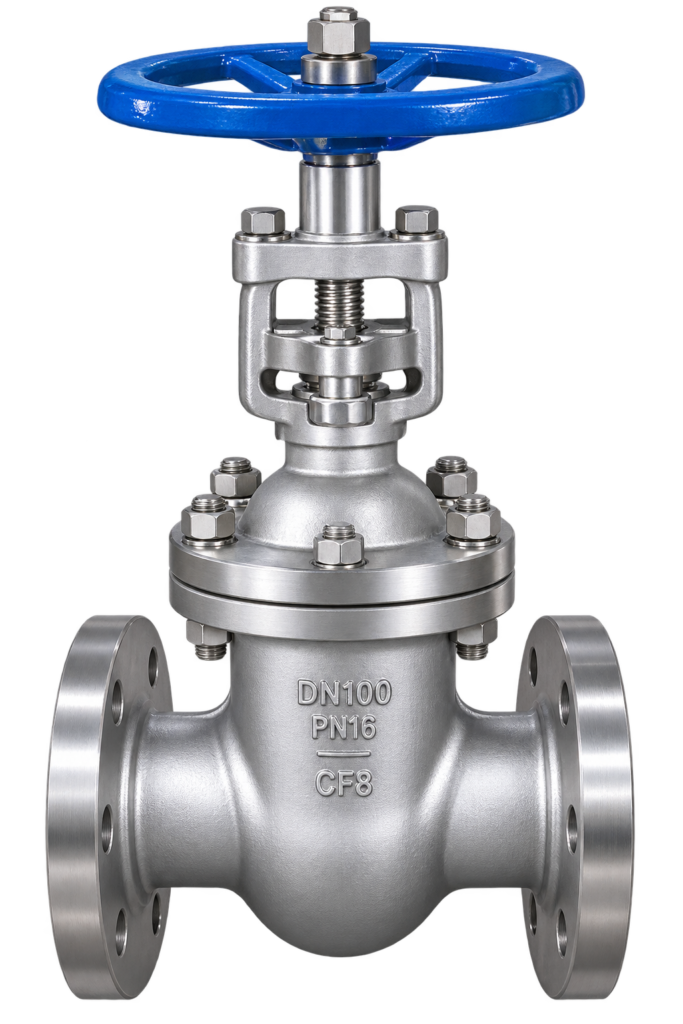
Alis Valves offers durable Non-Rising Stem Gate Valves designed for applications where space is limited and compact installation is required. In this design, the stem rotates to open or close the valve without moving vertically, making it ideal for underground and confined installations. Engineered for reliability and efficiency, non-rising stem gate valves provide tight shut-off, smooth operation, and long-lasting performance in water distribution, fire protection, and industrial systems.
Size Range
DN 50 to DN 1200
Pressure Rating
PN 10 / PN 16 / PN 25
Body Material
Cast Iron / Ductile Iron / Stainless Steel
Gate Material
Ductile Iron / Stainless Steel
Seat Material
EPDM / NBR / Metal Seated
End Connection
Flanged
Operation
Manual / Gear / Electric Actuated
Temperature Range
Up to 120°C (Depends on Seat Material)
Media
Water, Wastewater, Oil
Engineered valve solutions tailored for critical Cement operating processes.
Engineered valve solutions tailored for critical Chemical operating processes.
Engineered valve solutions tailored for critical Data centres operating processes.
Engineered valve solutions tailored for critical Fertilizer operating processes.
High-performance flow automation engineered for Ammonia operations.
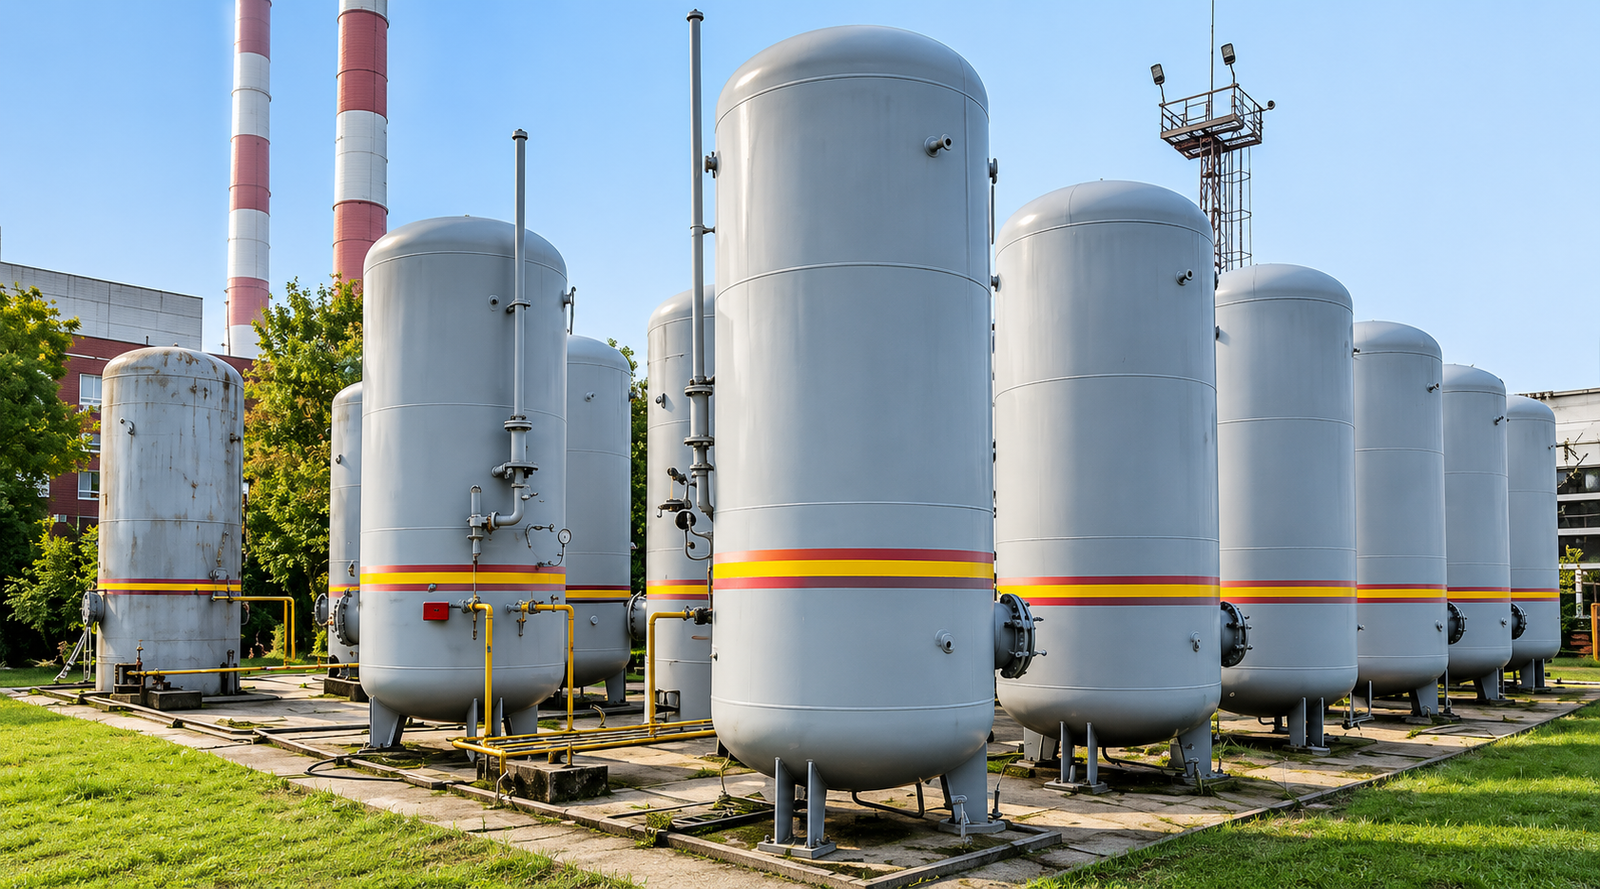
High-performance flow automation engineered for CO₂ operations.
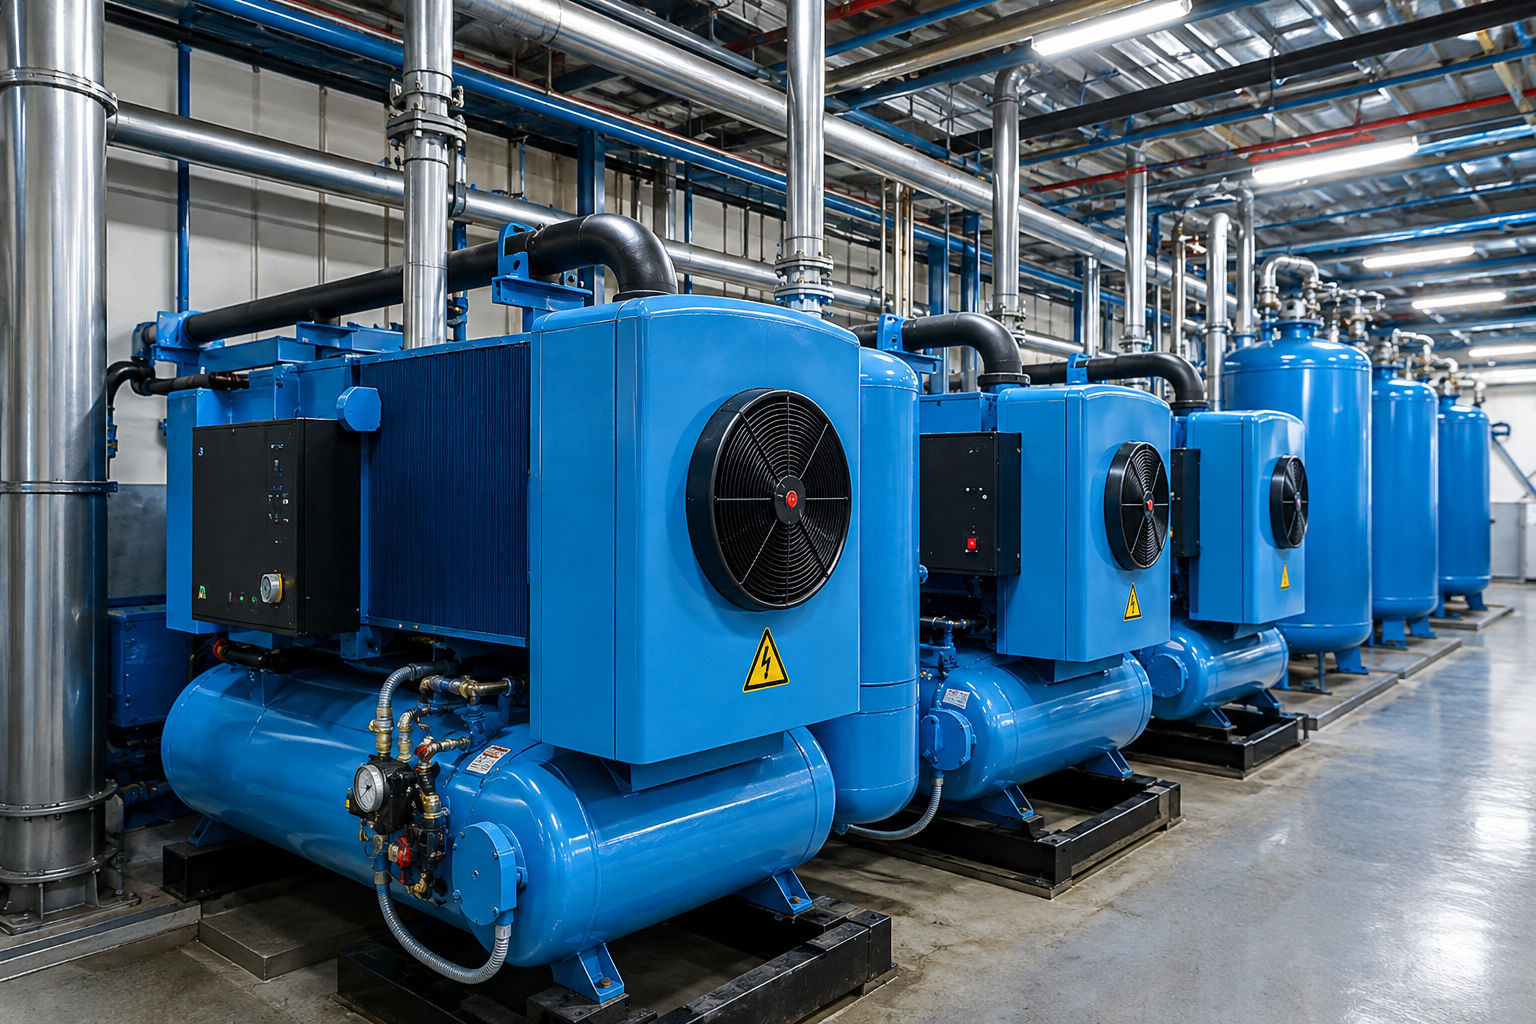
High-performance flow automation engineered for Compressed Air operations.
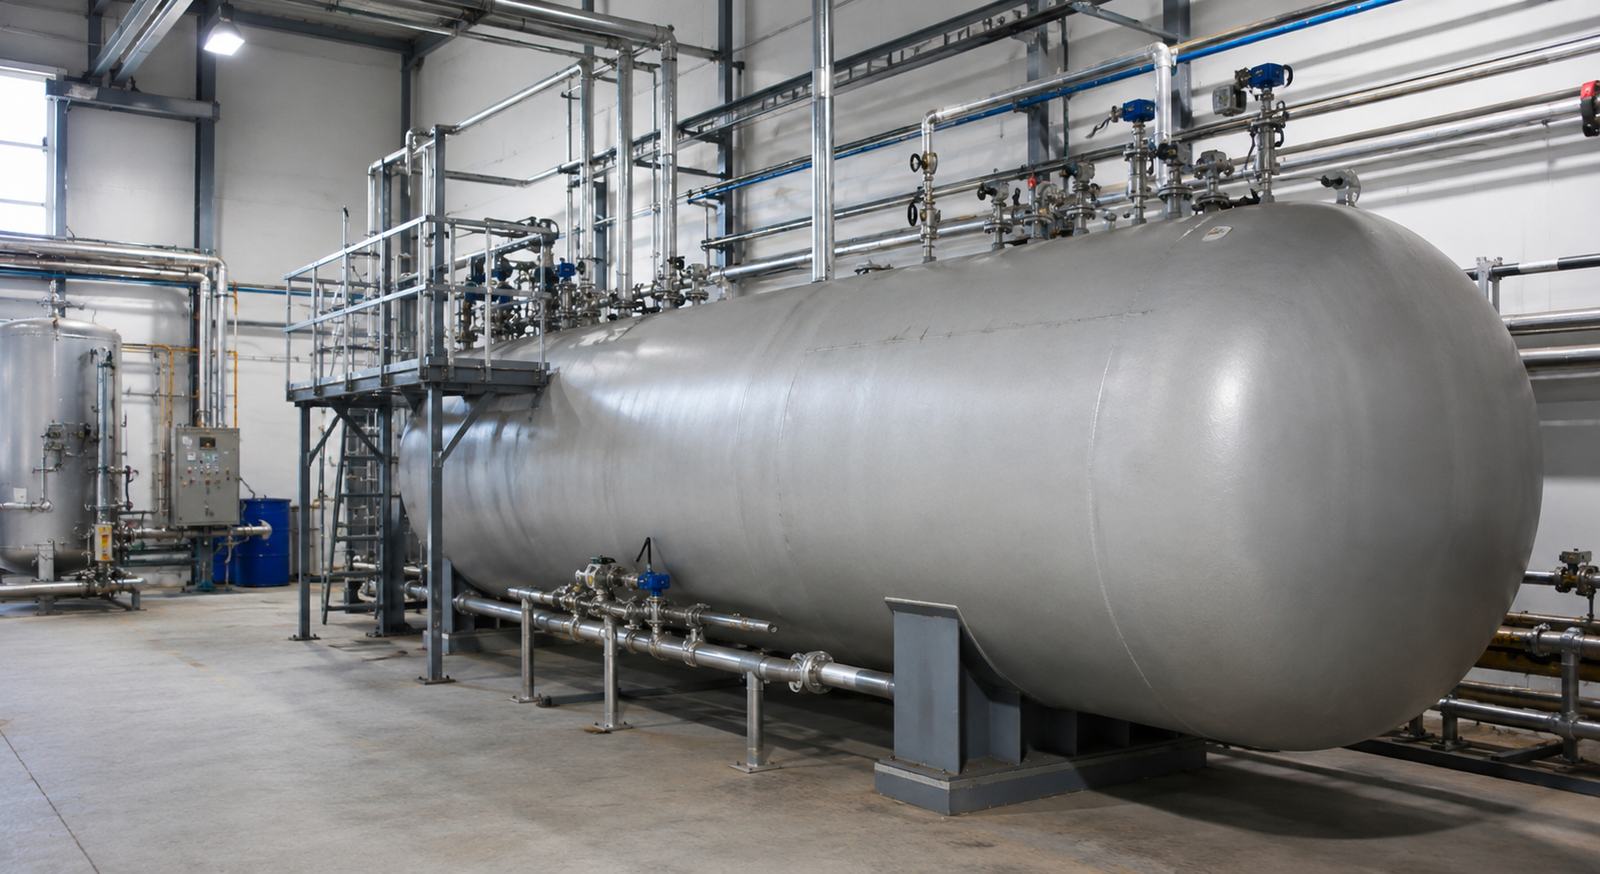
High-performance flow automation engineered for Cryogenic operations.
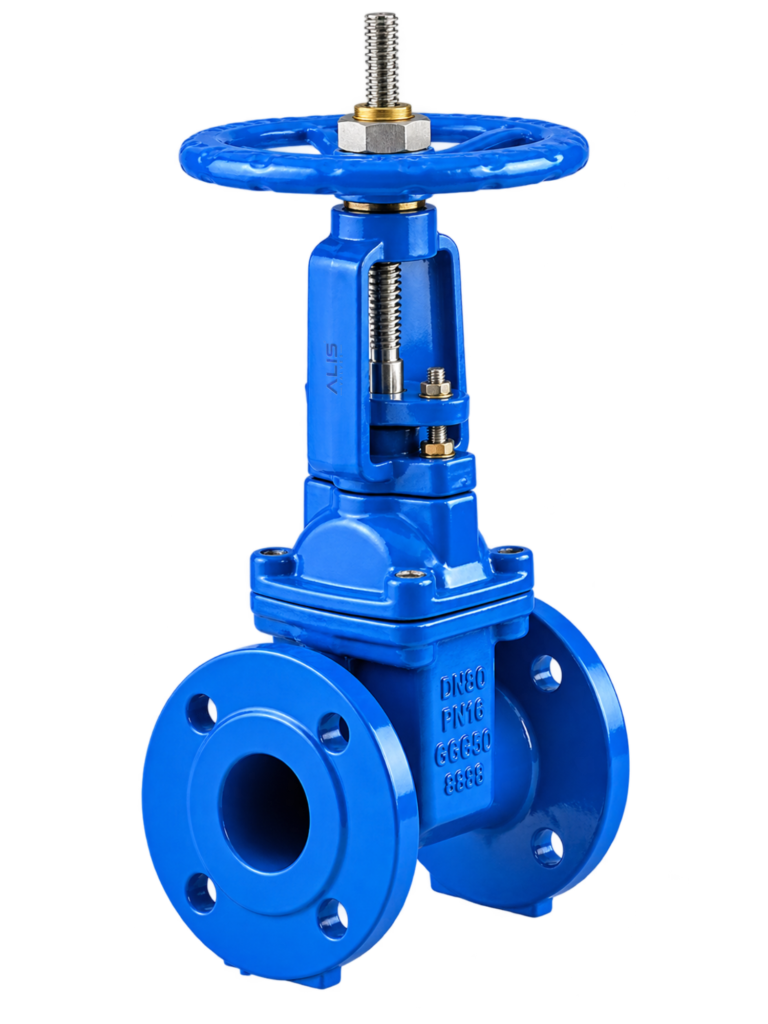
Alis Valves offers high-quality Rising Stem Gate Valves designed for reliable isolation…
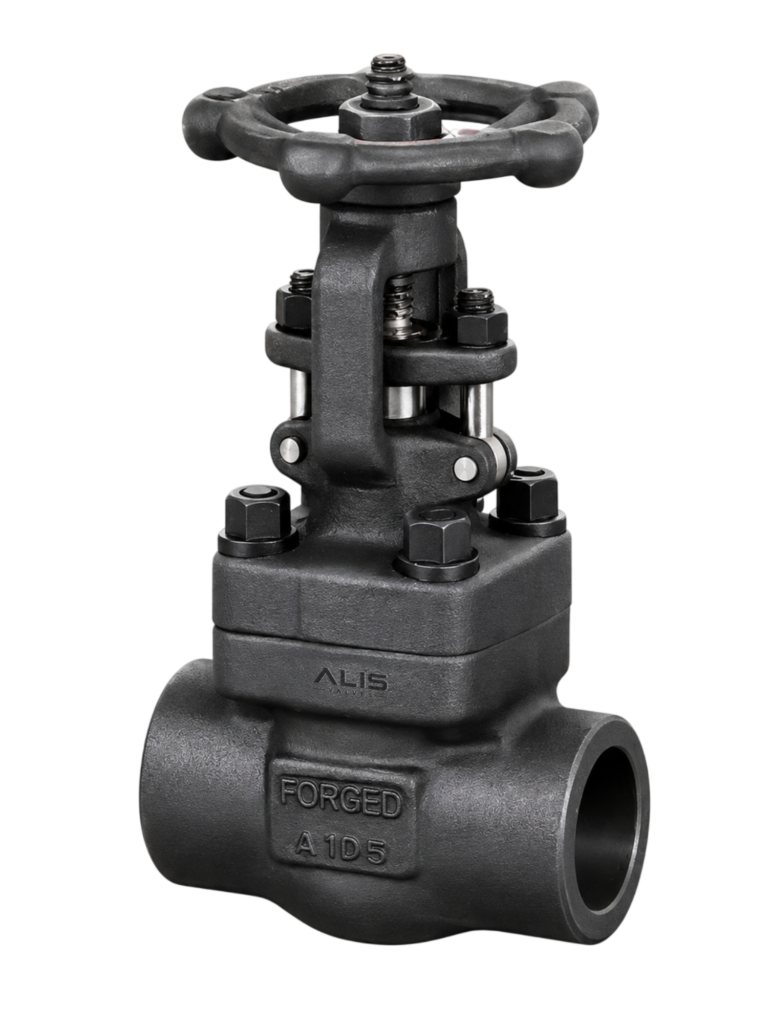
ALIS Valves is a Forged Steel Gate Valve Manufacturer in India, offering…
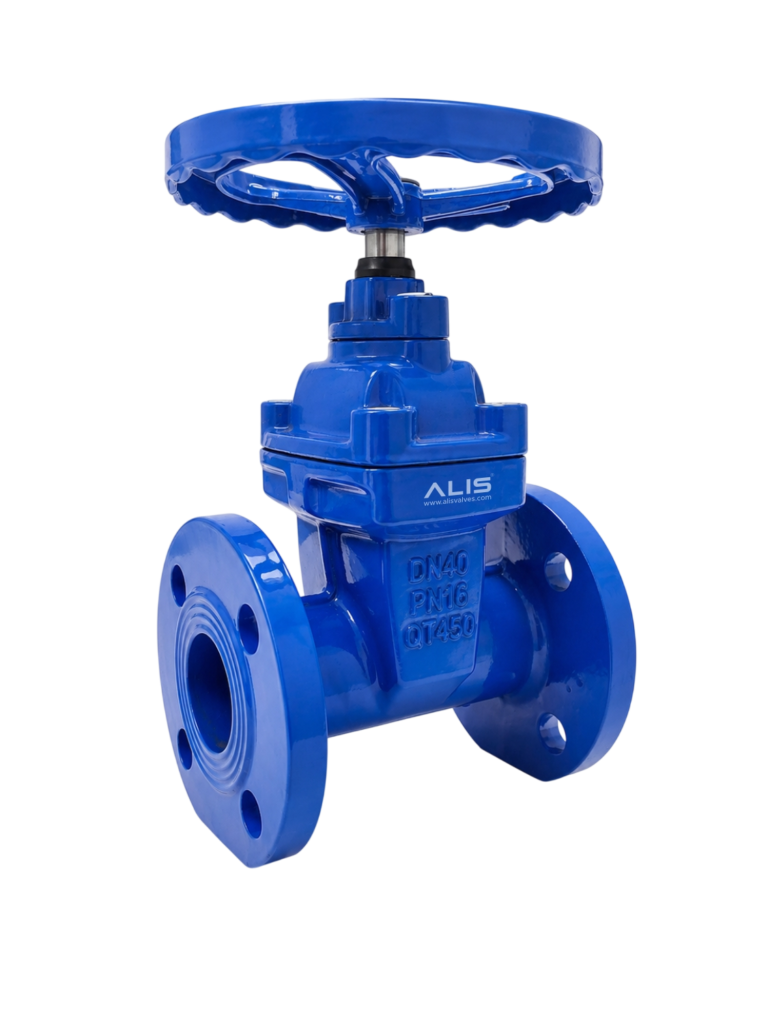
ALIS Valves is a leading Resilient Seated Gate Valve Manufacturer & Supplier…
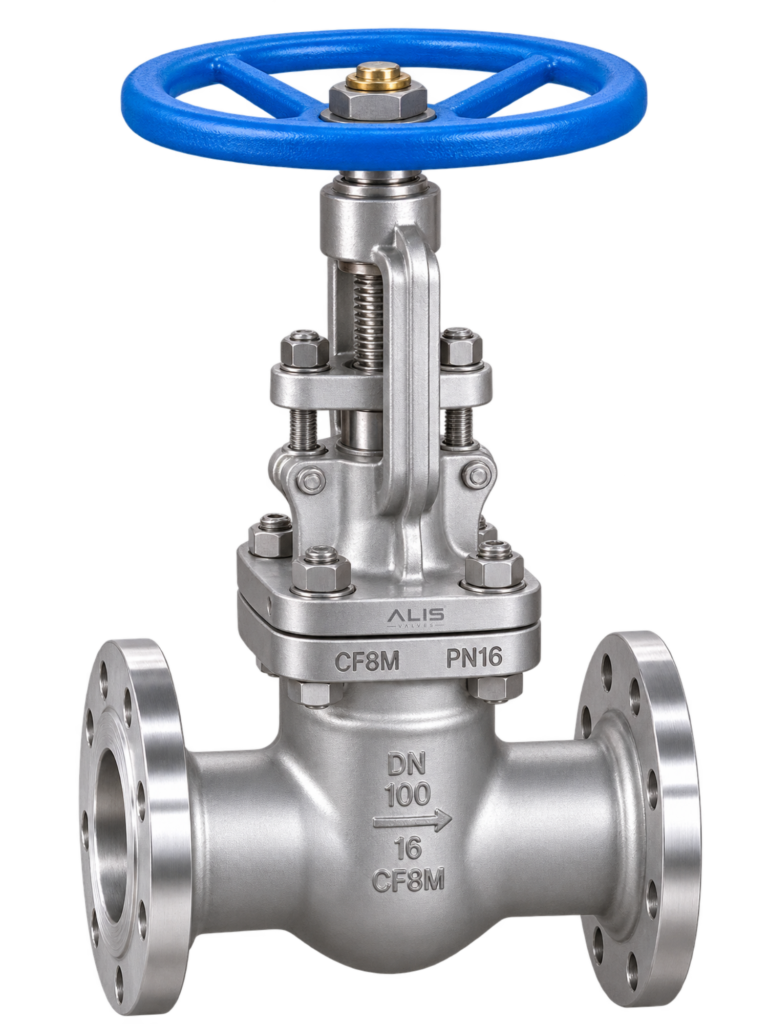
Alis Valves offers high-performance Metal Seated Gate Valves designed for demanding applications…