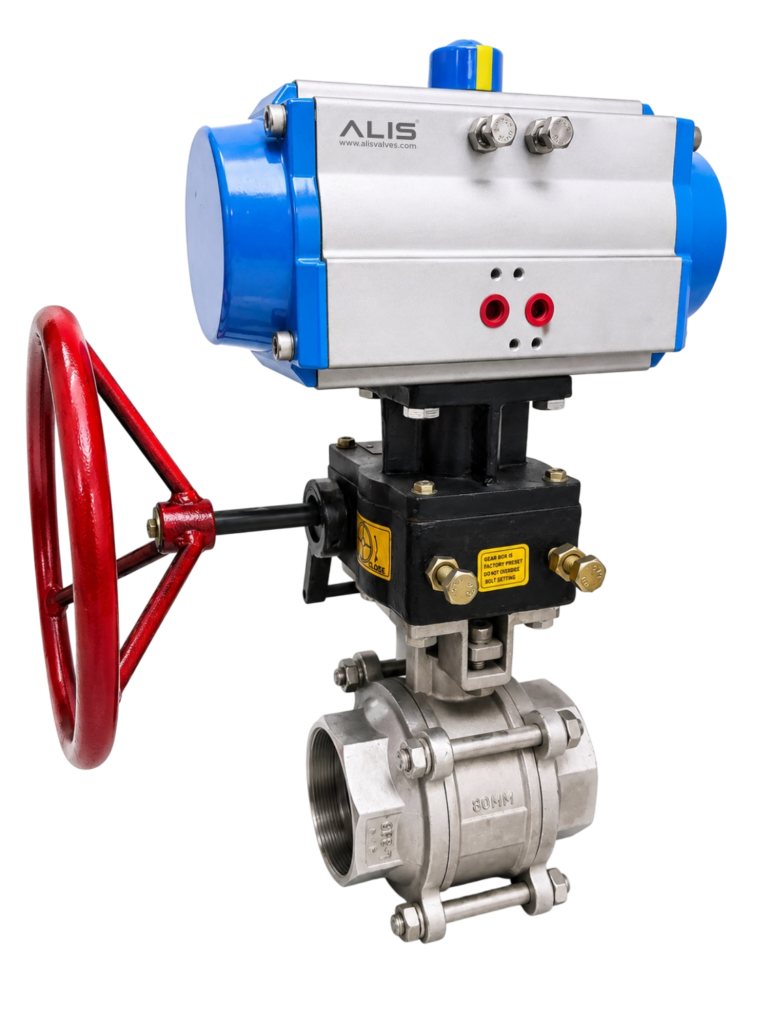
BALL VALVES
Pneumatic Screwed Ball Valve
ALIS Valves is a Pneumatic Screwed Ball Valve Manufacturer Supplier in India,…
Engineered for Safety, Reliability & Performance in Demanding Process Applications
Alis Valves Ammonia application valves manufacturer in India, engineered for reliable flow isolation and control across ammonia production, storage, transportation, refrigeration, chemical processing, and emerging low-carbon ammonia systems. Our range includes ball valves, gate valves, globe valves, check valves, butterfly valves, control valves, pneumatic actuated valves, and electric actuated valves, with configurations selected according to ammonia concentration, pressure, temperature, phase, material compatibility, and service requirements. Designed for demanding ammonia service, our valve solutions focus on reliable shut-off, corrosion resistance, tight sealing, low leakage, and dependable operation in critical ammonia infrastructure.
Industrial valves used in ammonia systems are selected according to the process medium, operating pressure, temperature and required flow-control function. Ball, gate, globe, check and butterfly valves may be used for isolation, flow regulation or backflow prevention, depending on the system design and service conditions.
For ammonia production, storage, refrigeration and transfer systems, engineers should verify valve material compatibility, seat and seal selection, pressure-temperature ratings and leakage requirements before finalizing a valve. The selection process should also account for whether the application involves anhydrous ammonia, aqueous ammonia or refrigerated ammonia.
ALIS Valves offers industrial valve configurations for process applications, subject to the specifications and operating limits of the selected valve model.
Valve Solutions for Ammonia
A wide range of high-performance valves designed to meet the critical demands of Ammonia applications.
ALIS Valves is a Pneumatic Screwed Ball Valve Manufacturer Supplier in India,…
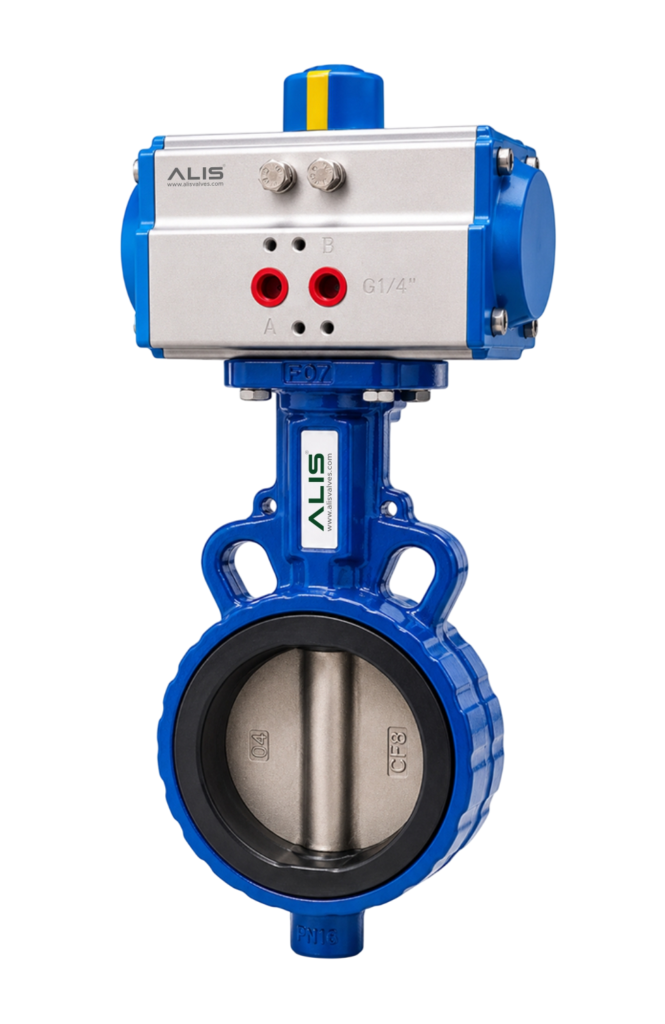
ALIS Valves is a leading Pneumatic Wafer Butterfly Valve Manufacturer in India,…
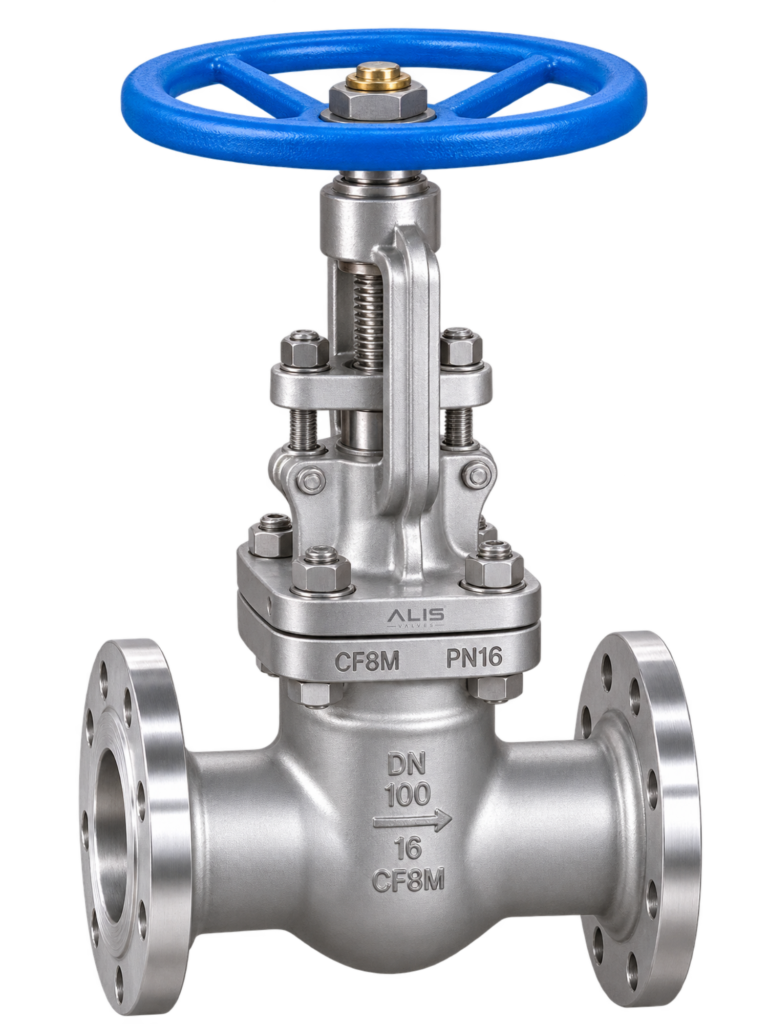
Alis Valves offers high-performance Metal Seated Gate Valves designed for demanding applications…
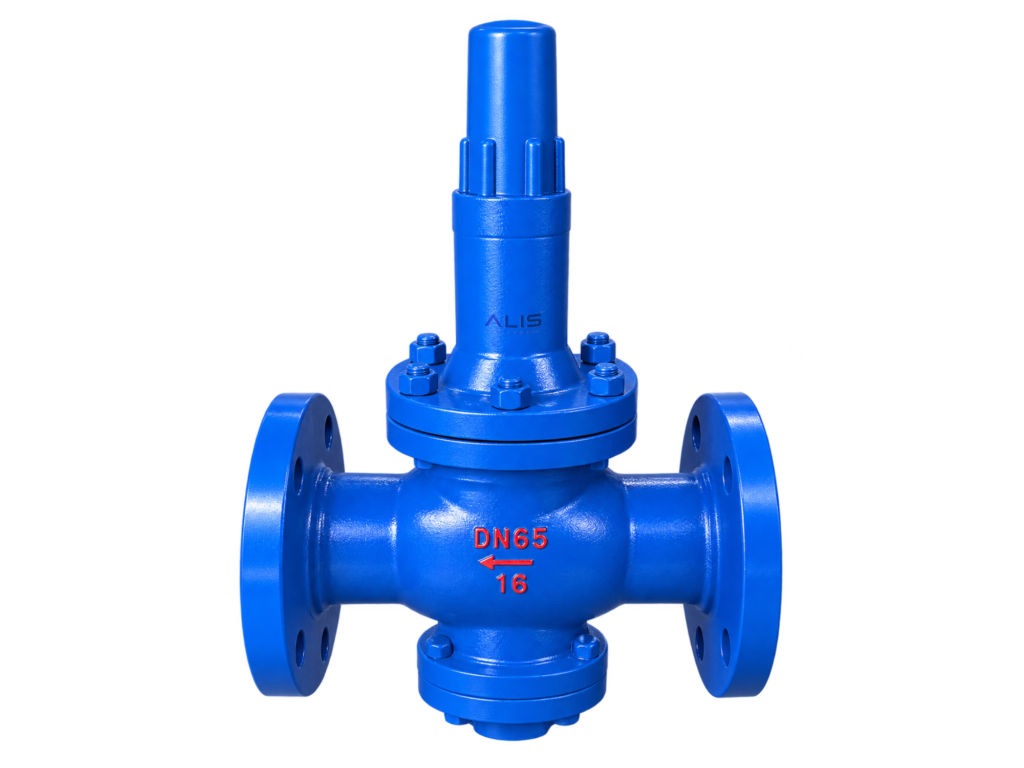
Alis Valves offers Direct Acting Pressure Reducing Valve Manufacturer Supplier India designed…
Product Categories for Ammonia
Explore key valve categories and automated packages engineered for Ammonia applications.
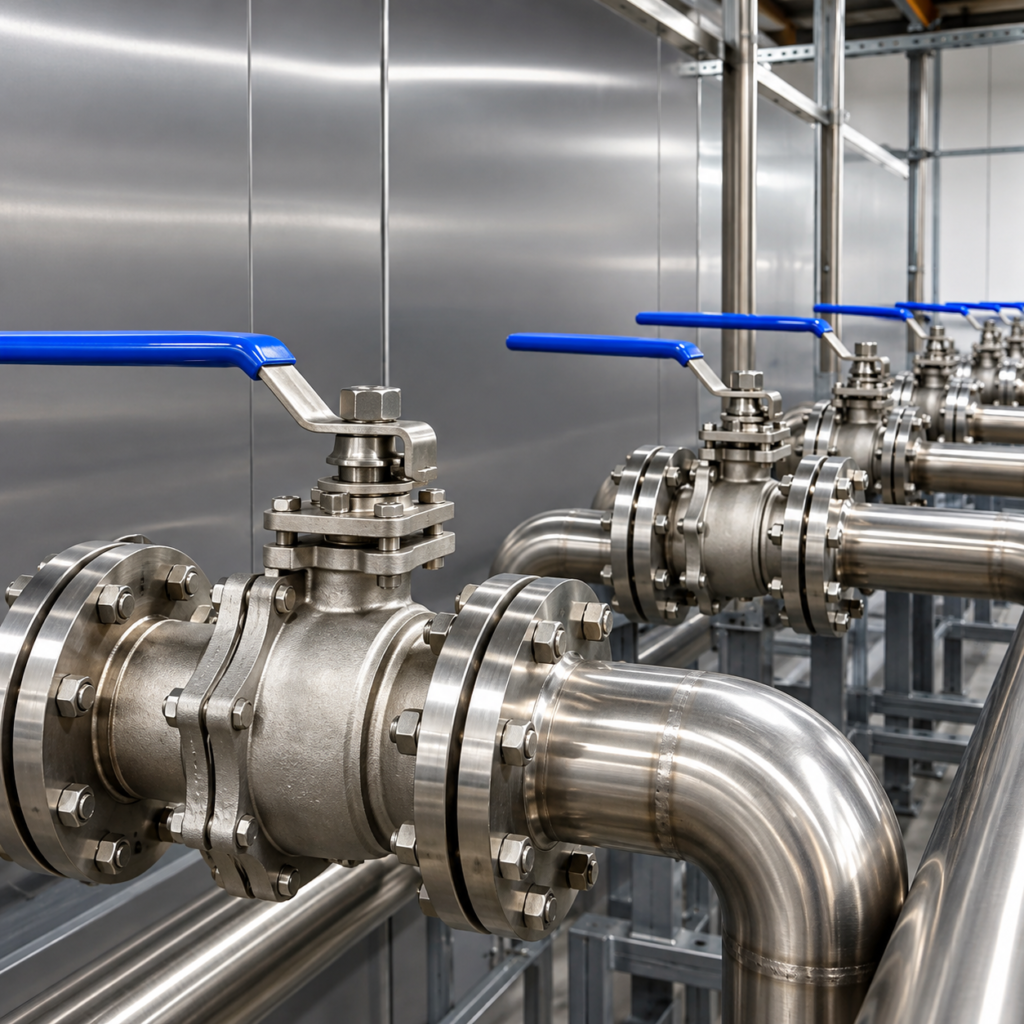
Designed around your needs, our Ball Valves deliver smooth operation, reliable shut-off, and the confidence you need for every flow…
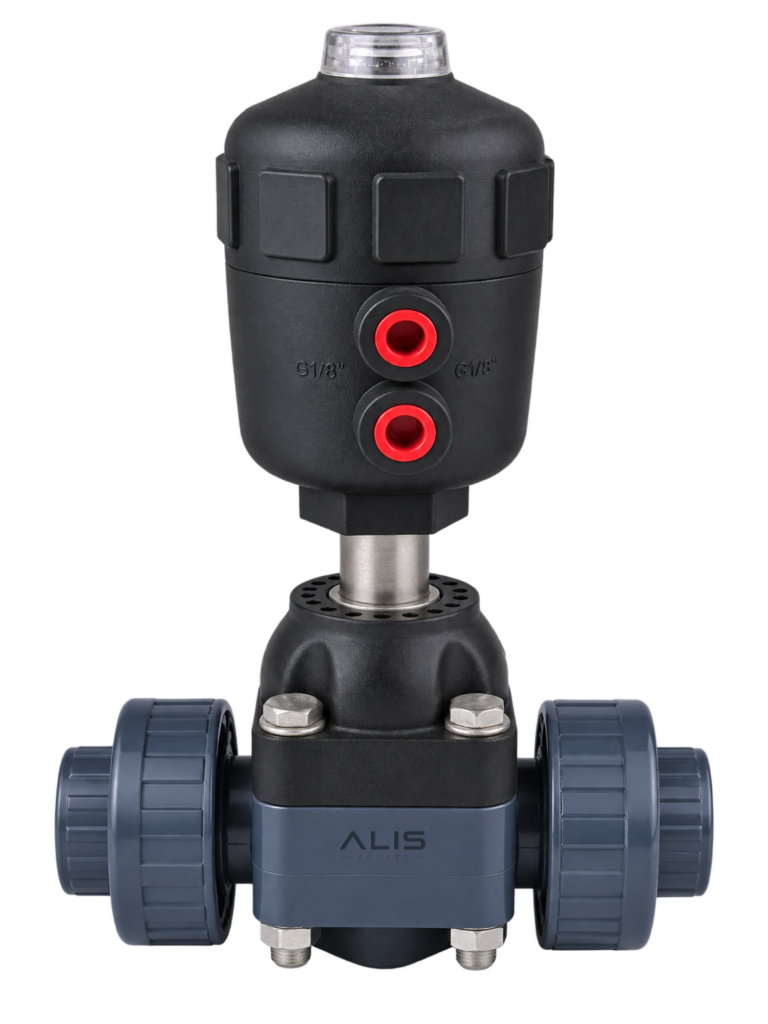
Complete Range of Pneumatic Actuated Ball, Butterfly, Gate, Globe and Control Valves for Reliable Industrial Automation and Precise Flow Control.
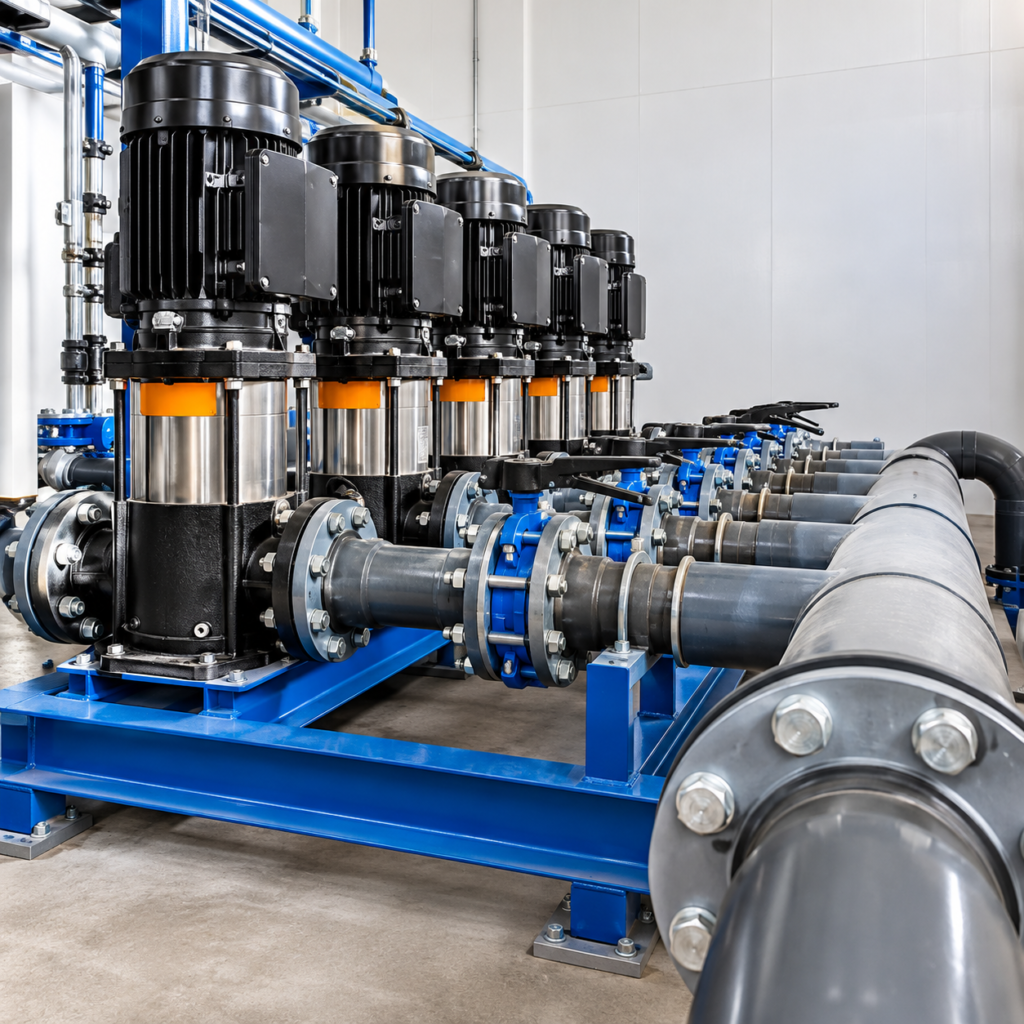
Designed for effortless flow control, our Butterfly Valves combine easy operation, dependable shut-off, and durable performance to keep your processes…

Engineered Gate Valve engineered for superior reliability and severe service performance.
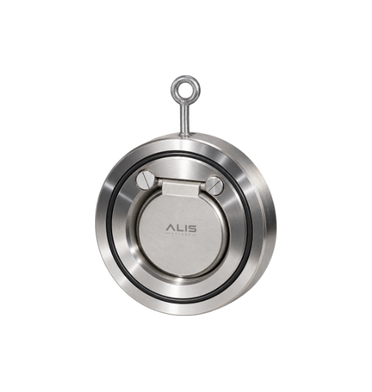
GGC Valves designed to deliver dependable shut-off, precise flow control, and effective non-return protection in demanding industrial process applications.
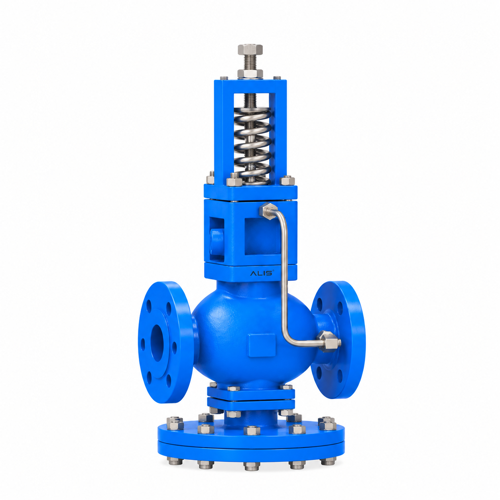
Pressure Reducing Valves engineered to maintain constant outlet pressure while protecting pipelines and equipment from excessive pressure. Ideal for power…
AMMONIA PROCESS SOLUTIONS
Industrial valve solutions for ammonia production, storage, transfer, and industrial refrigeration systems. Our valve technologies support reliable flow control and isolation, with product selection based on ammonia service conditions, pressure, temperature, material compatibility, and applicable safety requirements.
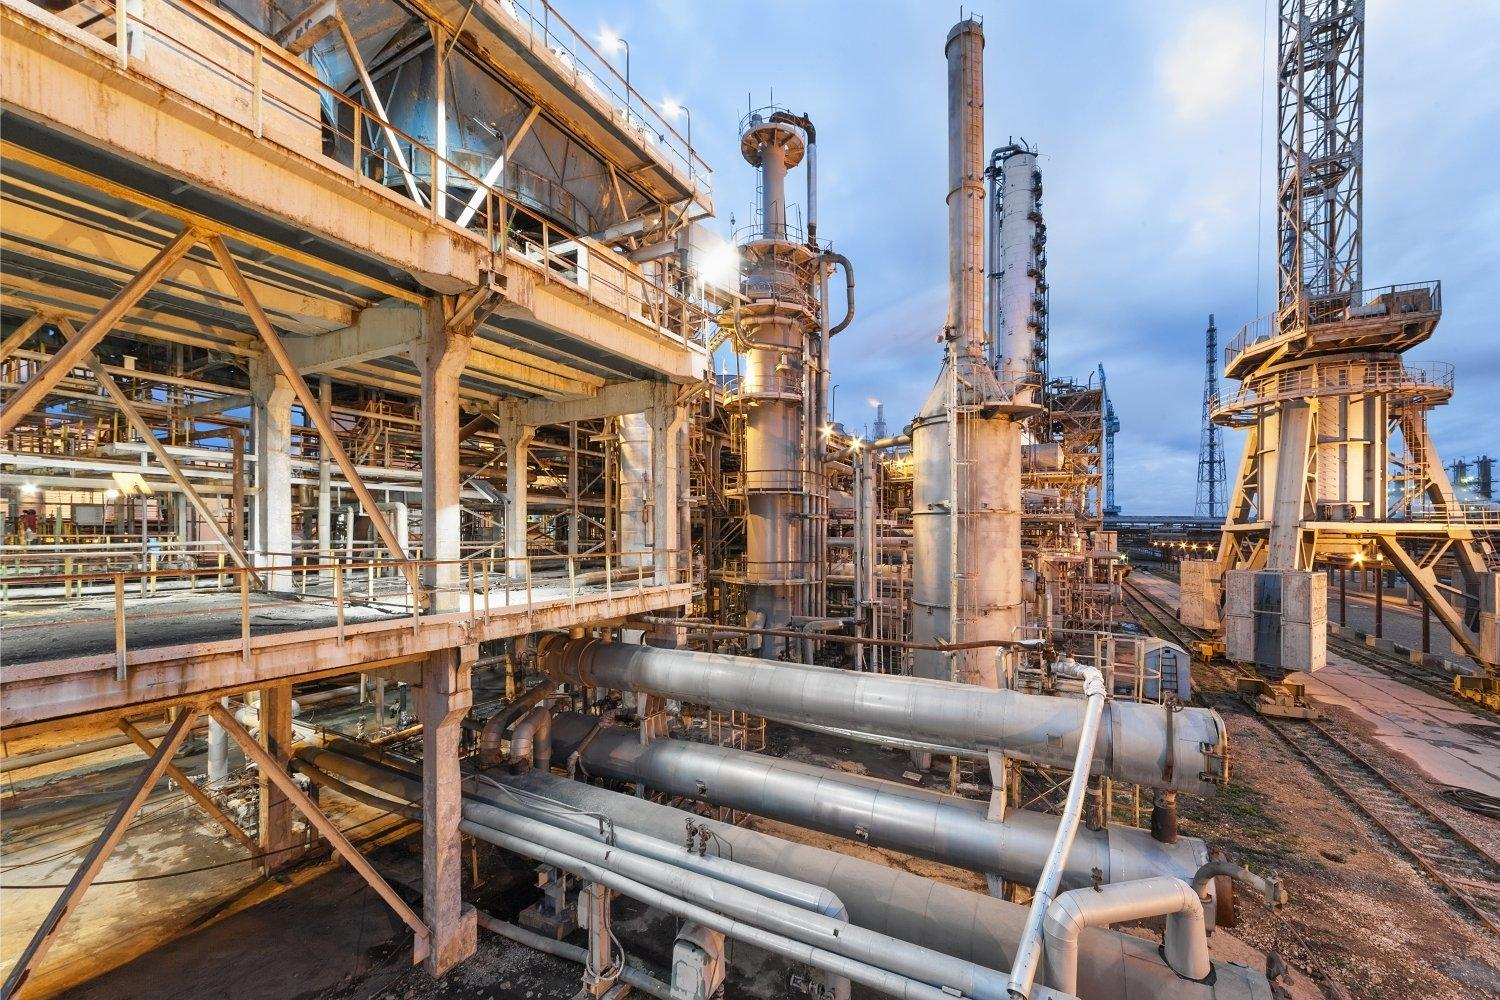
Industrial valve solutions for ammonia synthesis, process gas lines, and production utilities, selected according to pressure, temperature, and ammonia compatibility requirements.
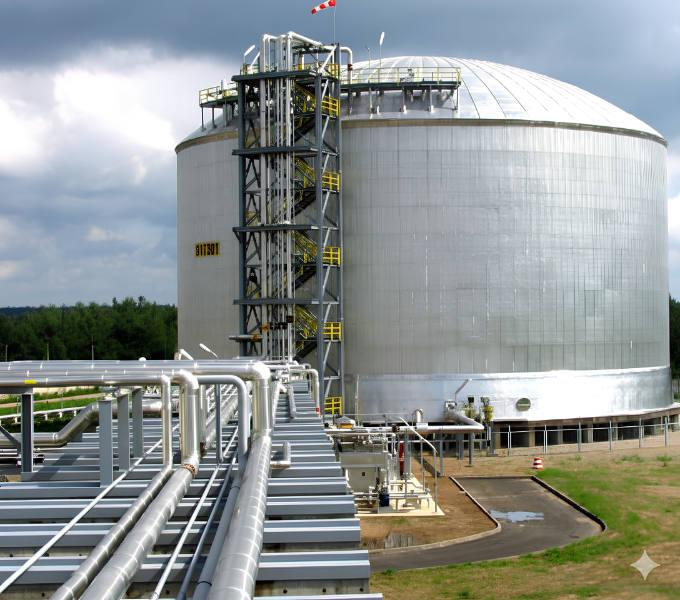
Valve solutions for ammonia storage, loading and unloading systems, and transfer pipelines, with suitable materials and seals for the operating conditions.
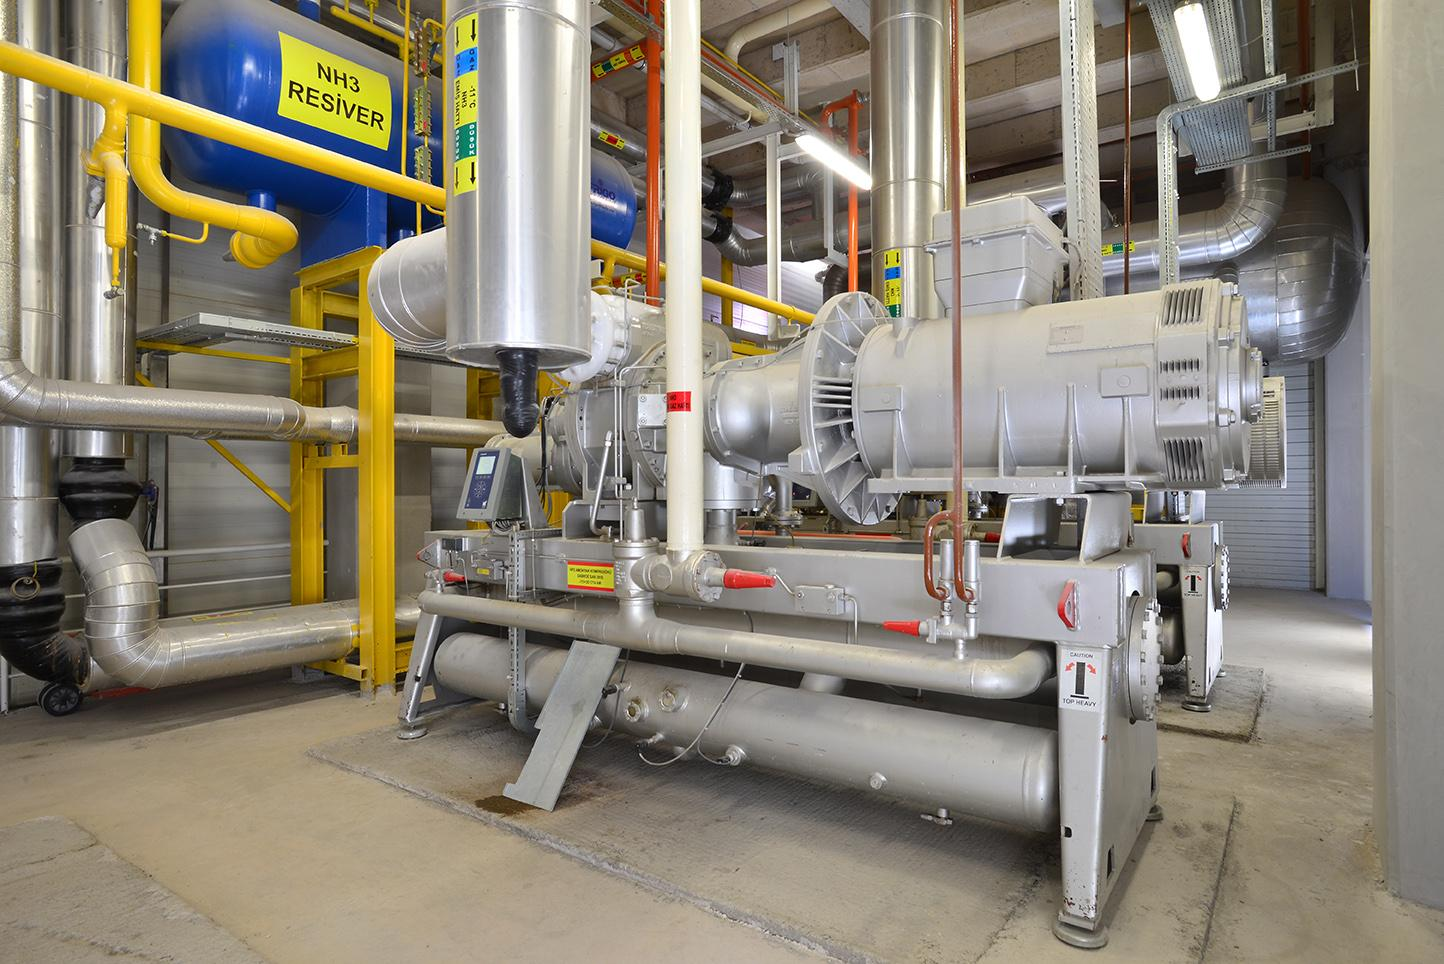
Valve solutions for industrial ammonia refrigeration circuits, compressors, and refrigerant distribution lines, selected for the required pressure, temperature, and refrigerant service.
Built for Demanding Conditions
Up to Class 2500 (ASME B16.34)
(-196°C to +650°C)
(Depending on valve type, material, sealing system, and application)
1/2" to 20"
DN15 to DN500
Flanged, Butt Weld, Socket Weld, Threaded, RTJ
WCB, LCB, CF8, CF8M, SS304, SS316, Duplex Stainless Steel, Super Duplex Stainless Steel, Alloy Steel, Chrome Moly Alloy Steel
API 6D, API 608, API 609, API 598, ASME B16.34, ISO 15848, ISO 27913, ANSI, DIN, BS
Got Questions?
Common questions about valve design, performance, and automation for this application.