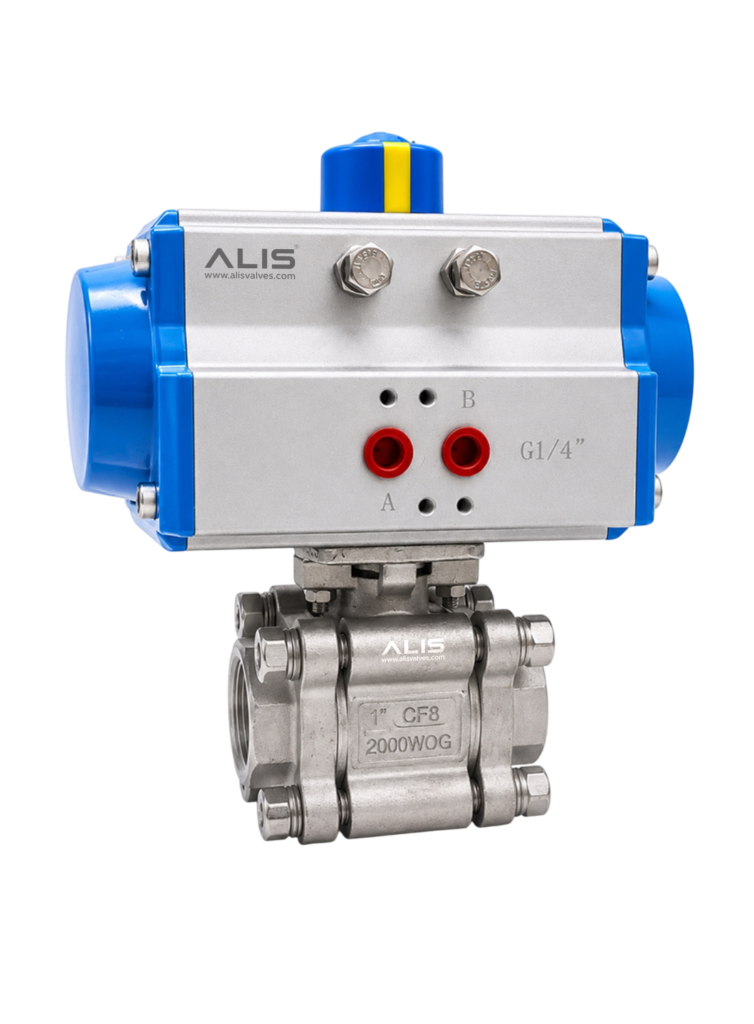
BALL VALVES
Pneumatic 3 PC Screwed Ball Valve
ALIS Valves is a leading Pneumatic 3 Piece Threaded Ball Valve Manufacturer…
Engineered for Safety, Reliability & Performance in Demanding Process Applications
Alis Valves Vaccum Valve Solutions & Manufacturer in India, engineered to provide reliable, leak-tight flow control in vacuum processing systems, chemical plants, pharmaceutical facilities, semiconductor manufacturing, food processing, laboratories, and industrial automation. Our comprehensive range of ball valves, butterfly valves, gate valves, globe valves, check valves, control valves, pneumatic actuated valves, and electric actuated valves is designed to maintain vacuum integrity while ensuring precise flow regulation and dependable performance. Built to international standards, our valves deliver superior sealing, corrosion resistance, and long service life in demanding vacuum environments.
Valve Solutions for Vacuum
A wide range of high-performance valves designed to meet the critical demands of Vacuum applications.
ALIS Valves is a leading Pneumatic 3 Piece Threaded Ball Valve Manufacturer…
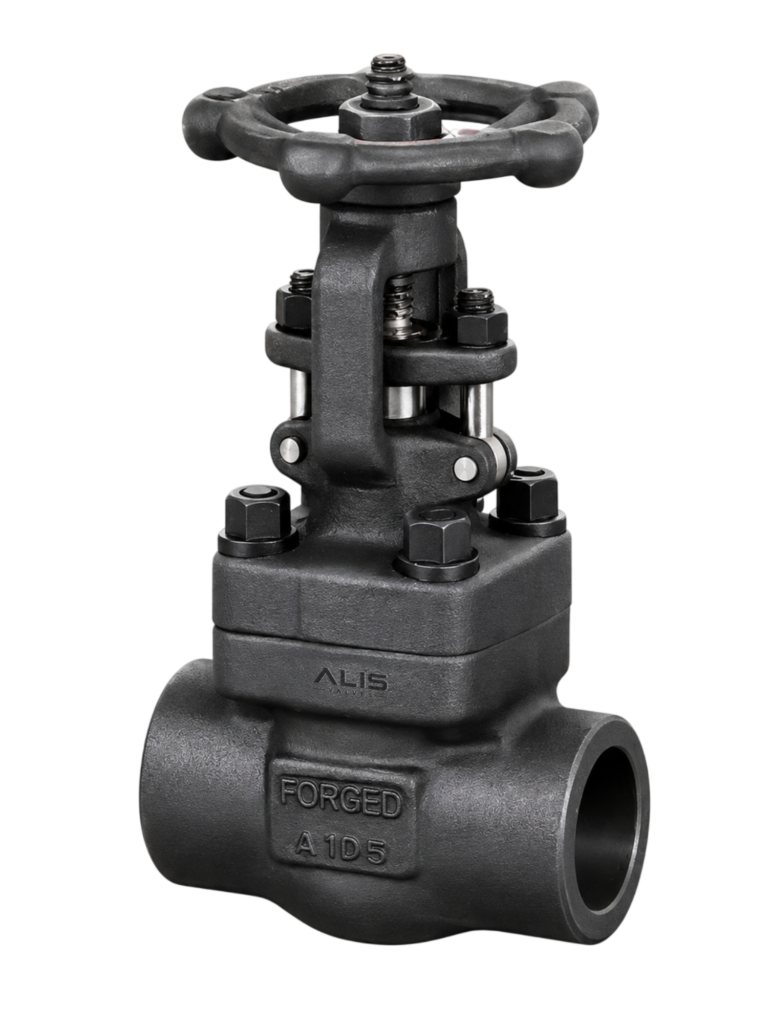
ALIS Valves is a Forged Steel Gate Valve Manufacturer in India, offering…
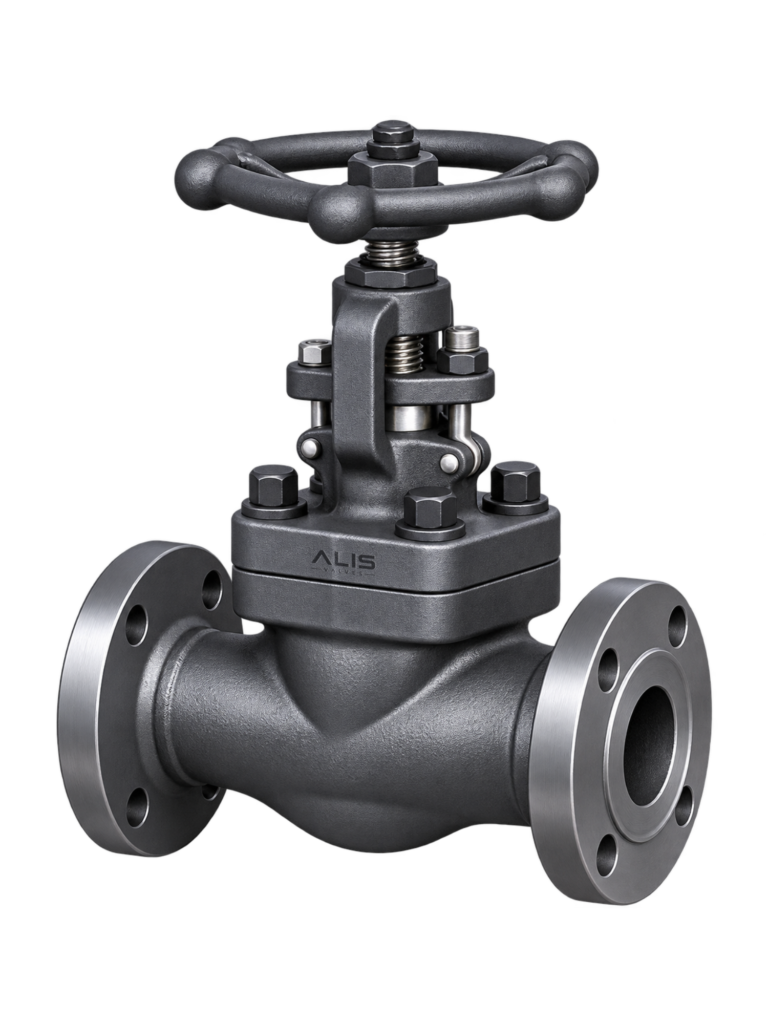
Alis Valves is an Forged Steel Globe Valve Manufacturer, Supplier in India…
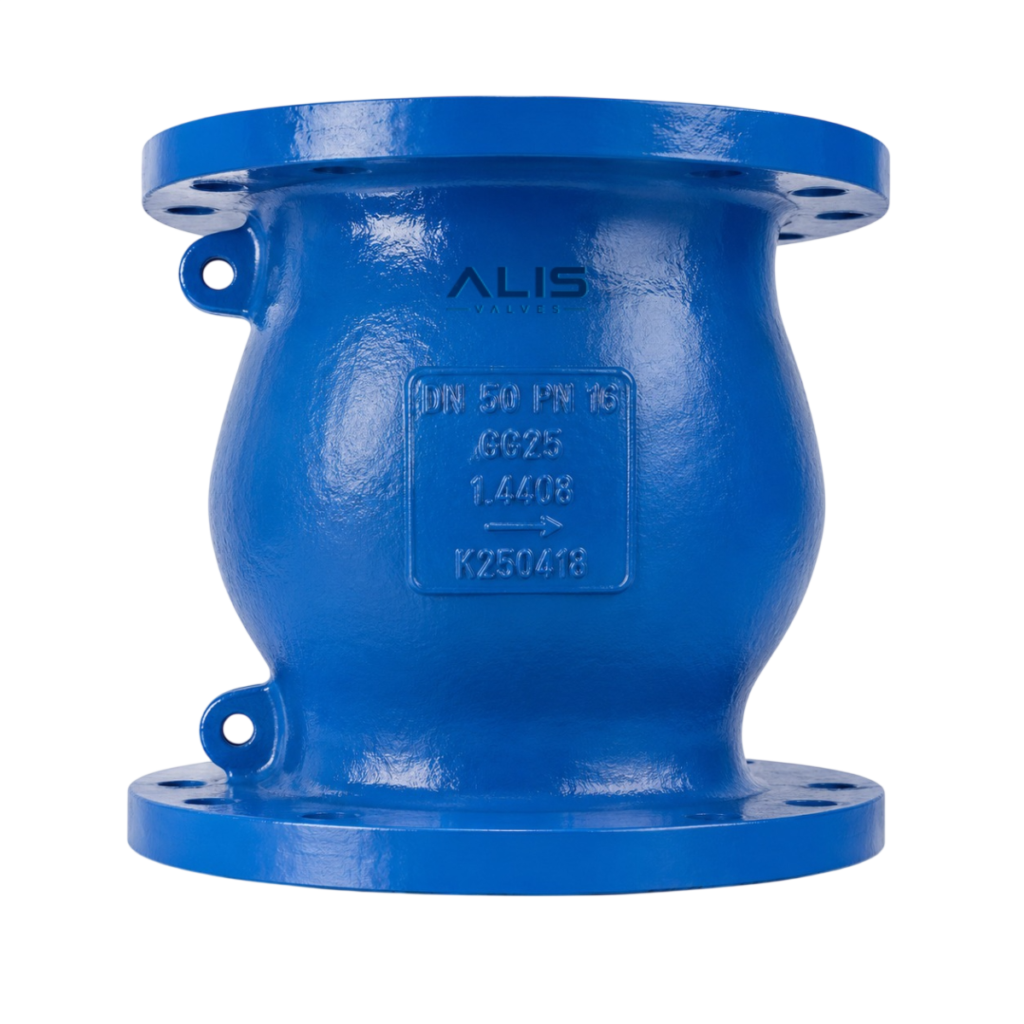
Axial Flow Check Valve Manufacturer Supplier in India is designed for reliable…
Product Categories for Vacuum
Explore key valve categories and automated packages engineered for Vacuum applications.
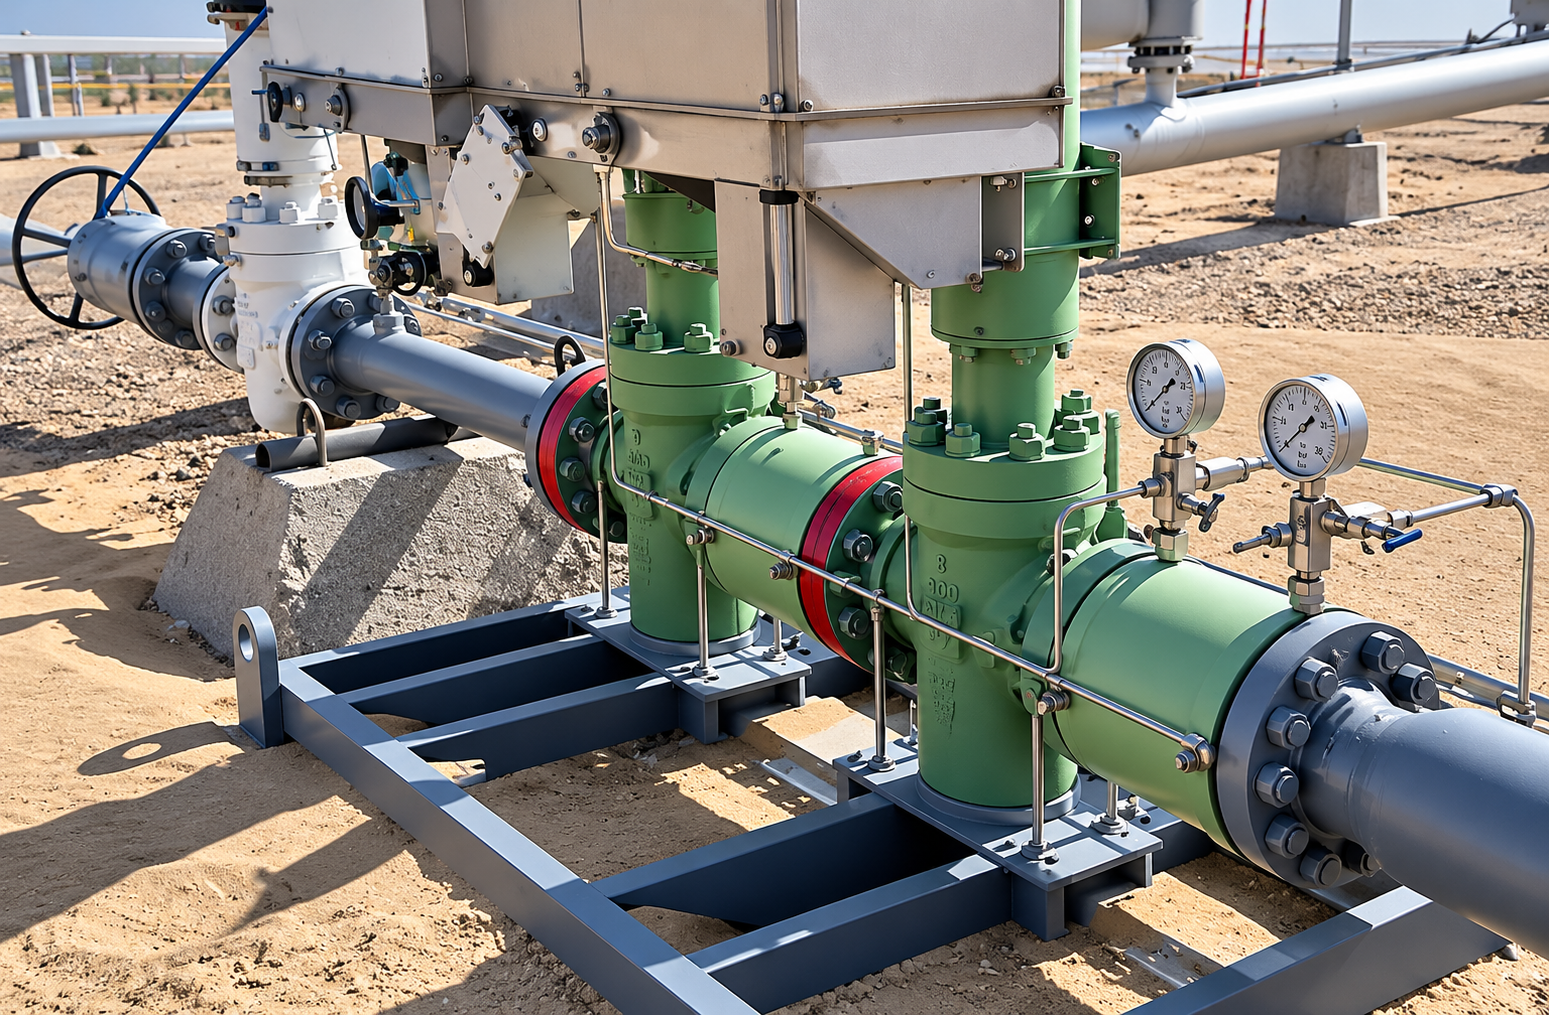
Designed around your needs, our Ball Valves deliver smooth operation, reliable shut-off, and the confidence you need for every flow…
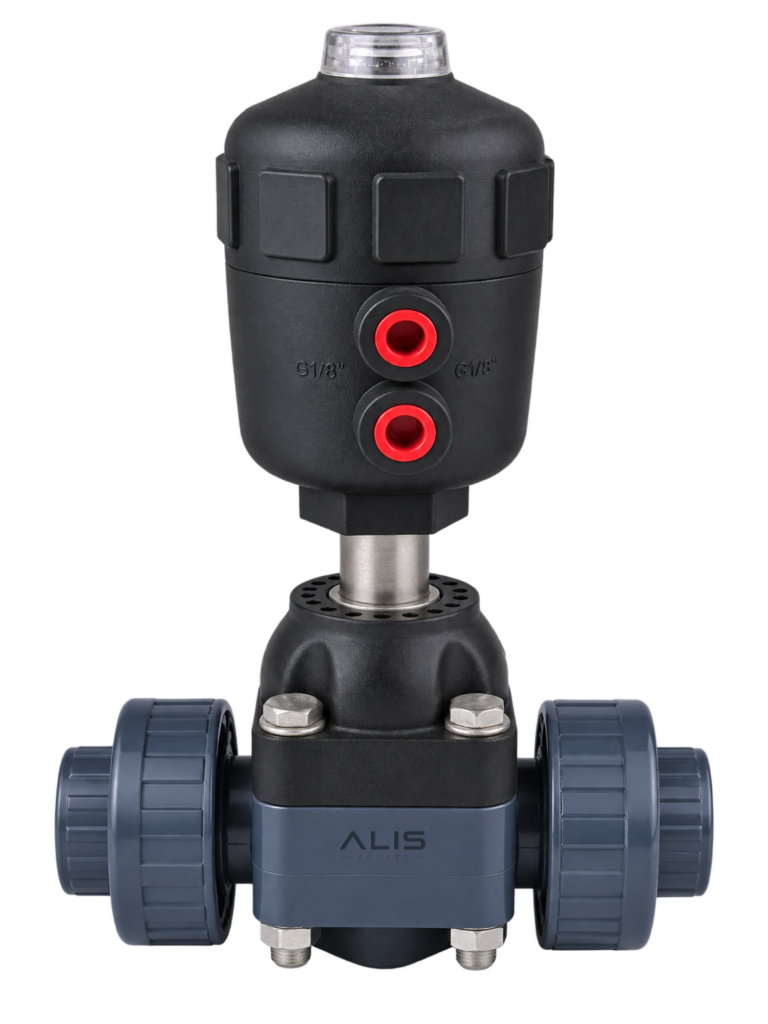
Complete Range of Pneumatic Actuated Ball, Butterfly, Gate, Globe and Control Valves for Reliable Industrial Automation and Precise Flow Control.

Engineered Gate Valve engineered for superior reliability and severe service performance.
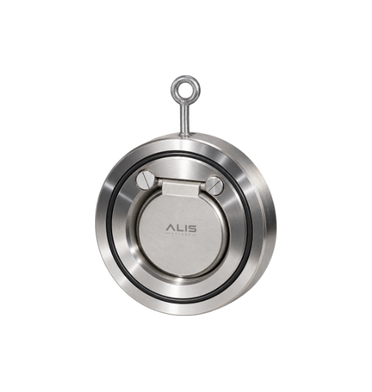
GGC Valves designed to deliver dependable shut-off, precise flow control, and effective non-return protection in demanding industrial process applications.
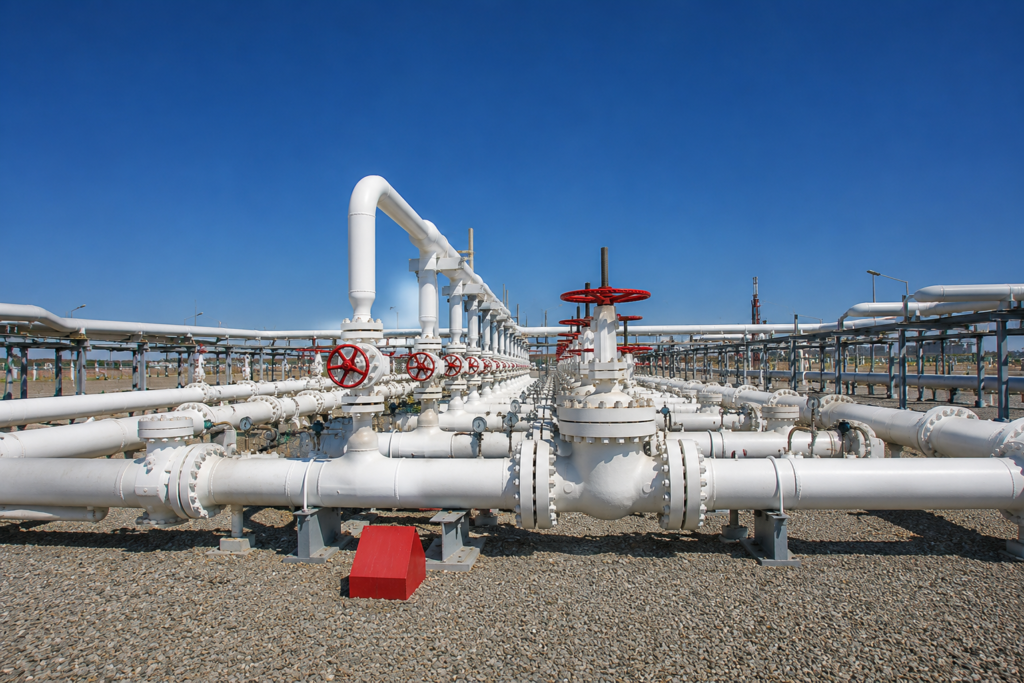
Ensures precise flow regulation and reliable shut-off for steam, water, oil, and other demanding industrial process applications.
VACUUM INDUSTRY SOLUTIONS
ALIS Valves provides industrial valve solutions for vacuum systems, process equipment and storage applications. Valve selection depends on operating pressure range, temperature, process media and application requirements.
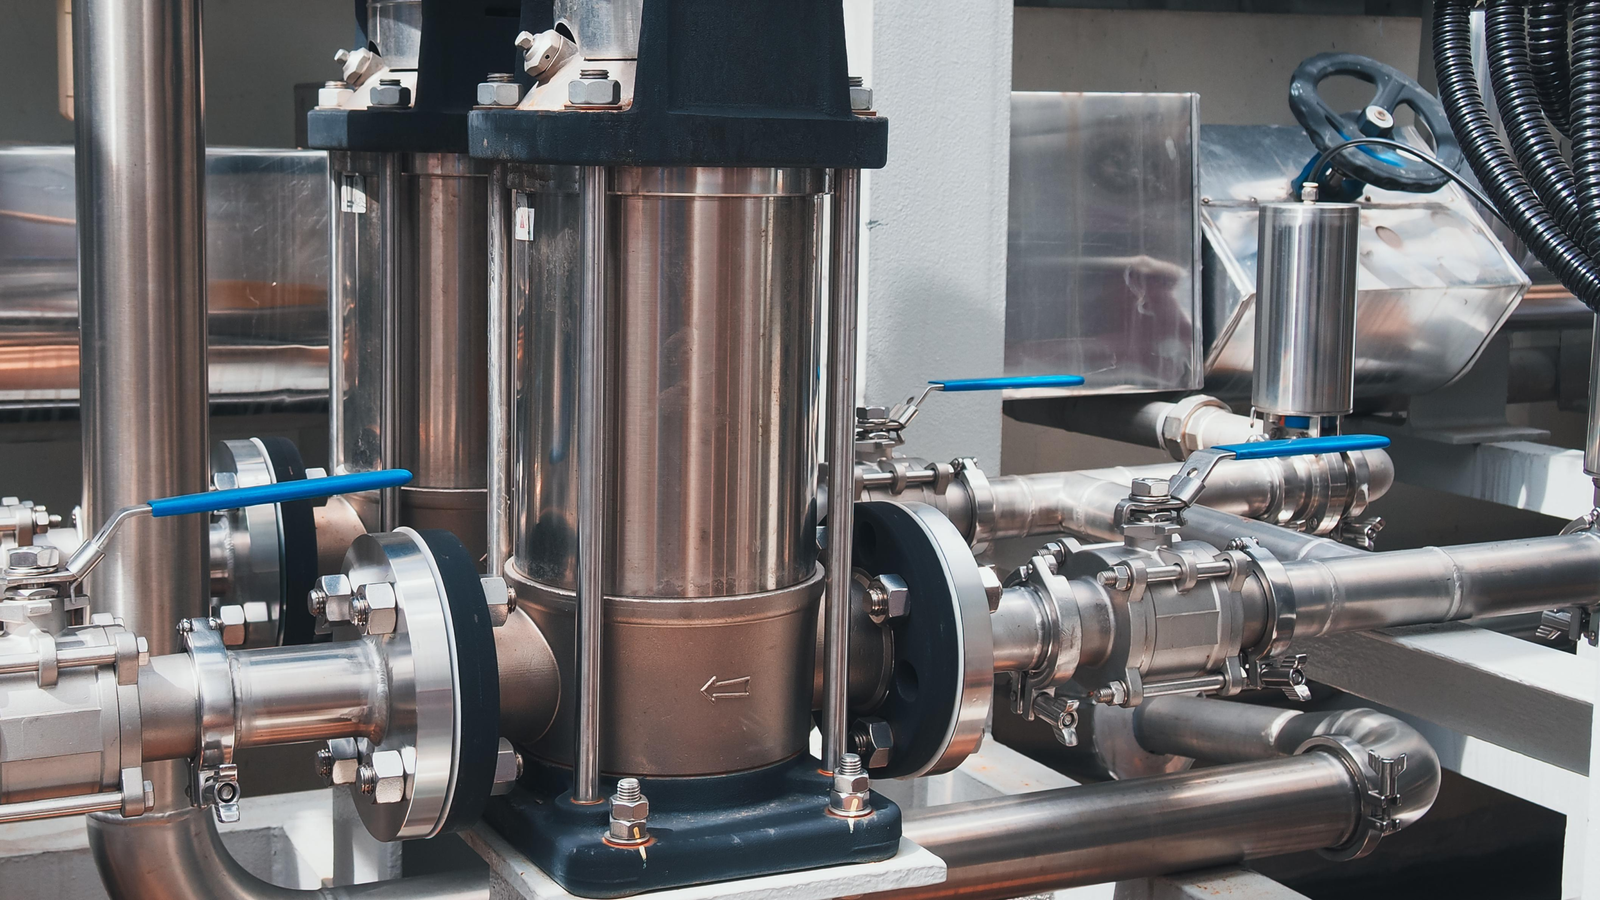
Valve solutions for vacuum pumps, vacuum generation systems and associated pipelines, supporting reliable isolation and process control.
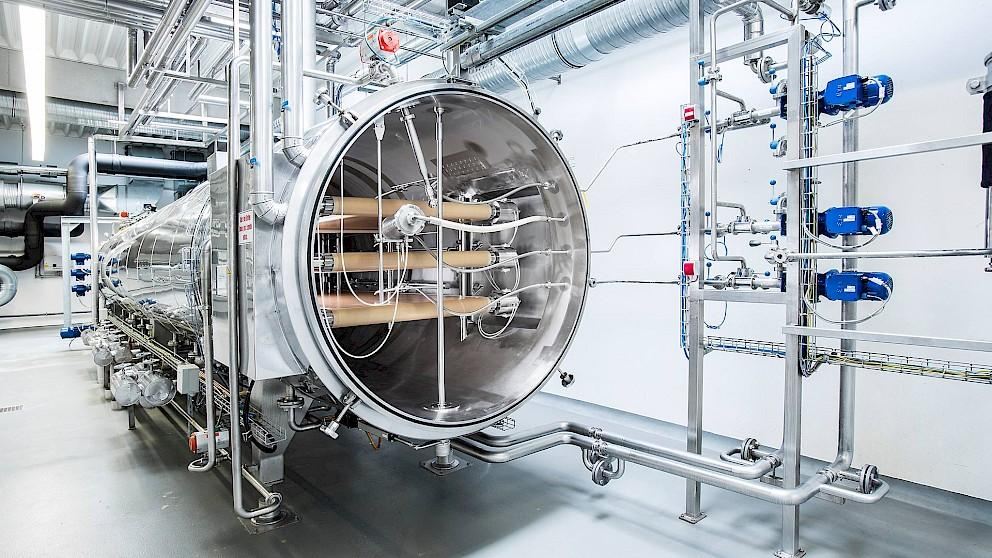
Industrial valve solutions for vacuum process lines, reactors, dryers and process vessels, selected for reliable performance under vacuum conditions.
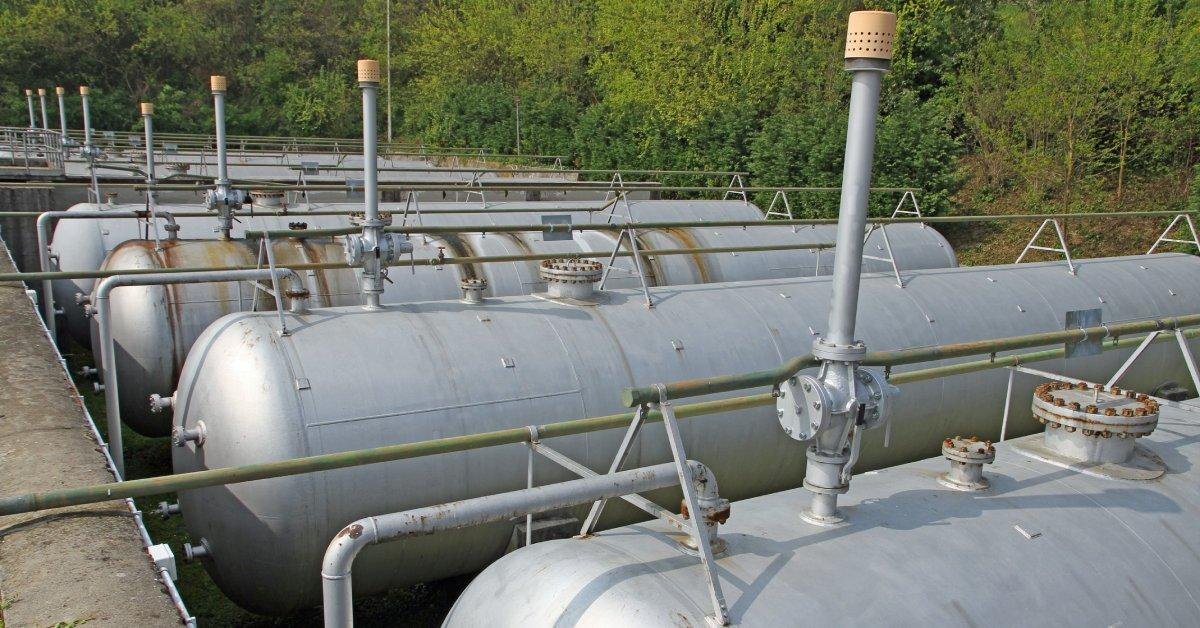
Valve solutions for vacuum protection of storage tanks, vessels and process equipment, helping maintain system integrity under vacuum conditions.
Built for Demanding Conditions
Full Vacuum to Class 600 (ASME B16.34)
-20°C to +250°C
1/2" to 20"
DN 15 to DN 500
Flanged, Wafer, Threaded, Socket Weld, Butt Weld, Tri-Clamp (TC)
WCB, CF8, CF8M, SS304, SS316, Duplex Stainless Steel, PTFE, PFA-Lined
API 6D, API 608, API 598, ASME B16.34, ANSI, DIN, BS, ISO
Got Questions?
Common questions about valve design, performance, and automation for this application.